19+
Years Industry Expertise (Est. 2006)
100+
Countries & Jurisdictions Exported
40,000+
Validated Batches Delivered
3,500+
B2B Brand Partners Globally
400+
Engineered Commercial Formulations
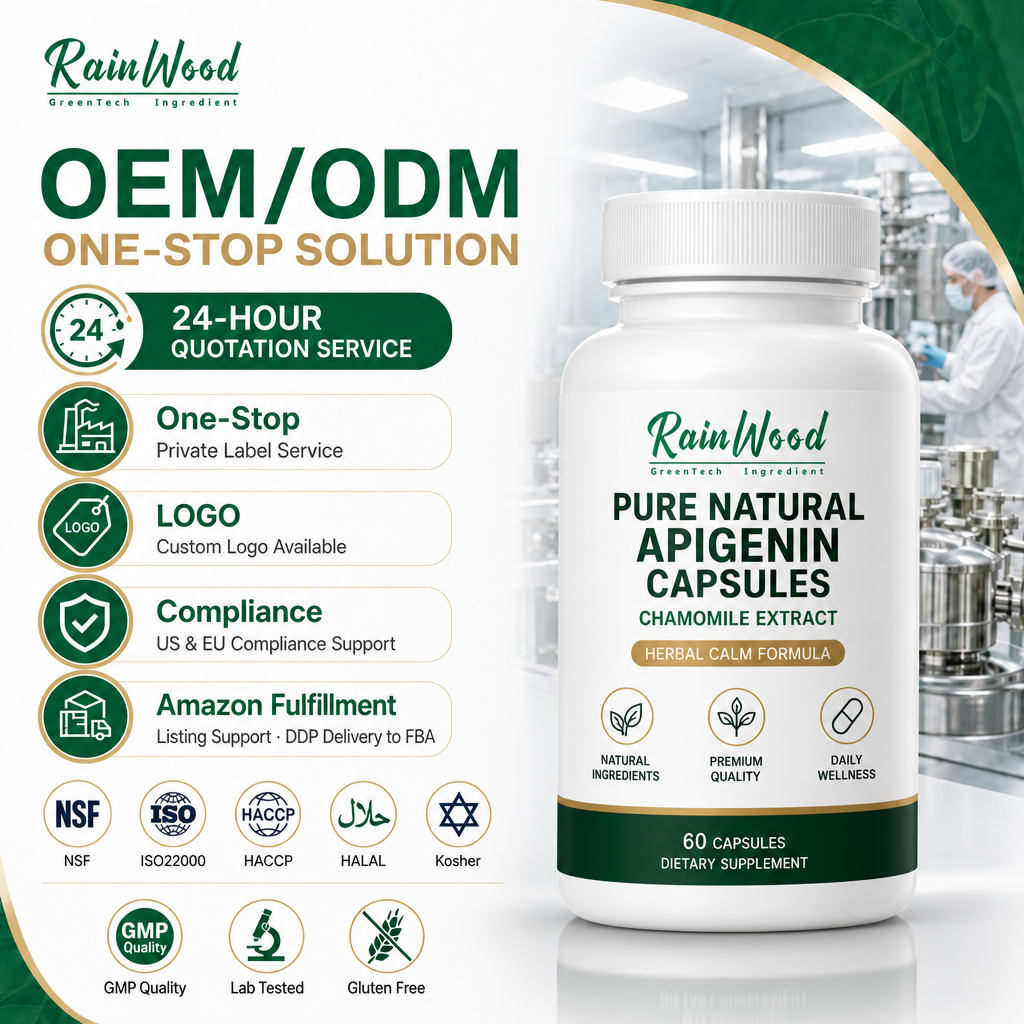
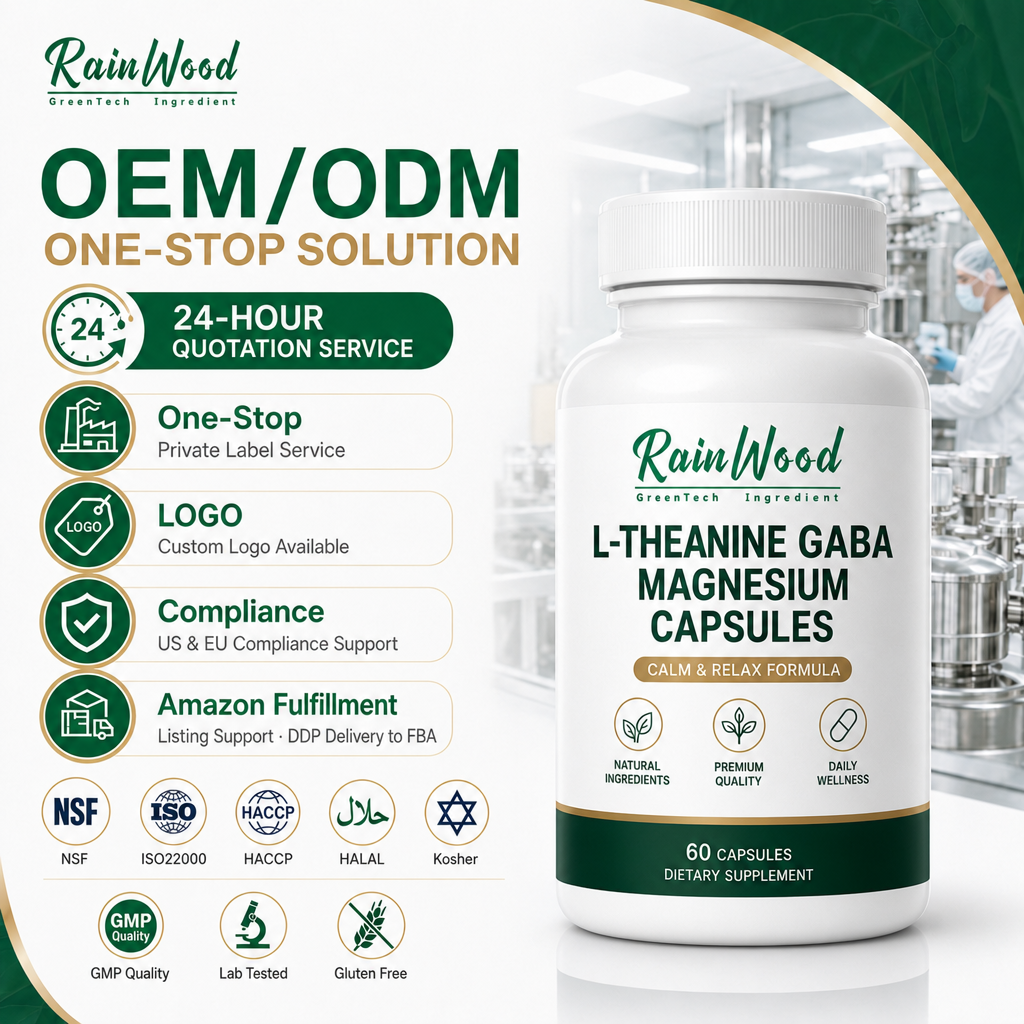
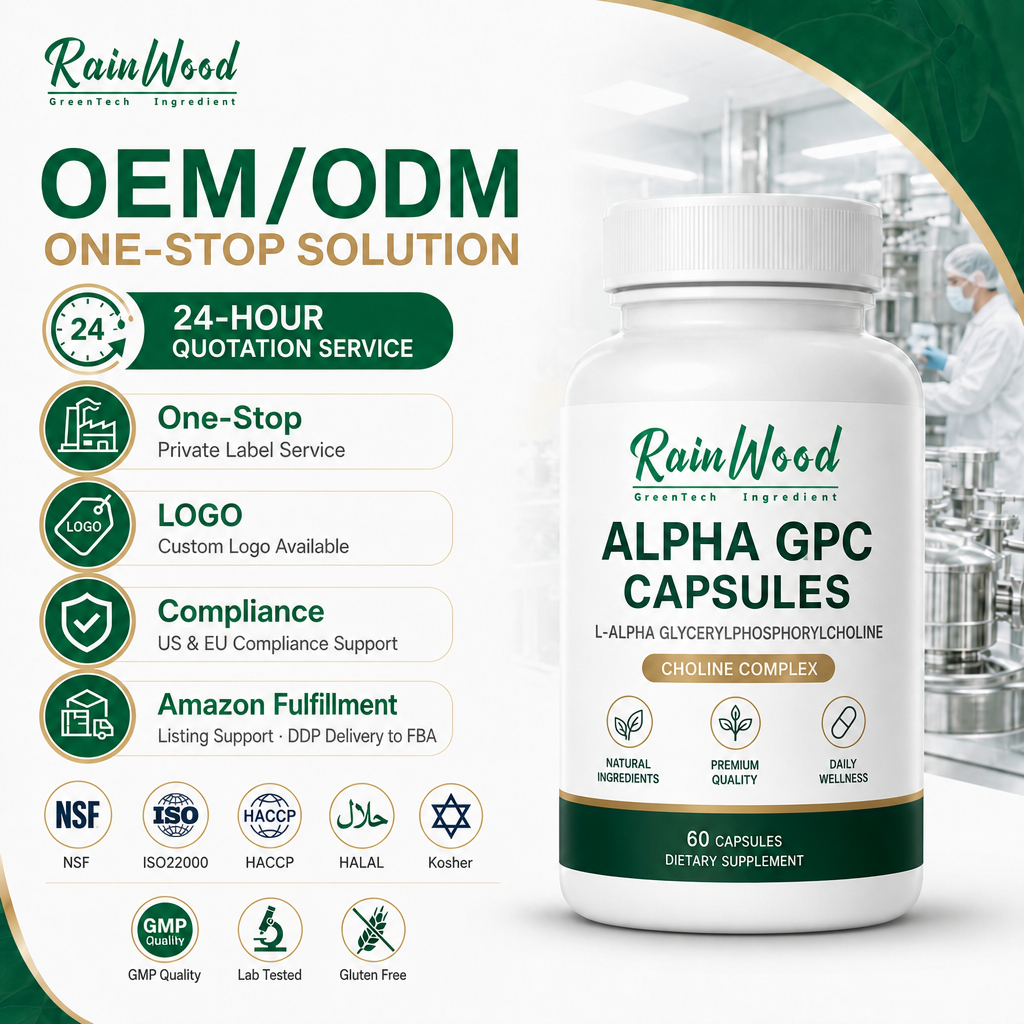
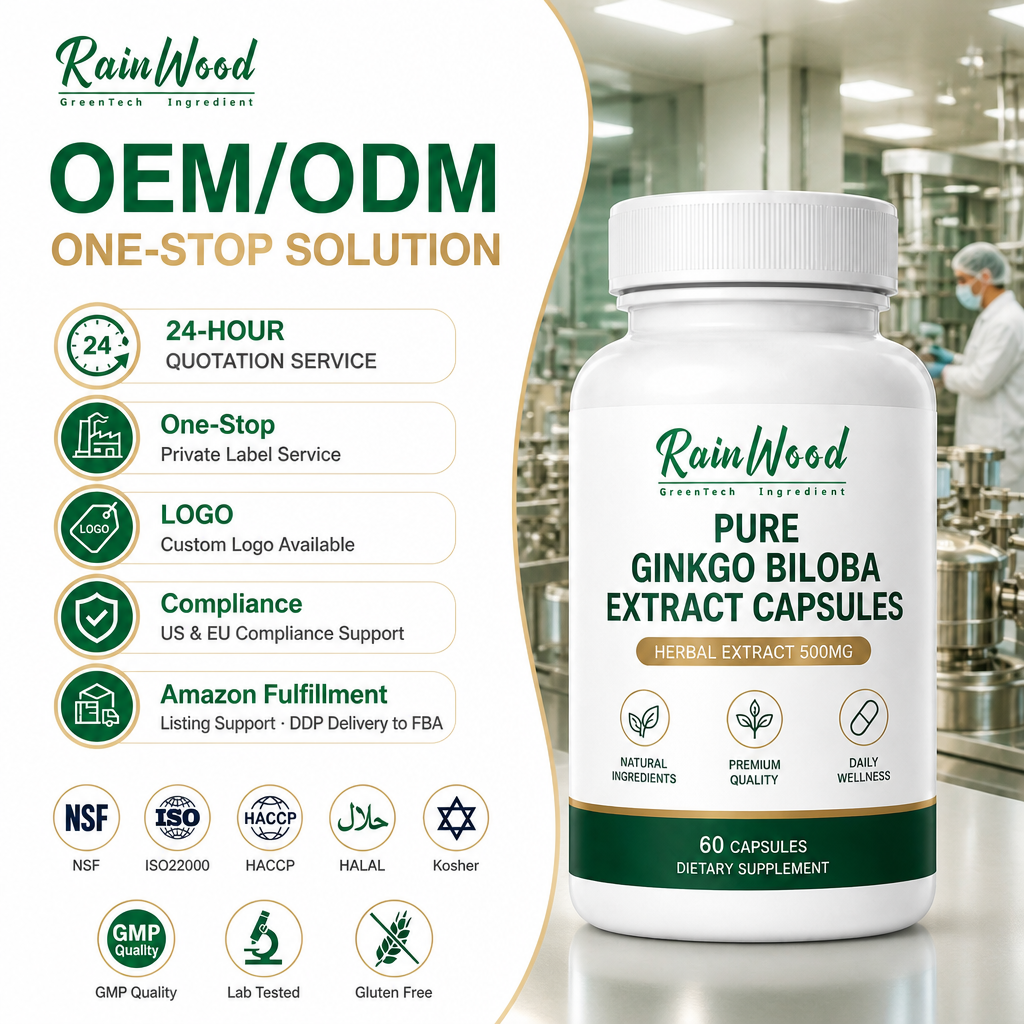
Flagship Formulations
Audited Herbal Leaf & Botanical Finished Formulations
Every finished formulation utilizes active herbal extracts and synergy-paired compounds produced in Class 100,000 cleanrooms under stringent NSF 455-2 GMP, ISO 22000, and CE compliance standards.
Procurement Intelligence
Technological Trajectories in Industrial Leaf Extraction
As international health authorities tighten botanical purity guidelines, sourcing professionals are transitioning from traditional fluid extracts to precision-standardized, green-extracted powders.
Supercritical CO2 & Low-Thermal Processing
Thermal degradation remains the primary failure mode in standard leaf extraction. Conventional steam or high-heat ethanol baths often destroy thermolabile terpenes, volatile flavonoids, and polyphenols.
- Zero Residual Solvents: Meets stringent USP <467> class 1 and class 2 limits.
- Low-temperature vacuum concentration protects active marker profiles.
- Selective fractioning isolates target molecular weights with clinical accuracy.
Purity Verification & Xenobiotic Screening
Modern import customs and health ministries enforce zero-tolerance metrics for environmental contaminants. Industrial leaf extractors must operate in-house mass spectrometry suites.
- ICP-MS Heavy Metal Analysis: Lead (<0.5 ppm), Arsenic (<1.0 ppm), Cadmium, Mercury.
- Comprehensive 500+ GC-MS pesticide screening compliant with EU 396/2005.
- Aflatoxin and microbiological limit controls (USP <2021>, <2022>).
Solubility & Bioavailability Nano-Engineering
Standard raw leaf powders suffer from poor water solubility and sub-optimal digestive absorption. The shift toward functional beverages and rapid-action capsules requires structural modification.
- Micro-encapsulation & Liposomal Formats: Shields actives against stomach acid.
- Spray-dried instantized granulation tailored for stick packs and sachet dosing.
- Controlled tap density for high-speed automated capsule filling lines.
Market Forecast
Procurement Criteria Defining 2026–2030 Vendor Selection
Brand integrity rests upon raw material transparency. Leading brands are abandoning unverified brokerage markets in favor of direct-from-factory partnerships with verified audit trails.
1. Validated Botanical DNA Fingerprinting
Economic adulteration—such as spiking low-potency leaf extract with synthetic chemical markers or unrelated species—is eliminated through universal DNA barcoding and TLC/HPLC comparison against certified botanical reference materials.
2. Turnkey Private Label Integration
Importers reduce supply chain fragmentation by sourcing raw extraction and downstream dosage manufacturing (hard capsules, stick packs, gummies) from a single certified factory, drastically shortening lead times to 15–25 business days.
3. Ethical Wild-Harvesting & GAP Agriculture
Traceable origin mapping from Good Agricultural and Collection Practice (GACP) compliant botanical farms guarantees leaf raw materials are harvested at seasonal active-constituent peaks without contaminating native ecosystems.
4. Multi-Jurisdictional Regulatory Dossiers
Procurement teams now mandate that each batch arrives with complete technical documentation: full spectral COA, non-GMO declaration, BSE/TSE statements, allergen clearance, and packaging migration safety certifications.
Enterprise Manufacturing
Inside ESNO Biotech: 19 Years of Extraction Excellence
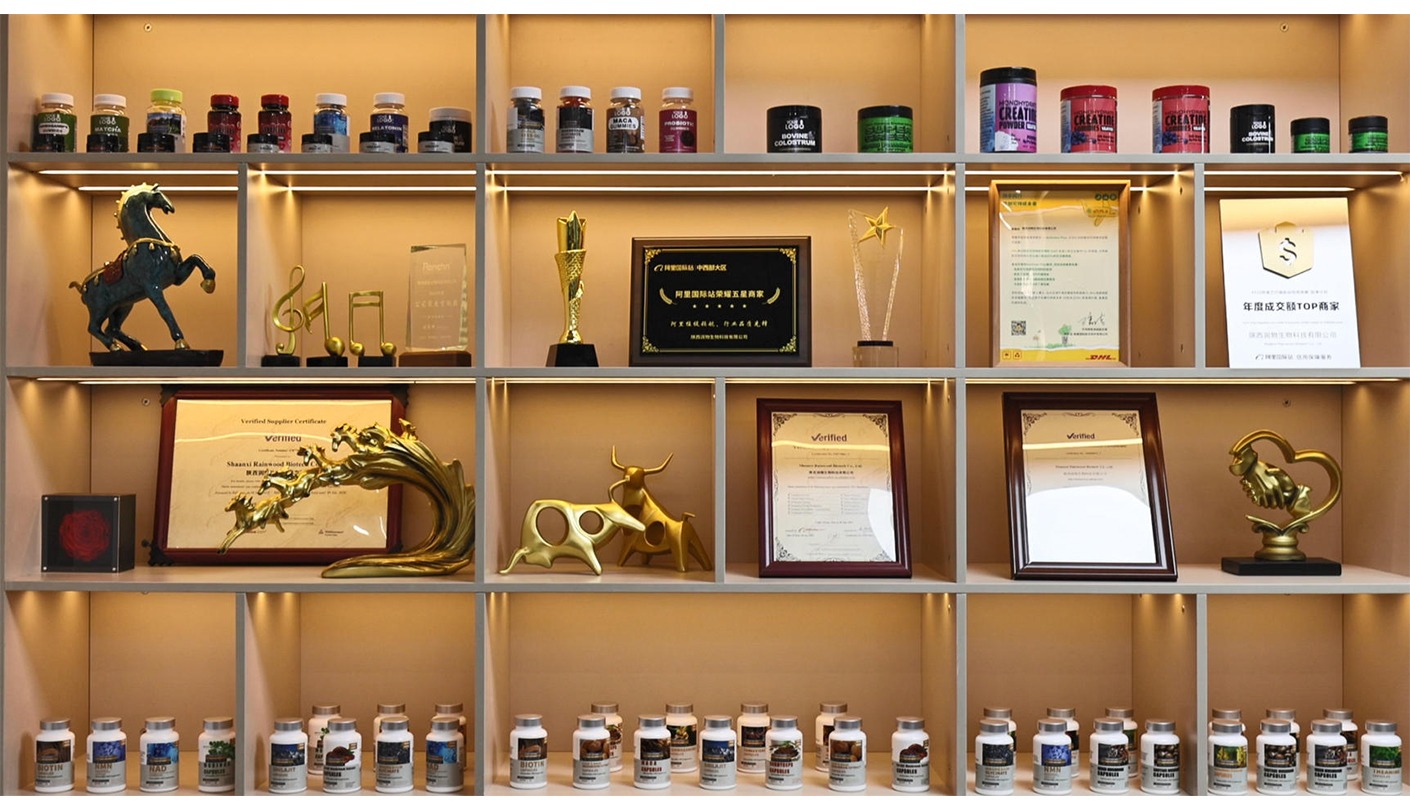
Established in 2006 in Xi'an, Shaanxi, ESNO Biotech operates industrial-scale extraction, isolation, and dosage manufacturing facilities audited by TÜV Rheinland and accredited under NSF 455-2 GMP, ISO 22000, and HACCP frameworks.
Automated Production Capacity
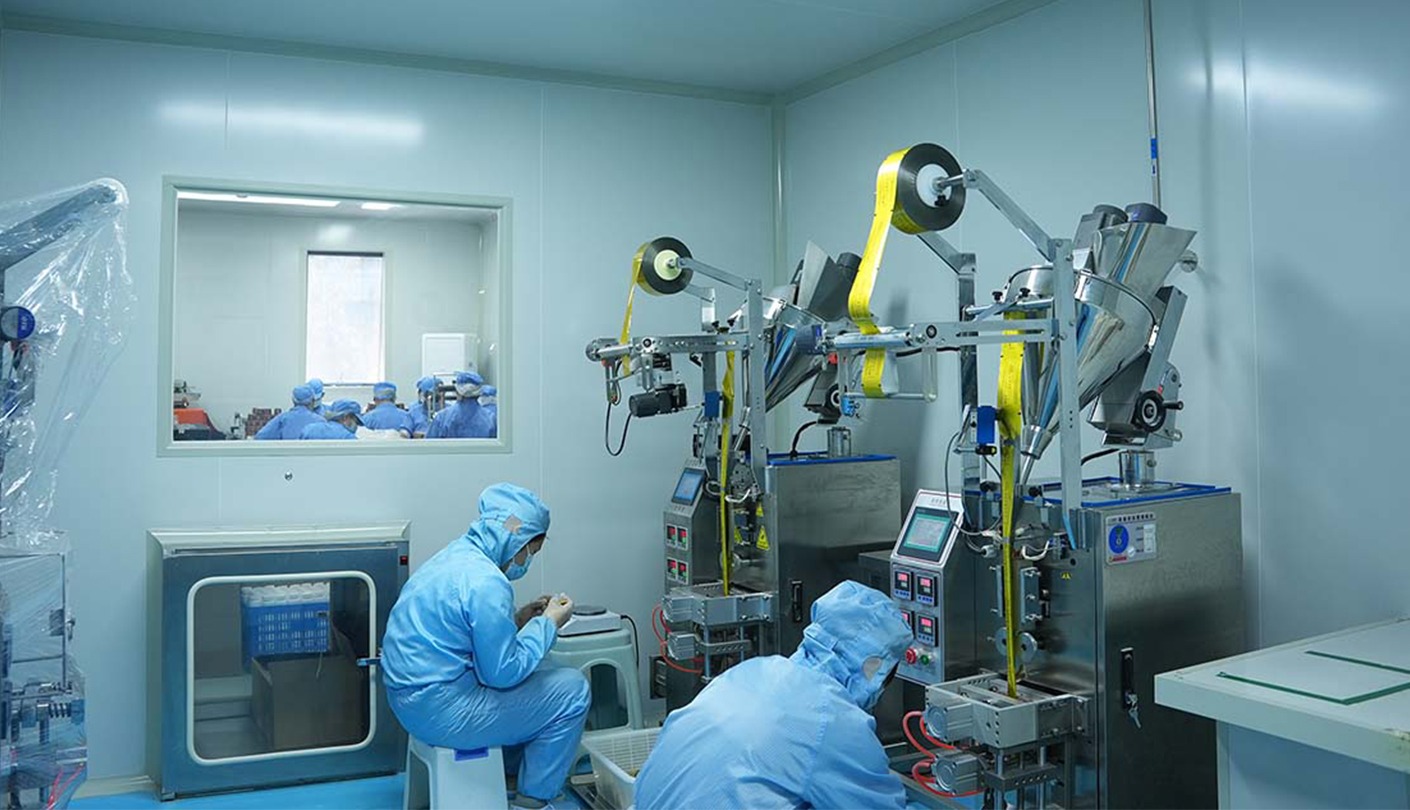
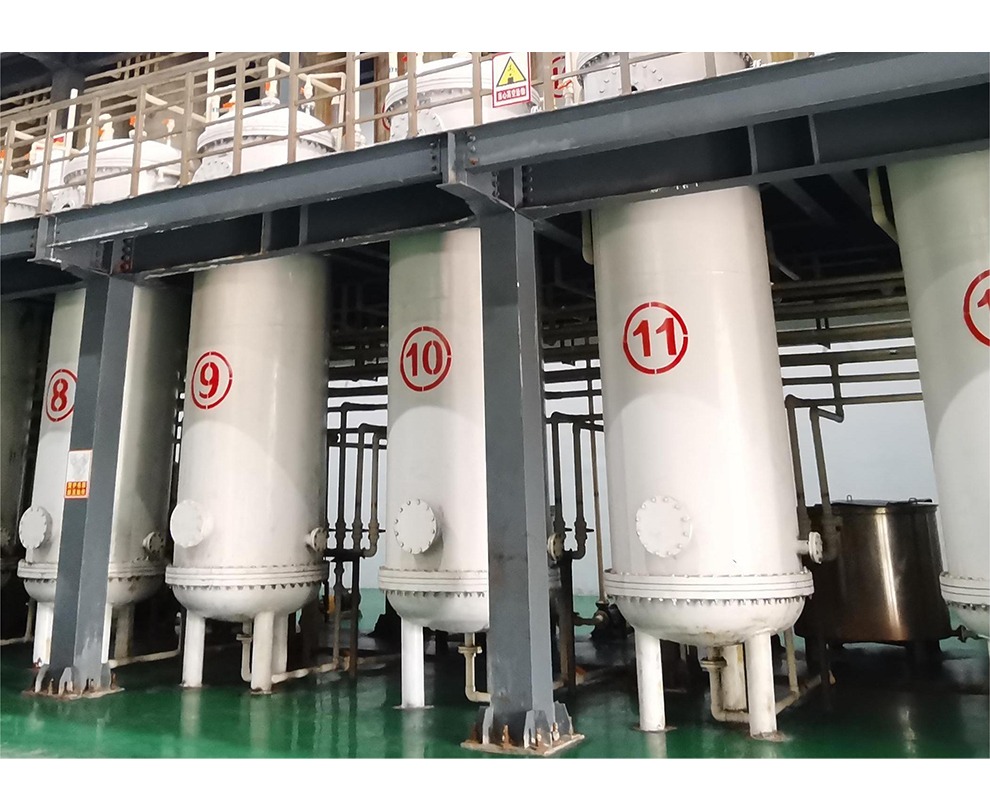
Equipped with multi-function dynamic countercurrent extraction tanks, continuous falling-film evaporators, spray drying towers, and high-speed capsule encapsulation lines, our automated workshops maintain continuous batch-to-batch homogeneity with zero cross-contamination risks.
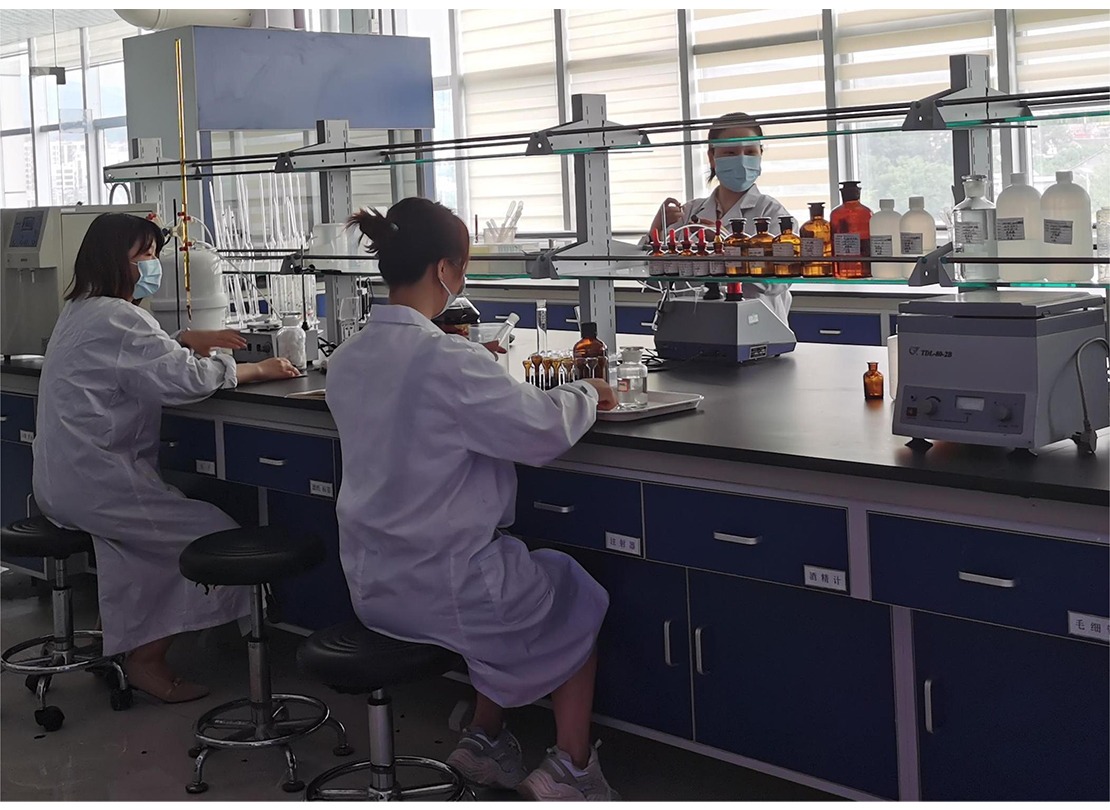
Internal Analytics & QC Laboratories
Our quality verification lab features Agilent HPLC systems, GC-MS, atomic absorption spectrophotometers (AAS), UV-Vis, stability test chambers, and microbiological incubators, enabling independent testing before any batch is released from quarantine.
Rapid Formulation & Prototyping
Supported by an experienced formulation team with over 400 completed commercial designs, we assist brand partners with excipient compatibility studies, disintegration optimization, vegan shell conversion (HPMC), and proprietary flavor/taste-masking development.
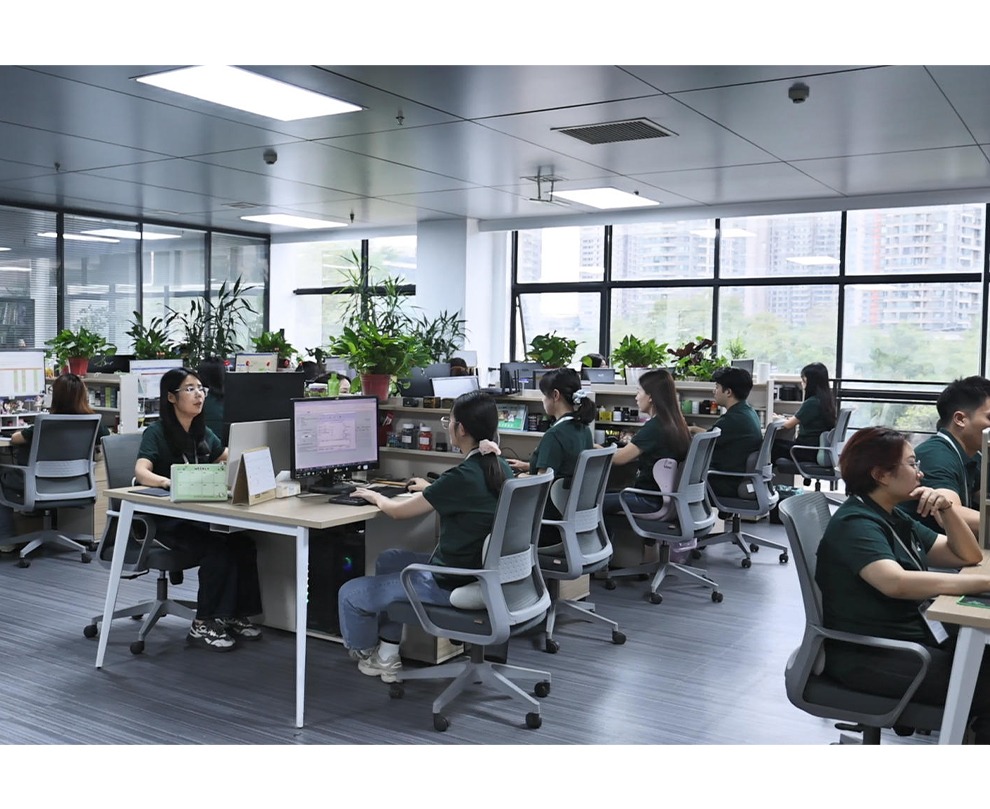
Corporate Headquarters
GMP Workshop
Production Lines
QC Analytical Lab
Clean Packaging
Logistics Warehouse
Procurement FAQ
Frequently Asked Questions by B2B Buyers
Direct answers addressing technical parameters, minimum orders, compliance paperwork, and export logistics.
What specific standardization and marker assays do you guarantee for leaf extracts?
Our extracts are standardized against specific pharmacopeial reference targets verified via HPLC, UV, or LC-MS/MS. For instance, our Ginkgo Biloba Leaf Extract is precisely titrated to ≥24% Flavonol Glycosides and ≥6% Terpene Lactones, with Ginkgolic Acids strictly controlled below 5 ppm (or <1 ppm upon buyer request). Every batch includes a comprehensive Certificate of Analysis (COA) specifying exact active marker percentages, loss on drying, ash content, and bulk density.
What are your factory Minimum Order Quantities (MOQs) for bulk powders and private label capsules?
To accommodate established brands and growing Amazon/eCommerce sellers, we provide flexible low-barrier entry tiers: bulk standardized botanical extracts typically start at 1 kg to 25 kg fiber drums. For private-label finished goods (such as 60-count hard capsule bottles or blister packs), stock formulas start from 100 to 500 units, while completely custom formulations with tailored excipient systems generally require 1,000 units.
What international compliance certifications are accessible for supplier qualification audits?
Our manufacturing operations are verified on-site by TÜV Rheinland and operate in full compliance with NSF 455-2 GMP (Dietary Supplements), ISO 22000 (Food Safety Management), HACCP principles, and EU/USDA Organic standards. We provide complete audit dossiers containing process validation records, pest control logs, allergen segregation matrices, cleanroom calibration sheets, and CE compliance documentation.
How do you handle stability, dissolution, and heavy metal testing for finished capsule runs?
Every manufactured batch undergoes a mandatory 3-stage QA quarantine: raw material testing prior to weighing, in-process testing during blending and encapsulation (weight variance <±3%, disintegration time <15 minutes according to USP <701>), and finished-lot analytical release. Heavy metals (Pb, As, Cd, Hg) are quantified via ICP-MS, and real-time/accelerated stability testing is available to support expiration dating on your retail labels.
Can you support custom export clearance documents for the European Union, UK, and North America?
Yes. Having exported to over 100 countries since 2006, our dedicated documentation team issues full customs-ready shipping packets including Phytosanitary Certificates, Certificates of Free Sale (CFS), Certificates of Origin (CO / Form A), Safety Data Sheets (SDS), TSE/BSE Non-Contamination Declarations, and bilingual compliant product specification sheets for seamless border clearance.
Launch Your Standardized Leaf Extract Formulation
Connect with our technical formulation team to request comprehensive Certificates of Analysis, request trial sample lots, or obtain detailed OEM/ODM volume pricing for your private label brand.