Advanced Plant Extract & Bio-Nutrient Catalog
Standardized botanicals and clean-label synergistic premixes manufactured under NSF 455-2 GMP, ISO 22000, and HACCP certifications.
19+
Years of Botanical Extraction & Processing
100+
Global Export Destination Markets
40,000+
Nutraceutical Production Batches Delivered
400+
Proprietary Formulations Engineered
Technological Leadership
Next-Generation Botanical Extraction: Science, Bioavailability, and Standardization
The global concentrated plant extract market is undergoing a seismic structural paradigm shift. The historical reliance on crude solvent extractions and generic marker ratios (such as 10:1 or 20:1 TLC dry-weight ratios) has rendered modern brands vulnerable to severe analytical scrutiny, adulteration accusations, and sub-therapeutic bioavailability. Modern nutraceutical brands, pharmaceutical formulators, and sports nutrition enterprises require validated phytonutrient markers, validated by high-performance liquid chromatography (HPLC), gas chromatography-mass spectrometry (GC-MS), and ultra-performance liquid chromatography (UPLC).
As a foundational manufacturer operating out of China's primary botanical and herbal corridor in Shaanxi, ESNO Biotech leverages advanced green extraction methodologies. Our physical and supercritical fluid separation infrastructures eliminate harmful petrochemical residuals while preserving volatile secondary metabolites, terpenes, and polyphenols. By transitioning from conventional thermal drying to vacuum freeze-drying and microencapsulated spray drying, we mitigate thermolabile compound degradation, yielding concentrated botanical extracts characterized by superior aqueous solubility, bulk density stability, and enhanced physiological efficacy.
Key Procurement Insight: The implementation of targeted subcritical water extraction and enzymatic-assisted cellular wall breakdown allows us to isolate delicate phytomolecules—such as salidrosides in Rhodiola, withanolides in Ashwagandha, and trans-resveratrol from Polygonum cuspidatum—with recovery efficiencies outperforming standard atmospheric refluxing systems by over 34%.
Furthermore, the convergence of active plant extracts with clinically evaluated cellular energizers (such as Urolithin A, PQQ, and Magnesium L-Threonate) demands an uncompromising commitment to formulation science. Our research facility bridges the gap between raw botanical processing and finished retail-ready delivery systems, giving international buyers immediate access to scalable manufacturing, turn-key private labeling, and airtight regulatory documentation designed for North American, European, and Asia-Pacific market access.
Chromatographic Fingerprinting
Every commercial batch undergoes multi-point HPLC/UPLC compound fingerprinting, ensuring precise active content standardization, pesticide screening under EP/USP parameters, and eradication of botanical adulterants.
Bio-Enhancement Formulations
We deploy lipid-carrier systems, liposomal dispersion, and co-crystallization techniques to drastically overcome the poor intestinal absorption profiles characteristic of polyphenols, sterols, and triterpenoids.
Clean-Label Excipient Engineering
Eliminate titanium dioxide, talc, and magnesium stearate. Our production floor uses natural rice hull concentrates, organic acacia gum, and modified plant fibers for 100% clean-label finished capsules and powder packs.
Procurement Intelligence
Emerging Global Sourcing Trends in Concentrated Plant Extracts
Critical procurement intelligence for chief supply chain officers, raw material directors, and regulatory compliance leaders for the 2025–2030 sourcing cycles.
Full-Chain DNA & Isotope Provenance
Global regulatory bodies (FDA, EFSA, TGA) now prioritize total supply transparency. Modern procurement protocols require isotope ratio mass spectrometry (IRMS) and DNA barcoding to authenticate indigenous origin and harvest sustainability.
Shift from Raw Extracts to Functional Delivery
Purchasers are reducing exposure to raw powder processing risks by contracting fully integrated OEM producers capable of handling high-speed encapsulation, micro-granulation, functional gummies, and direct-to-consumer stick packaging.
Dynamic Trace Heavy-Metal Mitigation
With California Proposition 65 thresholds dropping down to parts-per-billion levels for Lead (Pb), Cadmium (Cd), Arsenic (As), and Mercury (Hg), advanced ion-exchange resin washings and specialized filtration are becoming mandatory in supplier qualification.
Industrial Scale & Capacity
Integrated GMP Production Infrastructure
From botanical raw material extraction to high-speed cleanroom packaging lines: Shaanxi ESNO Biotech Co., Ltd.
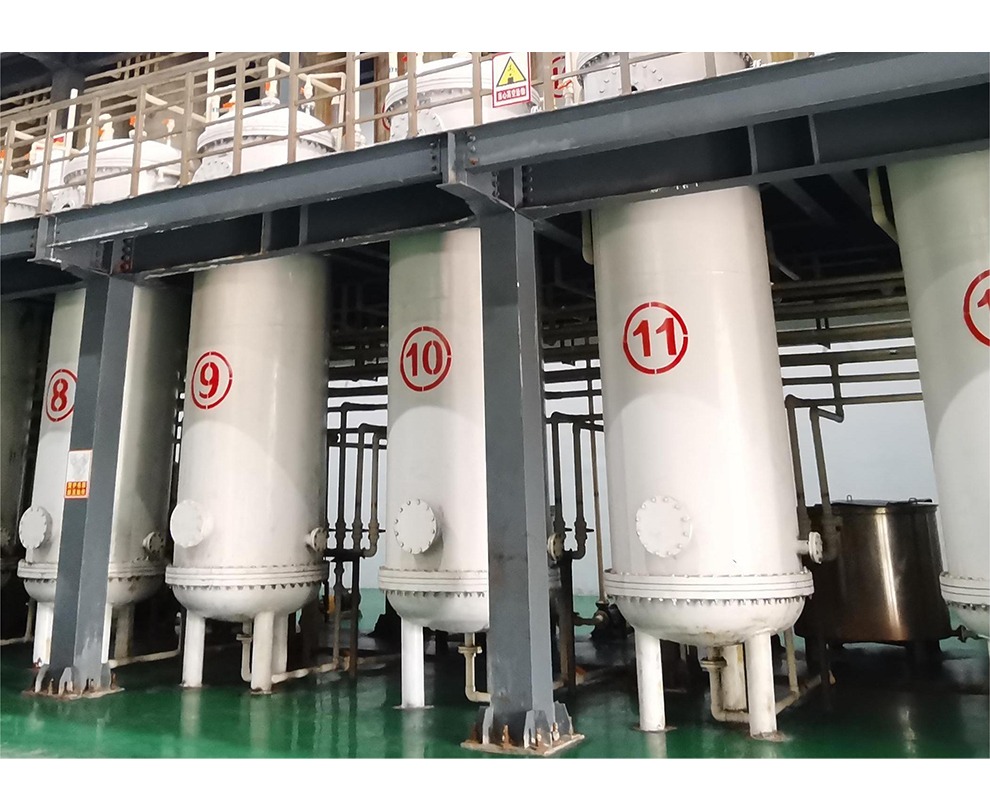
Headquartered in Xi'an, Shaanxi, ESNO Biotech operates fully validated Class 100,000 cleanroom workshops equipped with advanced multi-functional extraction tanks, low-temperature vacuum evaporators, micro-mesh granulation systems, and automated capsule filling arrays. Our site has been independently audited and verified on-site by TÜV Rheinland, fulfilling the requirements for NSF 455-2 GMP, ISO 22000, HACCP, and EU/USDA Organic standards.
Class 100,000 GMP Extraction & Compounding Cleanroom
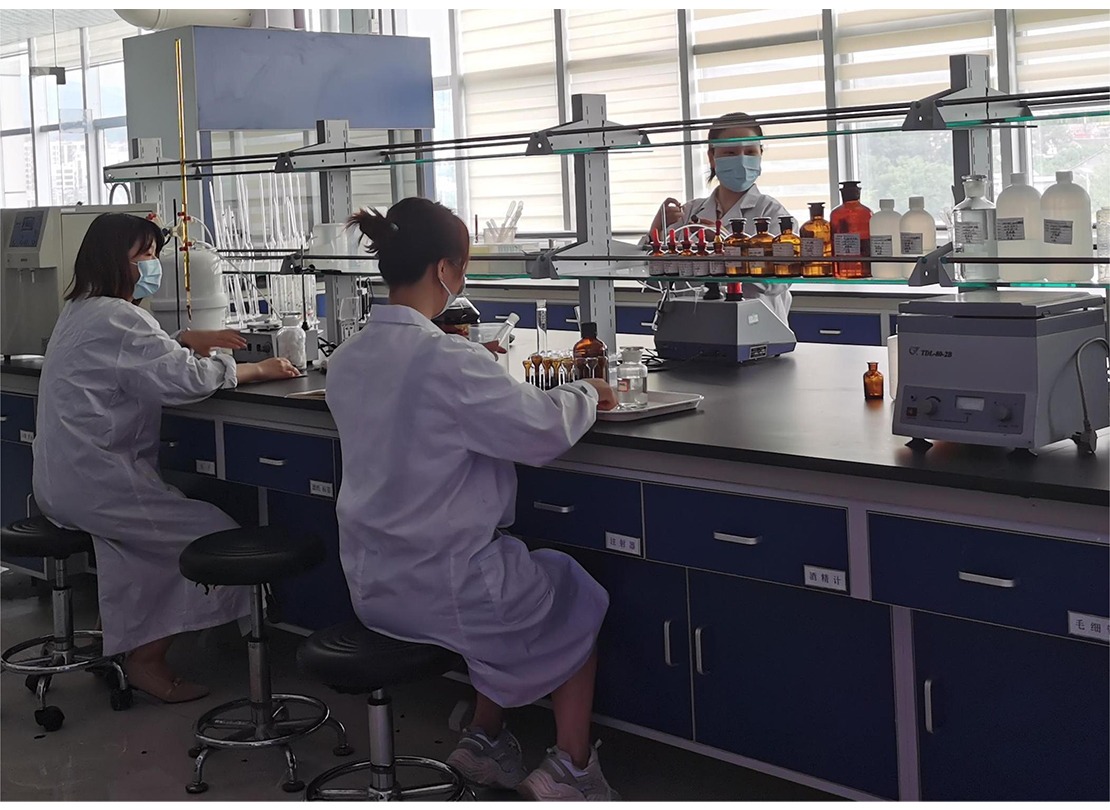
In-House Analytical & Microbiological Testing Laboratory
Automated High-Speed Encapsulation & Bottling Lines
Procurement Intelligence FAQ
Frequently Asked Questions by Global Sourcing Managers
Direct answers addressing chemical compliance, supplier qualification, testing protocols, and contract manufacturing logistics.
Q1: How does ESNO Biotech guarantee batch-to-batch standardized potency?
We deploy quantitative chromatographic testing (HPLC, GC, spectrophotometry) benchmarked against certified reference standards from USP and EDQM. We guarantee marker compounds—such as 3% Rosavins and 1% Salidroside for Rhodiola, or 98% Trans-Resveratrol—with zero downward variance across standard commercial orders.
Q2: What are the Minimum Order Quantities (MOQs) for custom formulated capsules and private label runs?
Standard in-stock formulated capsules start at accessible runs of 100 to 500 units. For fully bespoke custom active formulations, tailored encapsulation, custom color shells, and personalized retail box printing, our production runs typically scale from 500 to 1,000 finished boxes, offering low entry barriers for agile brands.
Q3: Can you deliver finished products compliant with California Proposition 65 heavy metal thresholds?
Yes. Our extraction methodology applies specific chelation filtration, activated carbon treatment, and ion-exchange separation, keeping lead (<0.5 mcg/day), cadmium, arsenic, and mercury well below stringent international and California Prop 65 daily exposure limits.
Q4: What technical and regulatory documentation accompanies shipments for customs clearance?
Every commercial consignment includes an authorized Batch Certificate of Analysis (COA), Allergen Declaration, Non-GMO Certification, Flow-Chart Diagram, Material Safety Data Sheet (MSDS), BSE/TSE Free Statement, and Certificate of Origin. Finished retail products also receive complete label compliance verification reviews.
Q5: Are your botanical extracts non-irradiated and ethylene oxide (EtO) free?
All our botanical powders, extracts, and finished encapsulations are sterilized utilizing supercritical heatless, clean-gas methods, or validated physical heat regimes. We adhere to a strict non-EtO and non-radiation policy, complying directly with European Union Regulation (EC) No 396/2005.
Q6: Can your technical team assist in novel ingredient compatibility and custom formula premixes?
With over 400 engineered product designs in our library, our in-house food scientists and pharmaceutical chemists evaluate active ingredient hygroscopic profiles, bulk densities, and cross-interaction risks before recommending excipients, micro-encapsulation, or delivery form adjustments.
Partner with an Audited Chinese Botanical Extract Manufacturer
Request comprehensive specification sheets, analytical COAs, bulk quotations, and technical formulation samples.