Precision Botanical & Nutraceutical Formulations
Engineered via high-shear botanical extraction, clean-label agglomeration, and validated active bioavailability.
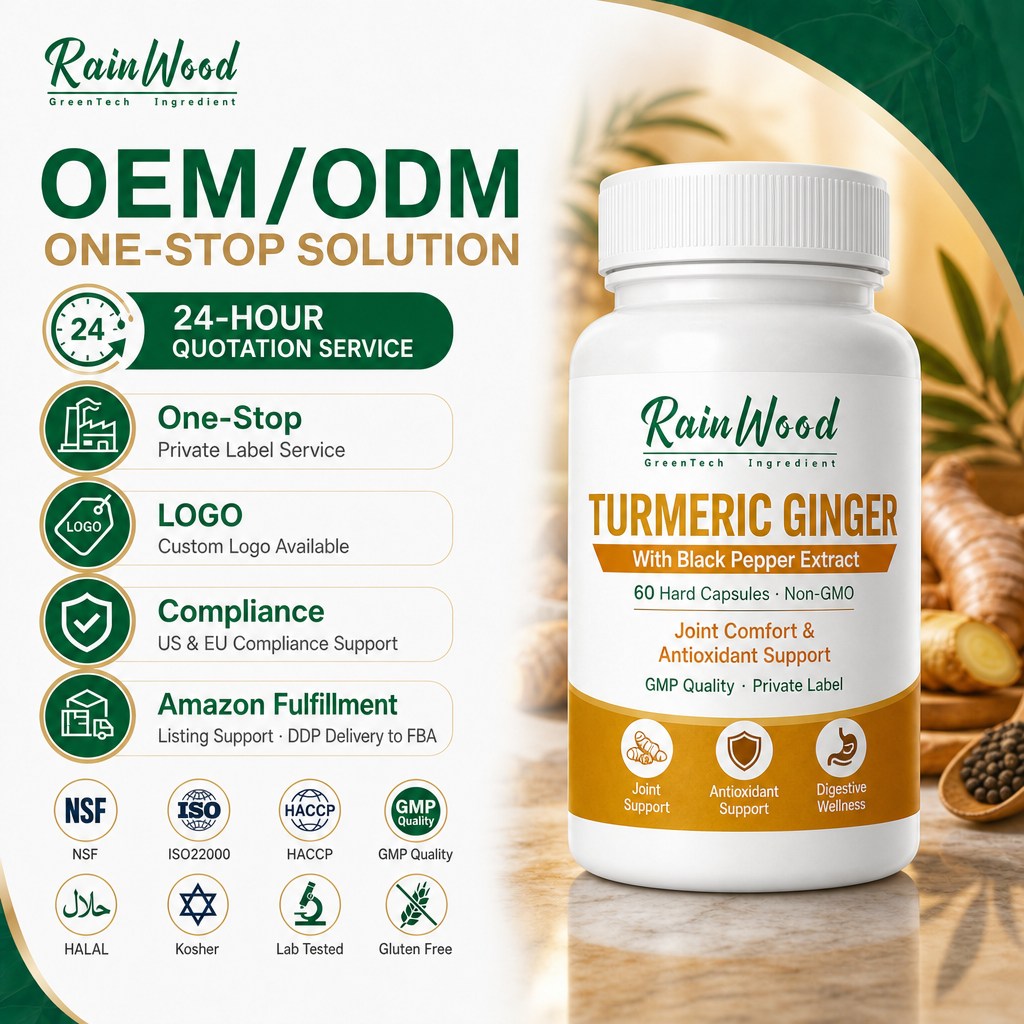
GMP Pure Turmeric Ginger Black Pepper Extract Hard Capsules 60 Count OEM Private Label
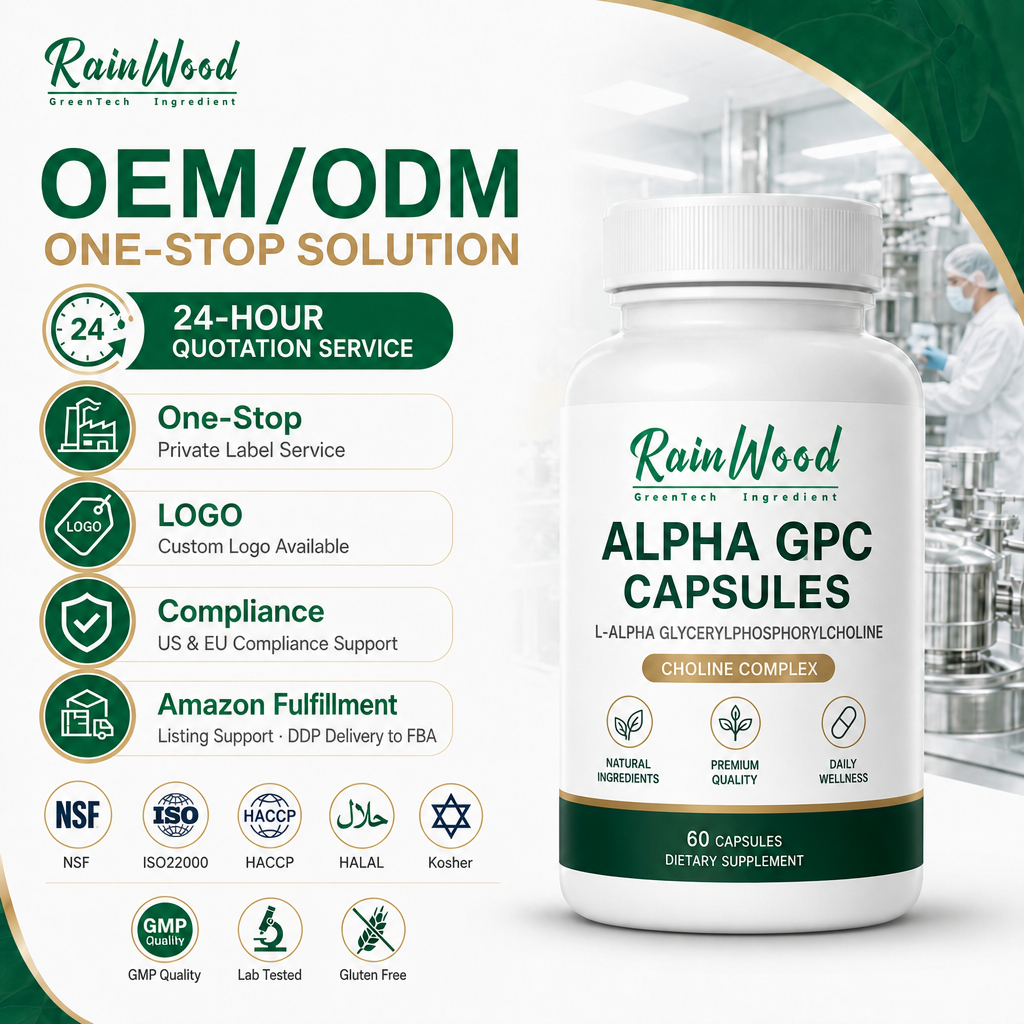
GMP Alpha GPC L-Alpha Glycerylphosphorylcholine Hard Capsules 60 Count Brain Supplement
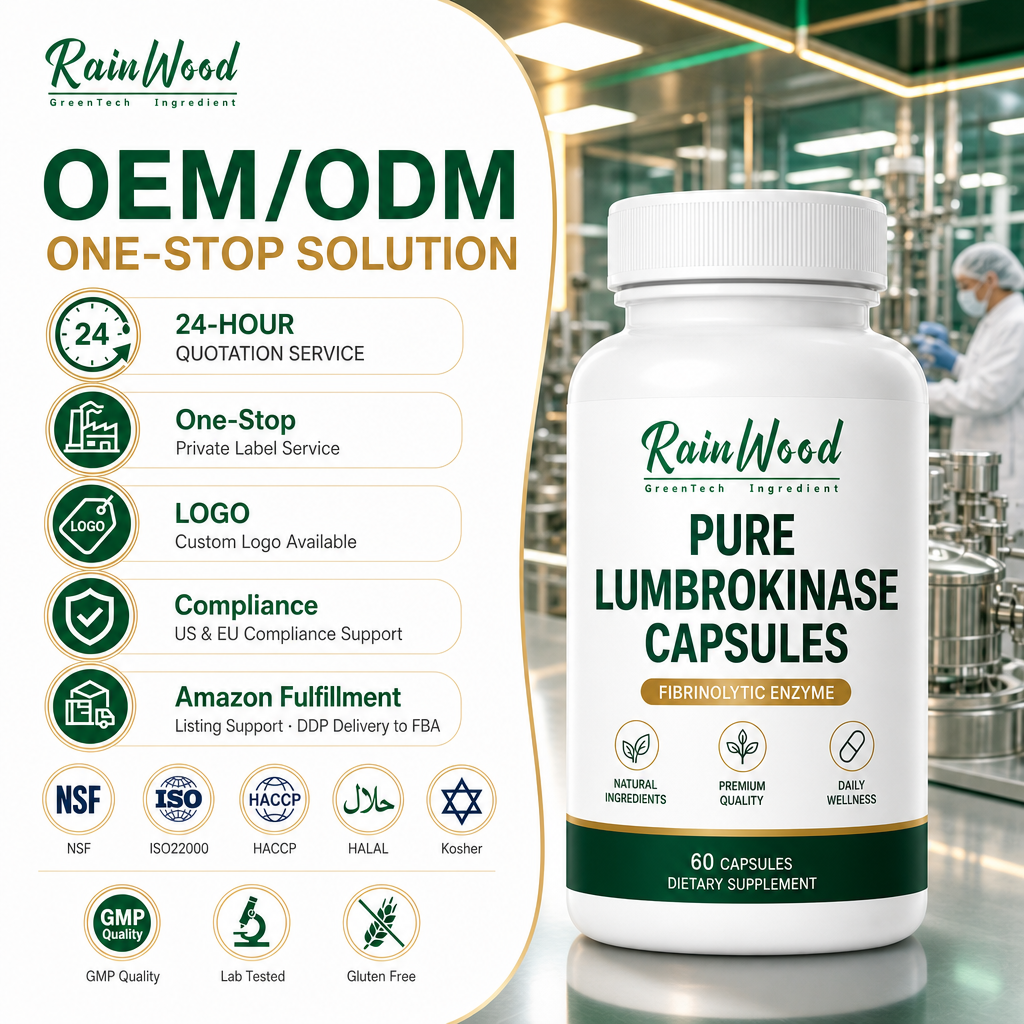
GMP Pure Lumbrokinase Fibrinolytic Enzyme Hard Capsules 60 Count OEM Custom Supplement
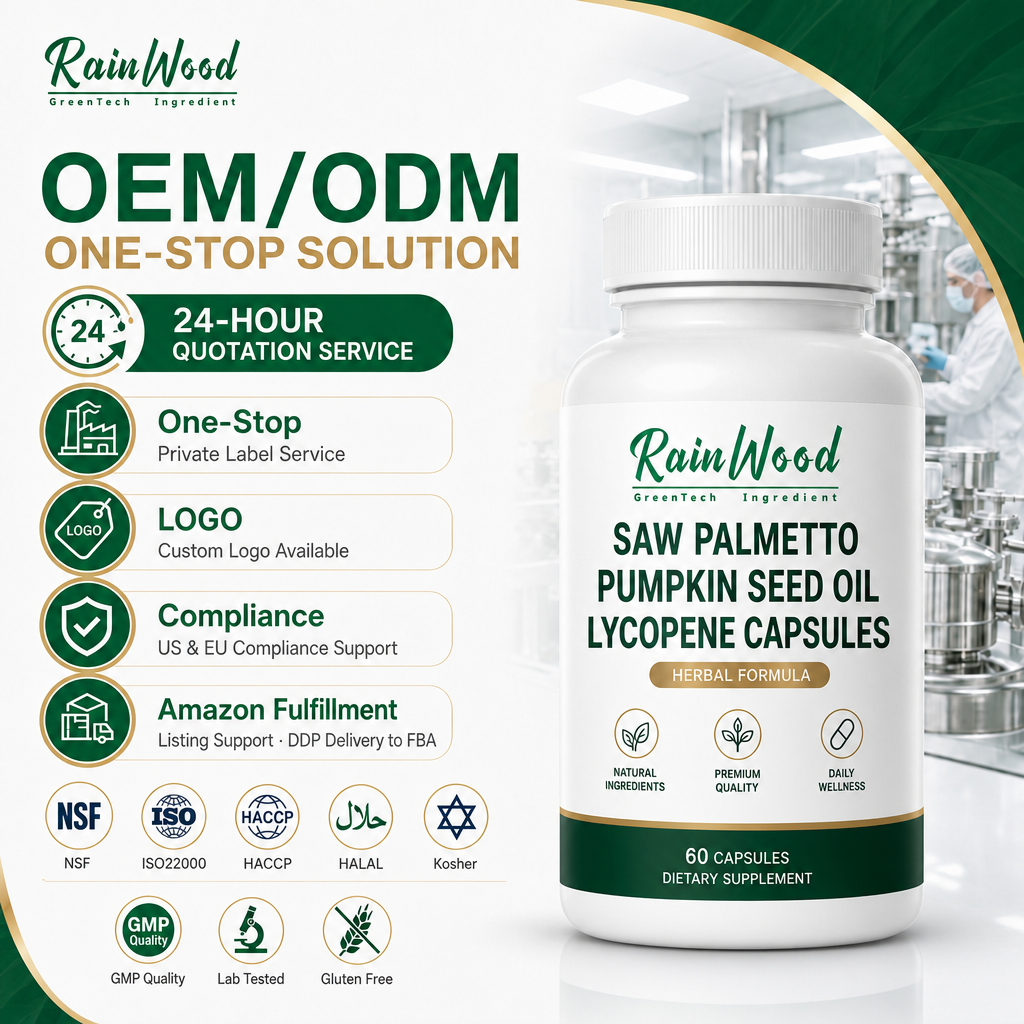
GMP Saw Palmetto Pumpkin Seed Oil Lycopene Hard Capsules 60 Count Men's Formula
GMP Magnesium Glycinate L-Theanine Apigenin Hard Capsules 60 Count Sleep Complex
OEM ODM Calcium Magnesium Zinc Vitamin D3 Capsules Private Label Mineral Supplement
GMP Pure Myo-Inositol D-Chiro Inositol 40 to 1 Hard Capsules 60 Count Supplement Box
GMP Pure Magnesium Glycinate Citrate Taurate Apigenin Hard Capsules 60 Count Sleep
19 Years of Validated Nutraceutical Engineering
Operating from Xi'an, Shaanxi since 2006, Shaanxi ESNO Biotech Co., Ltd. delivers direct-from-source agricultural extraction and sterile finished-form contract manufacturing.
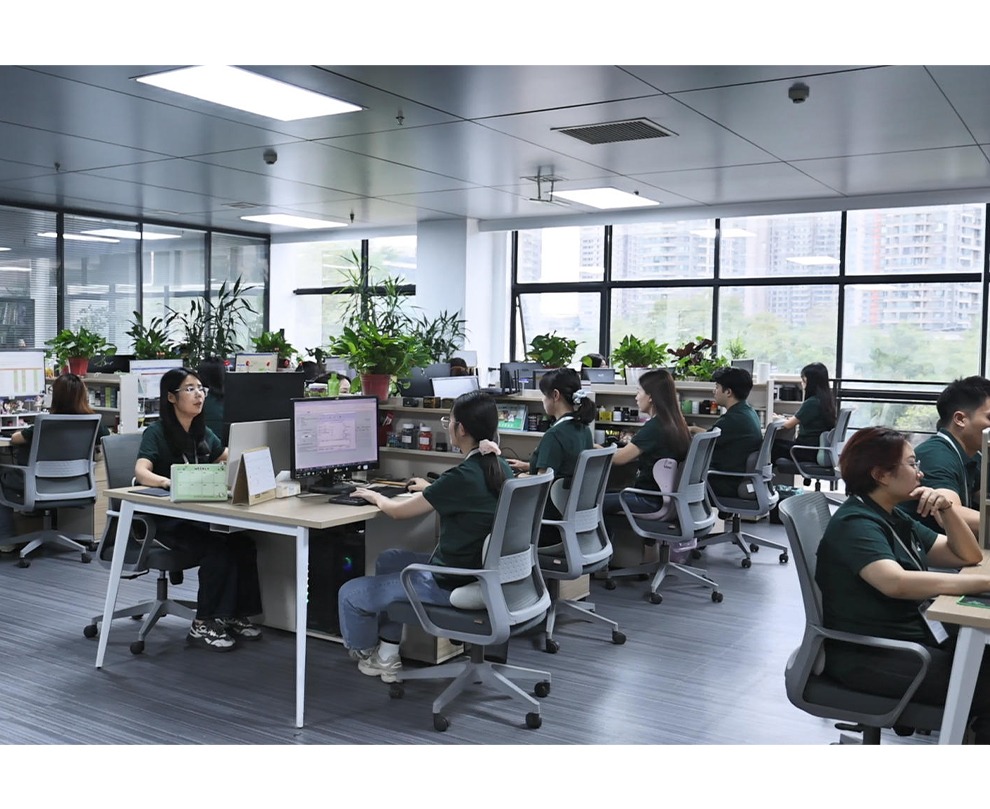
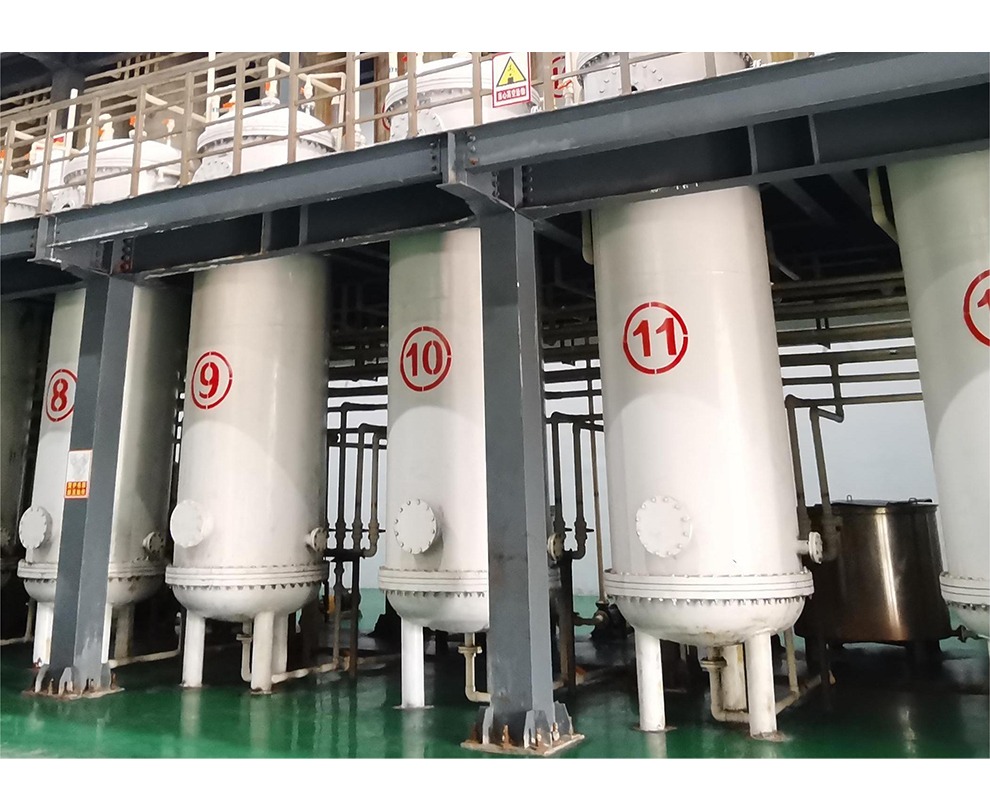
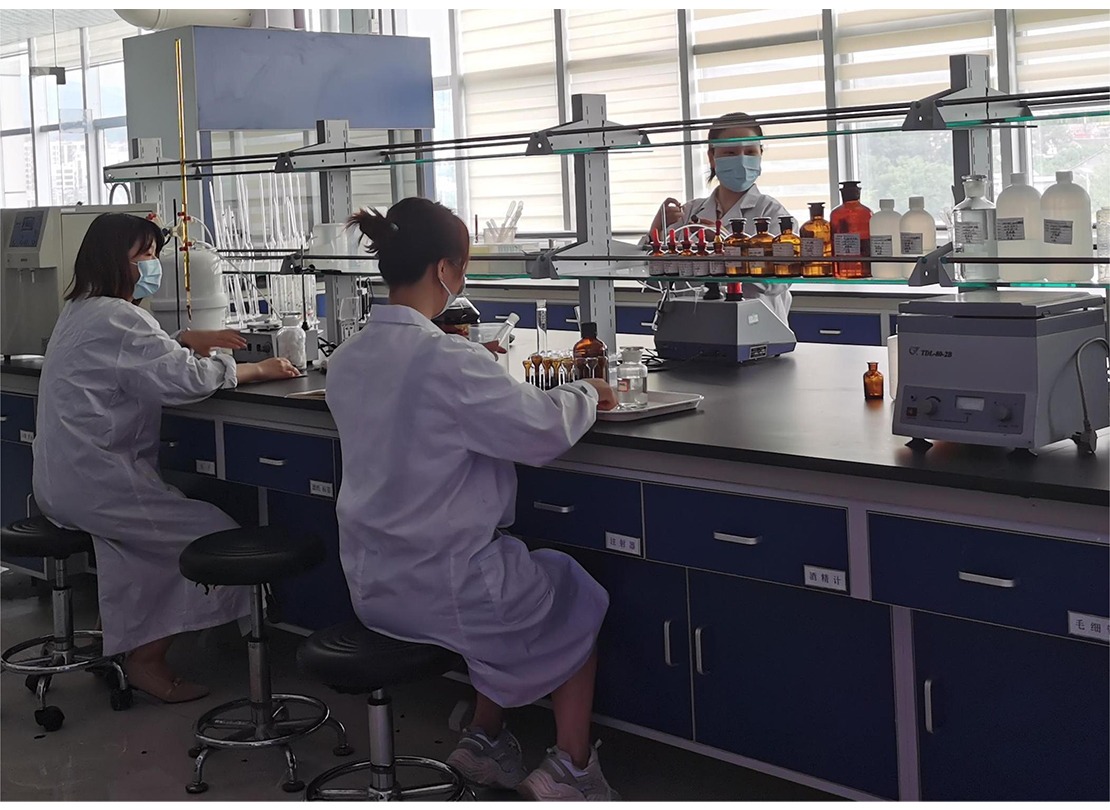
In global botanical processing, true quality control cannot be outsourced. By controlling our raw botanical sources in Shaanxi—the epicenter of China's Qinba Mountain medicinal flora reserve—and executing rigorous secondary processing under NSF 455-2 GMP, ISO 22000, and HACCP frameworks, we provide brand partners with uncompromised batch stability. The facility is verified on-site by TÜV Rheinland, allowing enterprise clients in North America, the European Union, Australia, and the Middle East to bypass intermediate trading houses and secure direct-from-source traceability.
Technological Paradigms: From Raw Milled Herbs to Standardized Molecular Isolates
How cutting-edge industrial drying, clean-solvent extraction, and nano-agglomeration are reshaping organic plant powder manufacturing.
The botanical powder industry has crossed a decisive threshold. The historic paradigm, characterized by mechanical crushing and pulverization of whole crude plants, resulted in severe bulk density instability, excessive microbiological contamination, and unstandardized active marker yields. Today, leading Chinese manufacturing hubs operate at the nexus of biochemical standardization and organic integrity.
1. Kinetic Low-Temperature Supercritical CO₂ and Hydro-Ethanolic Countercurrent Extraction
Traditional thermal evaporation frequently degrades thermosensitive phytocompounds such as polyphenols, ginsenosides, and active terpenes. Modern extraction relies on countercurrent automated solvent arrays operating under nitrogen blanketing, followed by supercritical CO₂ separation. This mechanical architecture ensures that bioactive plant metabolites are isolated without solvent toxicity, meeting both USDA Organic and European Commission EC 834/2007 non-irradiation standards.
2. Fluidized-Bed Agglomeration and Microencapsulation of Hydrophobic Actives
Botanical extracts such as 95% Curcumin, Apigenin, and Saw Palmetto lipids are inherently hydrophobic, suffering from dissolution limits and erratic gut bioavailability. Through precision fluidized-bed agglomeration, our technical teams introduce organic carrier matrices (such as organic tapioca maltodextrin or sunflower lecithin) to create water-dispersible granules that resist oxidation, prevent caking, and compress smoothly during high-speed encapsulation without synthetic anti-caking silicates.
3. Cryogenic Micronization and Laser Particle Sizing
Physical particle uniformity directly determines bioavailability and capsule fill uniformity. Employing liquid-nitrogen-cooled pin mills and jet micronization, plant matrices are refined to mesh sizes ranging from 80 to 200 mesh (D90 < 75 µm). Particle uniformity prevents density separation in multi-ingredient blends—vital for maintaining exact dose uniformity in complexes containing micro-actives like Lumbrokinase or Lycopene alongside dense botanical powders.
Chromatographic HPLC Fingerprinting
Every active marker—from Curcuminoids to D-Chiro-Inositol—is identified via high-pressure liquid chromatography to ensure exact potency retention per finished capsule.
Heavy Metal Stripping & ICP-MS Assay
Inductively Coupled Plasma Mass Spectrometry validates compliance with California Proposition 65 limits: Lead < 0.5 ppm, Arsenic < 1.0 ppm, Cadmium < 0.3 ppm, Mercury < 0.1 ppm.
Organic Cleanroom Agglomeration
Porous, instantly dispersible botanical granules designed specifically for clean-label capsule filling lines without the addition of magnesium stearate or talc.
Sterile Low-Temperature Spray Drying
Atomized drying chambers running below 60°C preserve delicate sensory pigments, biological enzymatic potency, and naturally occurring volatile terpenes.
Future Procurement Trends in Botanical & Organic Powders
Market dynamics, supply-chain risks, and regulatory realignments driving purchasing decisions across Fortune 500 nutraceutical brands.
Procurement teams are shifting away from fragmented spot-market buying toward dedicated API-grade contract manufacturing partnerships. Based on our transaction datasets spanning 100+ global jurisdictions, five distinct structural trends dominate modern wholesale sourcing:
1. Absolute Auditable Traceability (Source-to-Cradle)
Regulatory frameworks such as the EU Corporate Sustainability Due Diligence Directive (CSDDD) and FDA 21 CFR Part 111 mandate end-to-end transparency. Importers demand geotagged botanical harvest records, verified pesticide screening certificates (covering >500 compound screens), and non-GMO certification traceable to designated regional organic cooperatives.
2. Synergistic Multi-Active Blending at Factory Origin
Rather than importing standalone raw plant powders and incurring secondary blending fees in local Western facilities, brands are moving formula mixing directly to the primary Chinese manufacturer. Formulations such as our Magnesium Glycinate + L-Theanine + Apigenin or Turmeric + Ginger + Piperine are pre-formulated, homogenized, and encapsulated at source, cutting landed freight volume by 42%.
3. Clean-Label Excipient Elimination
Modern consumers actively reject synthetic magnesium stearate, silicon dioxide, and artificial coloring agents. Modern procurement contracts specify 100% plant-origin excipients, such as organic bamboo silica, organic rice fiber, and pullulan or HPMC vegetarian capsule shells, demanding zero-flow-aid formula validation directly from the OEM manufacturer.
4. Rapid Turnaround Small-Batch Piloting
E-commerce agility and private equity portfolios demand accelerated product iteration. Traditional MOQs of 50,000 units are being abandoned in favor of flexible 500-to-1,000-unit pilot runs. This allows direct-to-consumer and Amazon FBA brands to test custom formulas and packaging formats without overleveraging working capital or risking shelf-life degradation.
Frequently Asked Questions: Global Sourcing & Compliance
Detailed technical, operational, and regulatory answers addressing the primary friction points encountered during supplier qualification.
What specific documentation is issued with each shipment to satisfy FDA and EU custom border inspections?
How does ESNO Biotech guarantee the authenticity and non-adulteration of standardized herbal extracts?
What are your standard Minimum Order Quantities (MOQs) for custom formulated capsules versus bulk plant powders?
Can you manufacture vegan-certified, organic, and clean-label dietary supplement capsules?
What is the typical production timeline from formula sign-off to shipment dispatch?
How are stability and shelf-life verified across international export routes?
Why Tier-1 Global Supplement Brands Choose ESNO Biotech
Combining primary agricultural raw material leverage with advanced pharmaceutical-grade contract processing capabilities.
Raw Material Extraction Primacy
Directly headquartered adjacent to Shaanxi's botanical farming regions, cutting raw commodity costs, removing intermediary brokers, and giving brand owners genuine price leadership.
End-to-End In-House R&D
Over 400 commercialized market designs. Our formulation scientists optimize organoleptic profiles, solve moisture degradation, and formulate for maximum human bioavailability.
Rigorous Global Compliance Audits
Fully compliant with NSF 455-2 GMP, ISO 22000, HACCP, USDA Organic, and verified on-site by TÜV Rheinland. Export-ready documentation ensures zero customs delays.
Dedicated Enterprise Account Management
No fragmented middle agents. A dedicated bilingual formulation engineer coordinates your project through raw batch staging, laboratory testing, and final customs dispatch.
Launch or Scale Your Botanical Product Portfolio
Connect with our technical formulation team for rapid feasibility assessments, custom batch quotes, and sample requests. Direct factory pricing with validated GMP documentation.