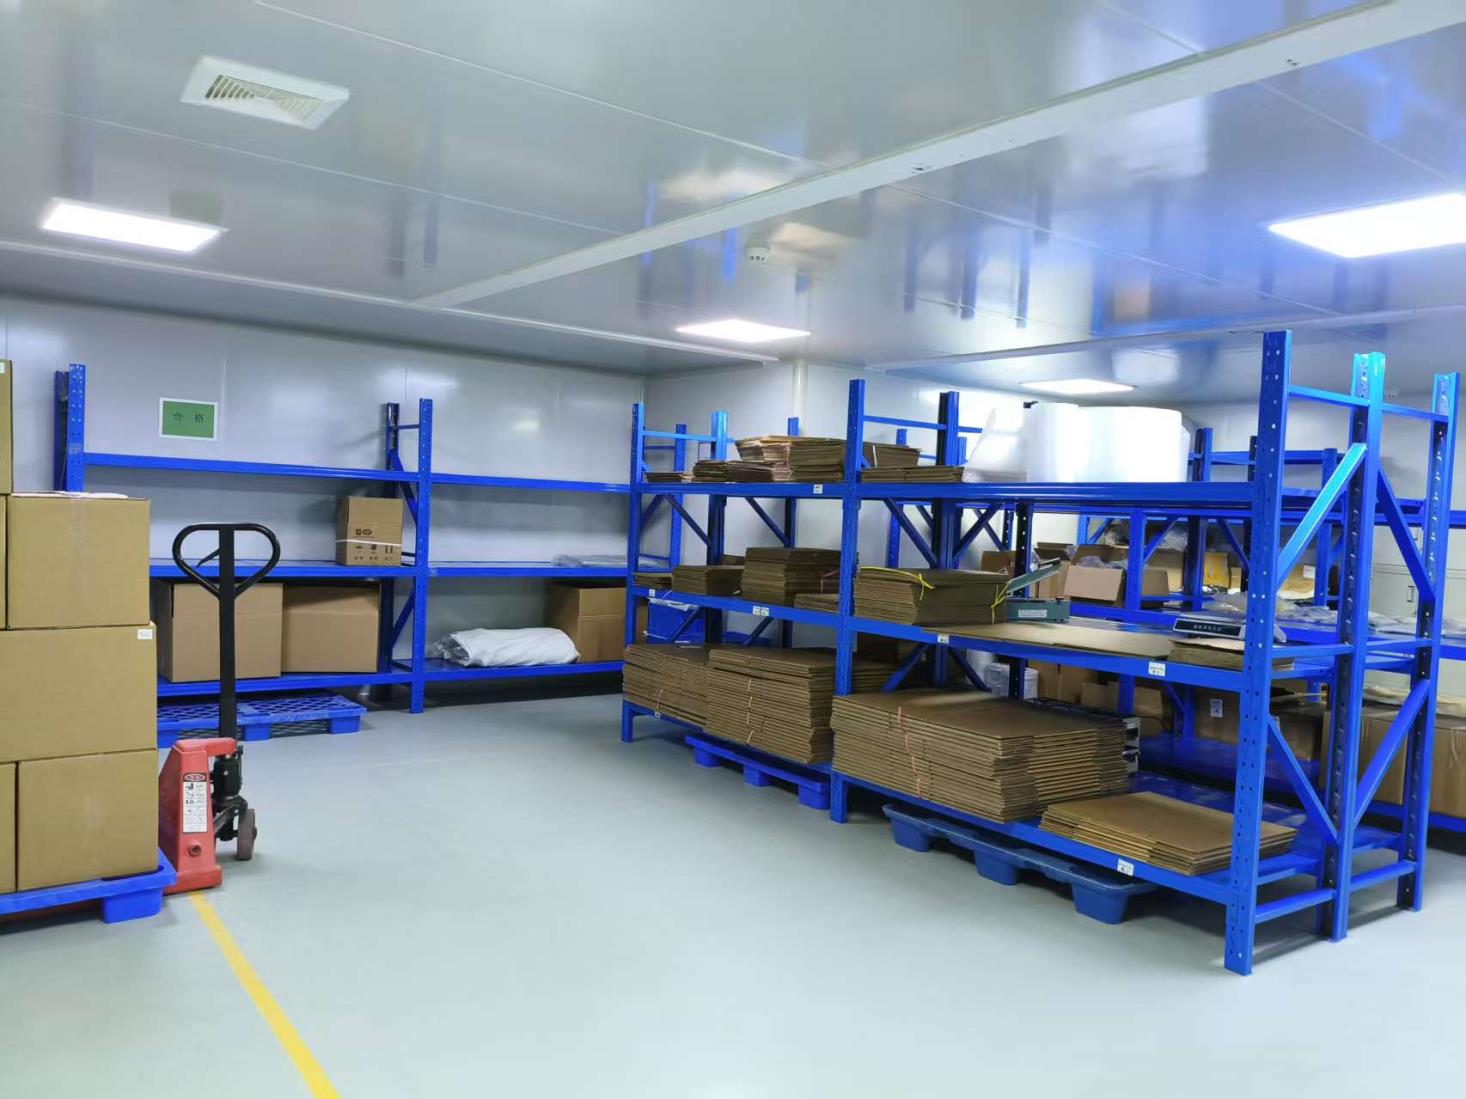
STAGE 01
Raw Material
Identity, potency, and purity verification upon intake quarantine.
Independent third-party audits and quantitative fulfillment metrics provide global procurement directors with transparent, verified supply chain stability.
Headquartered in Xi'an High-Tech Zone, Shaanxi ESNO Biotech Co., Ltd. maintains registered cleanrooms, specialized production workshops, and an on-site quality assurance lab to fulfill international food and pharmaceutical standards.
Our export distribution spans over 100 countries, with deep compliance experience across major North American, European, and Asia-Pacific customs regimes.
Every batch follows standard operating procedures (SOPs) from botanical raw material quarantine to cleanroom packaging and final export containerization.
Identity, potency, and purity verification upon intake quarantine.
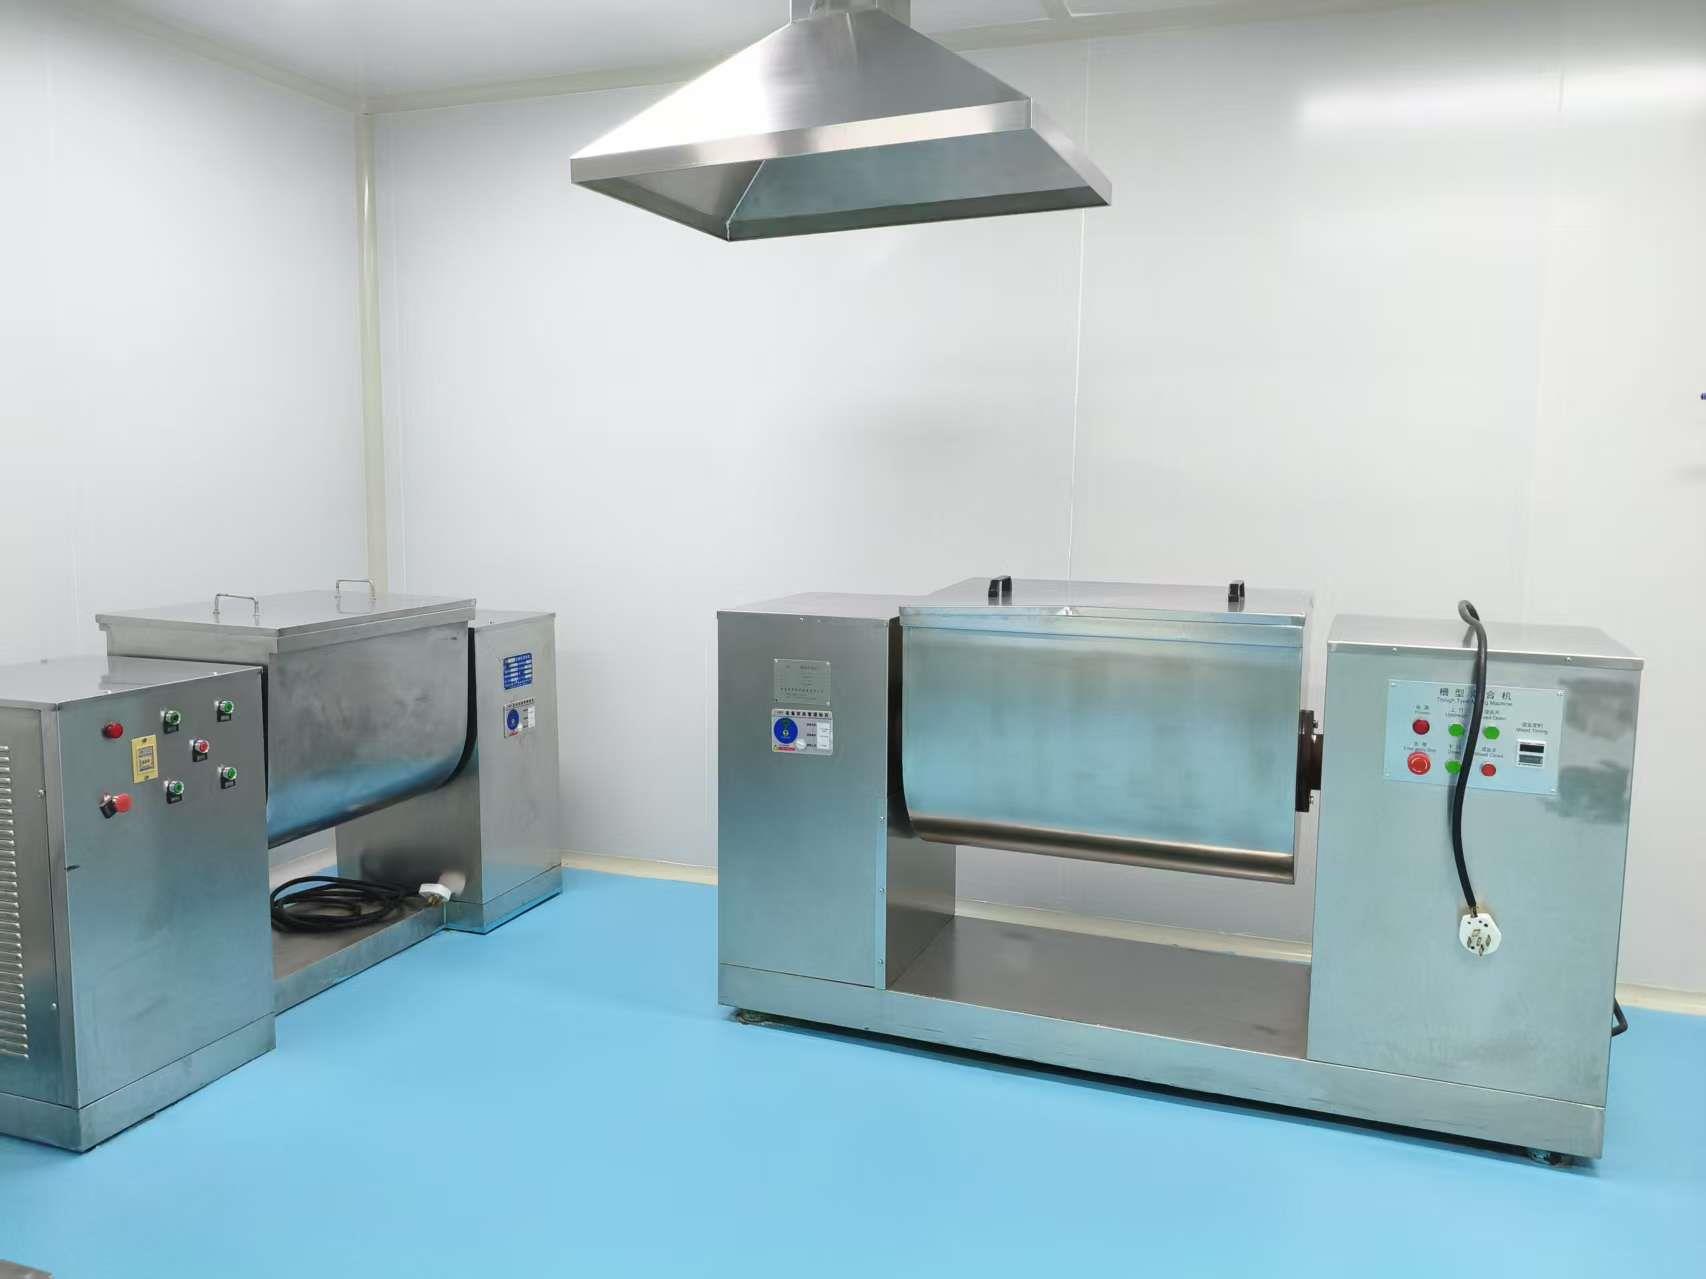
3D homogeneous powder blending of actives and excipients.
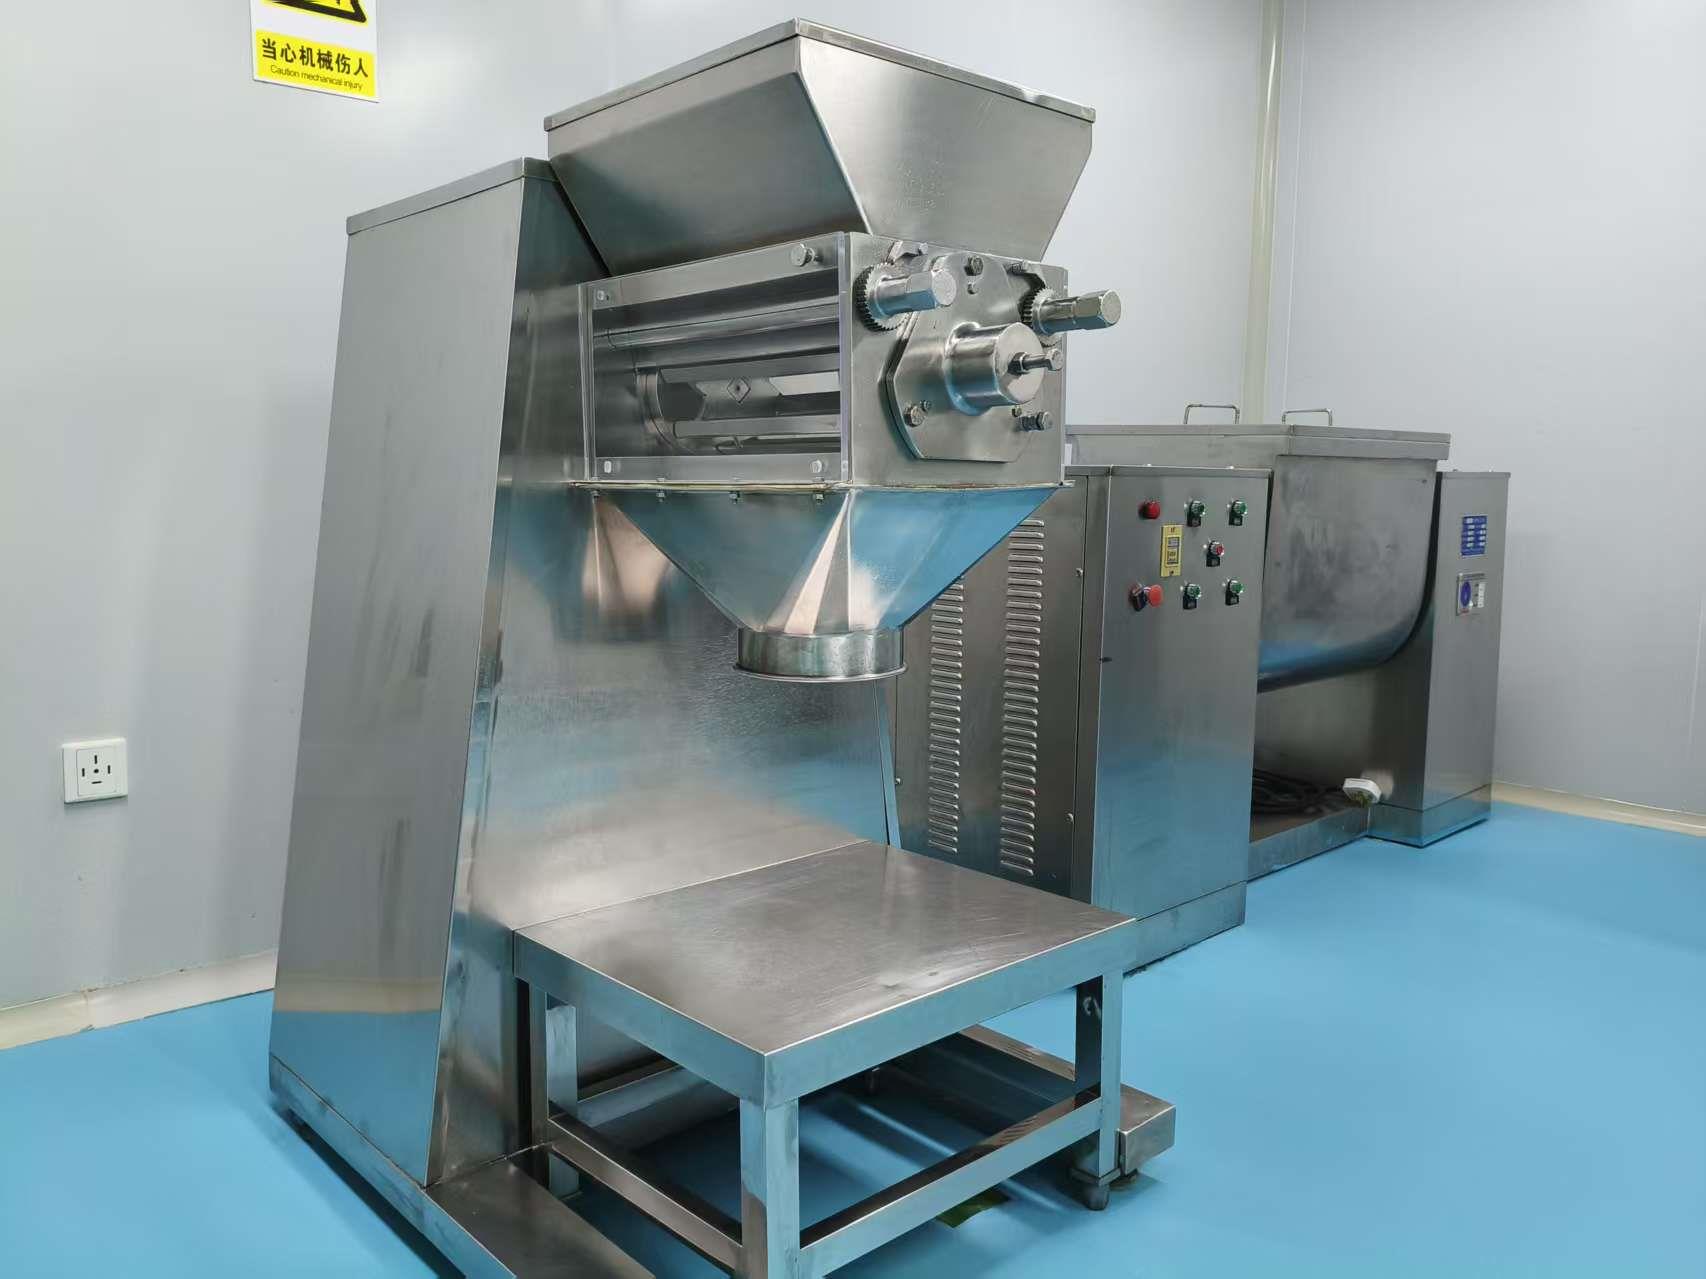
Granule formation to ensure optimal flowability and density.
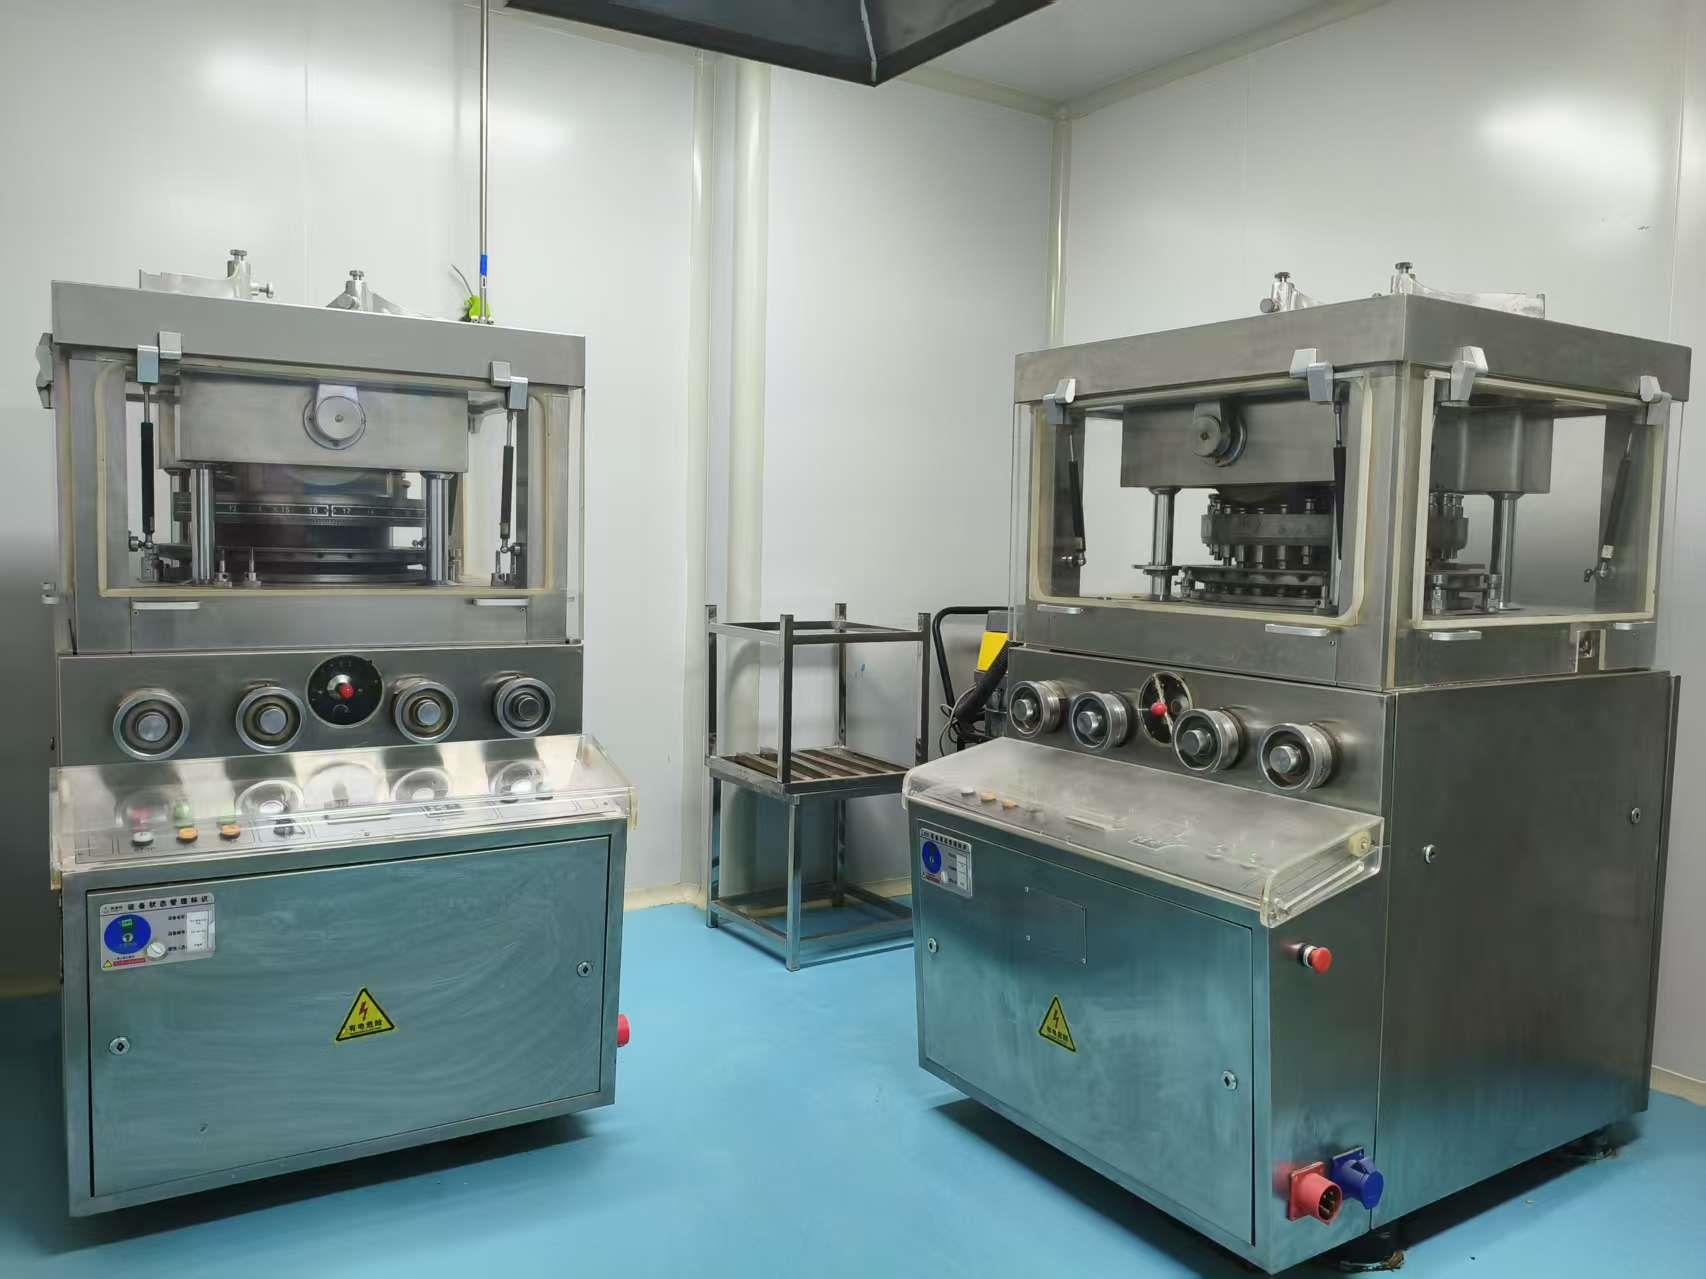
Rotary press compression with continuous weight and friability testing.
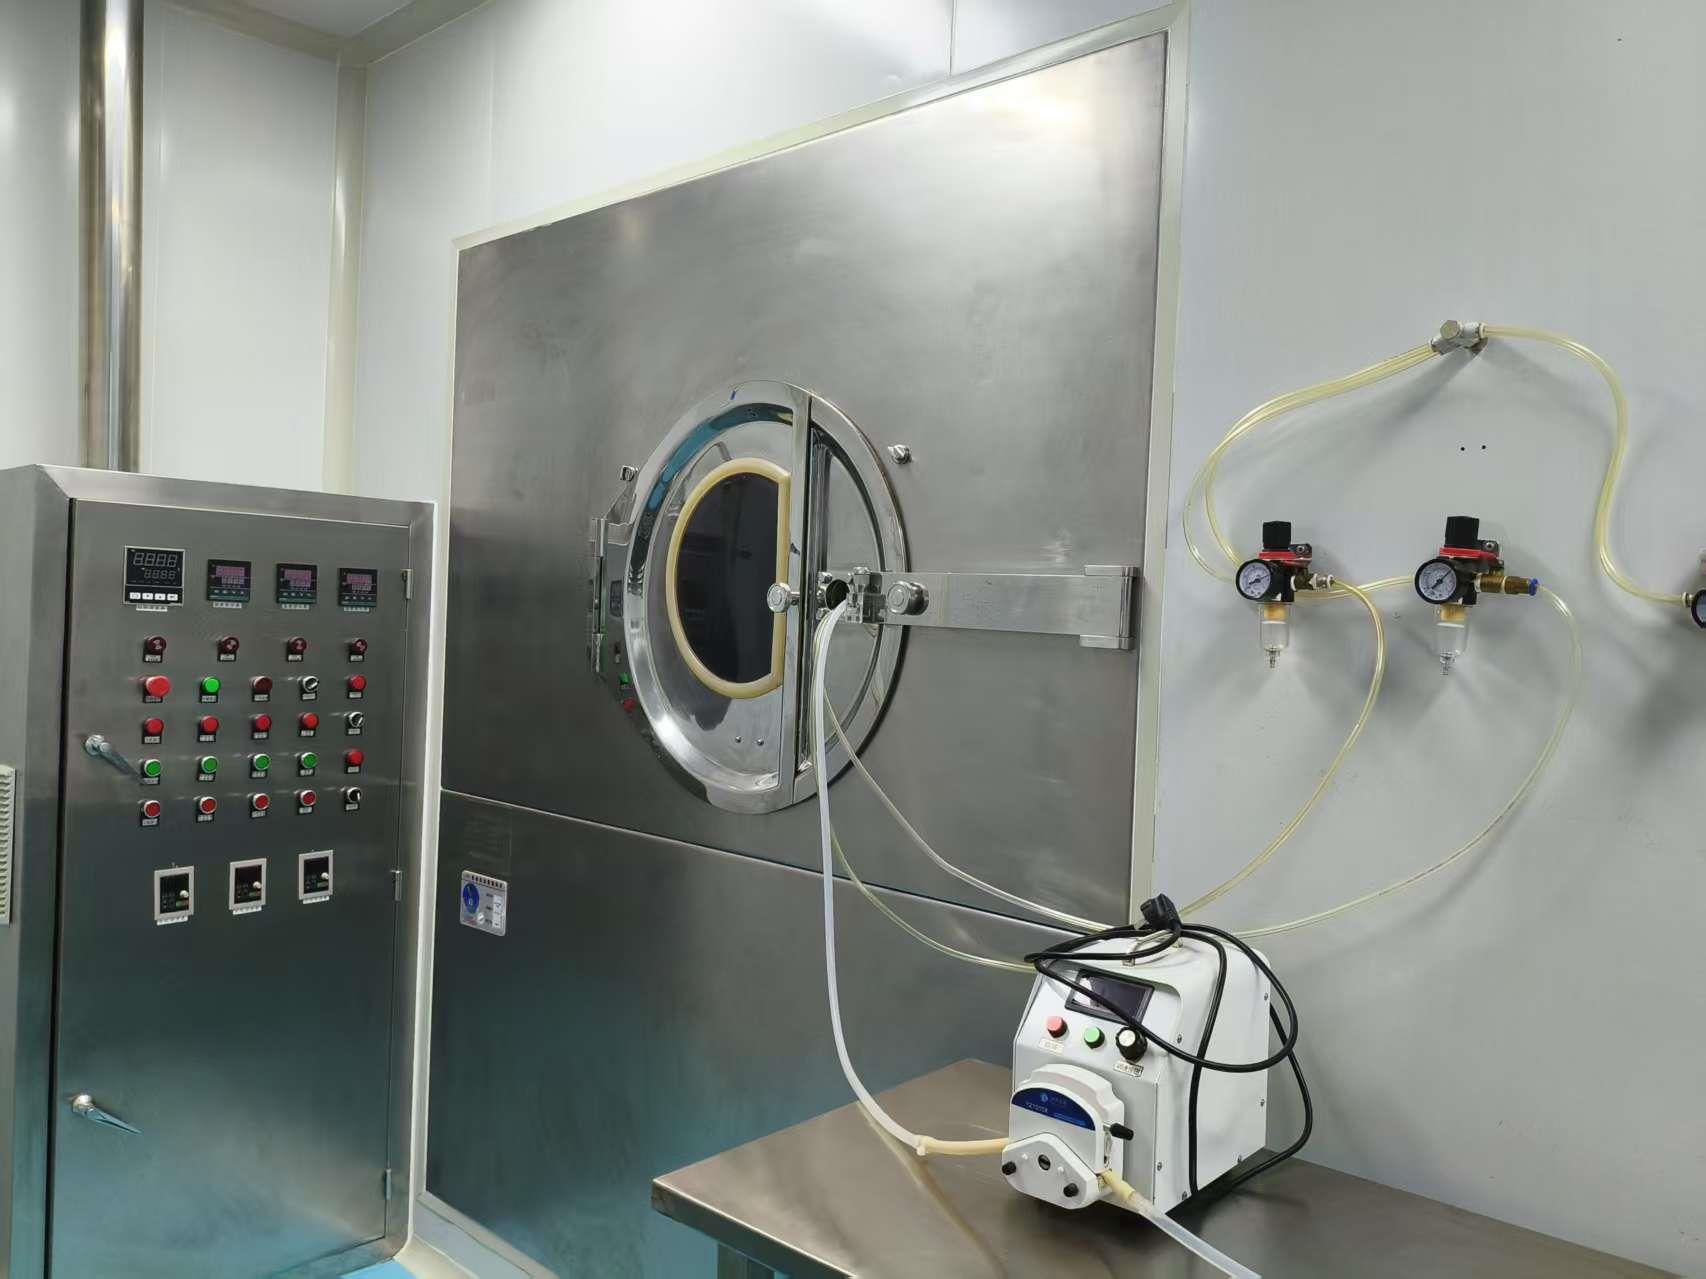
Enteric and film coating for stability, swallowability, and branding.
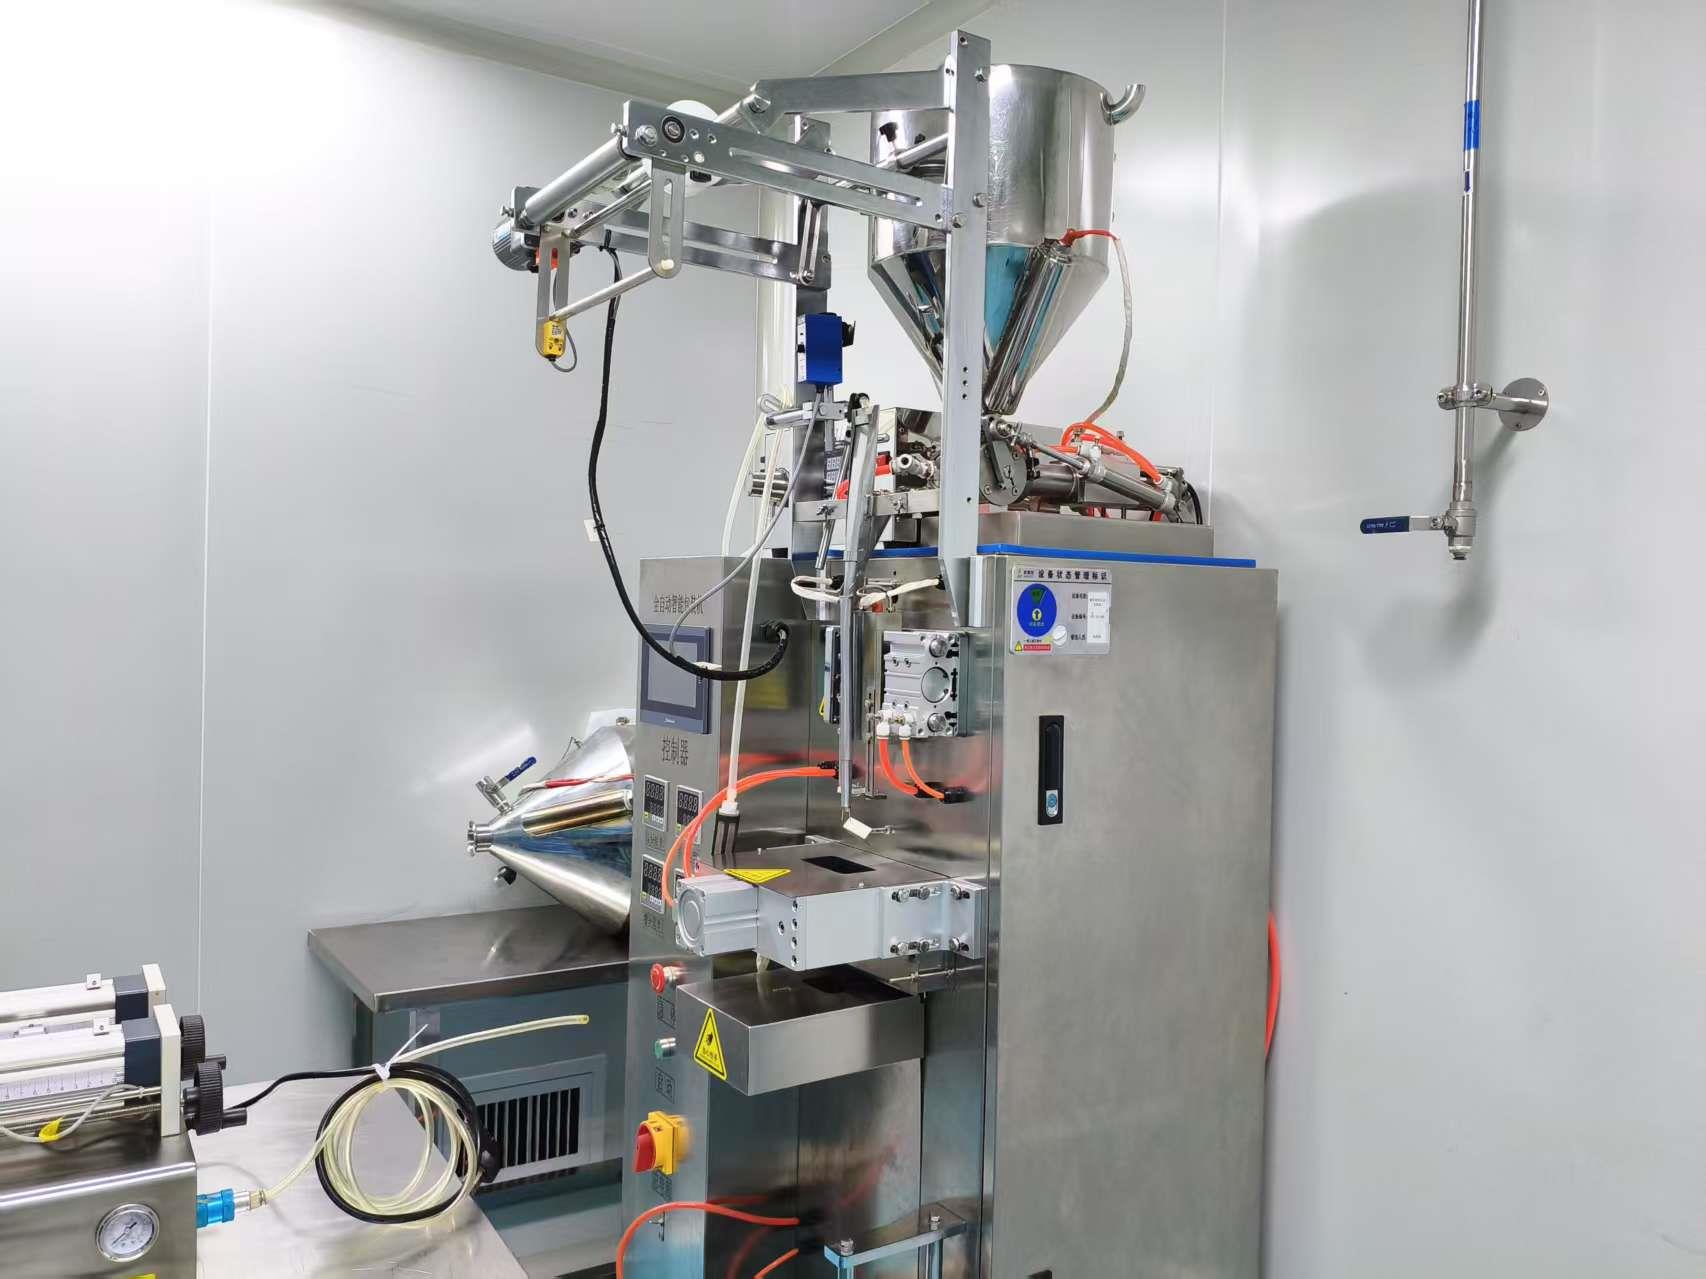
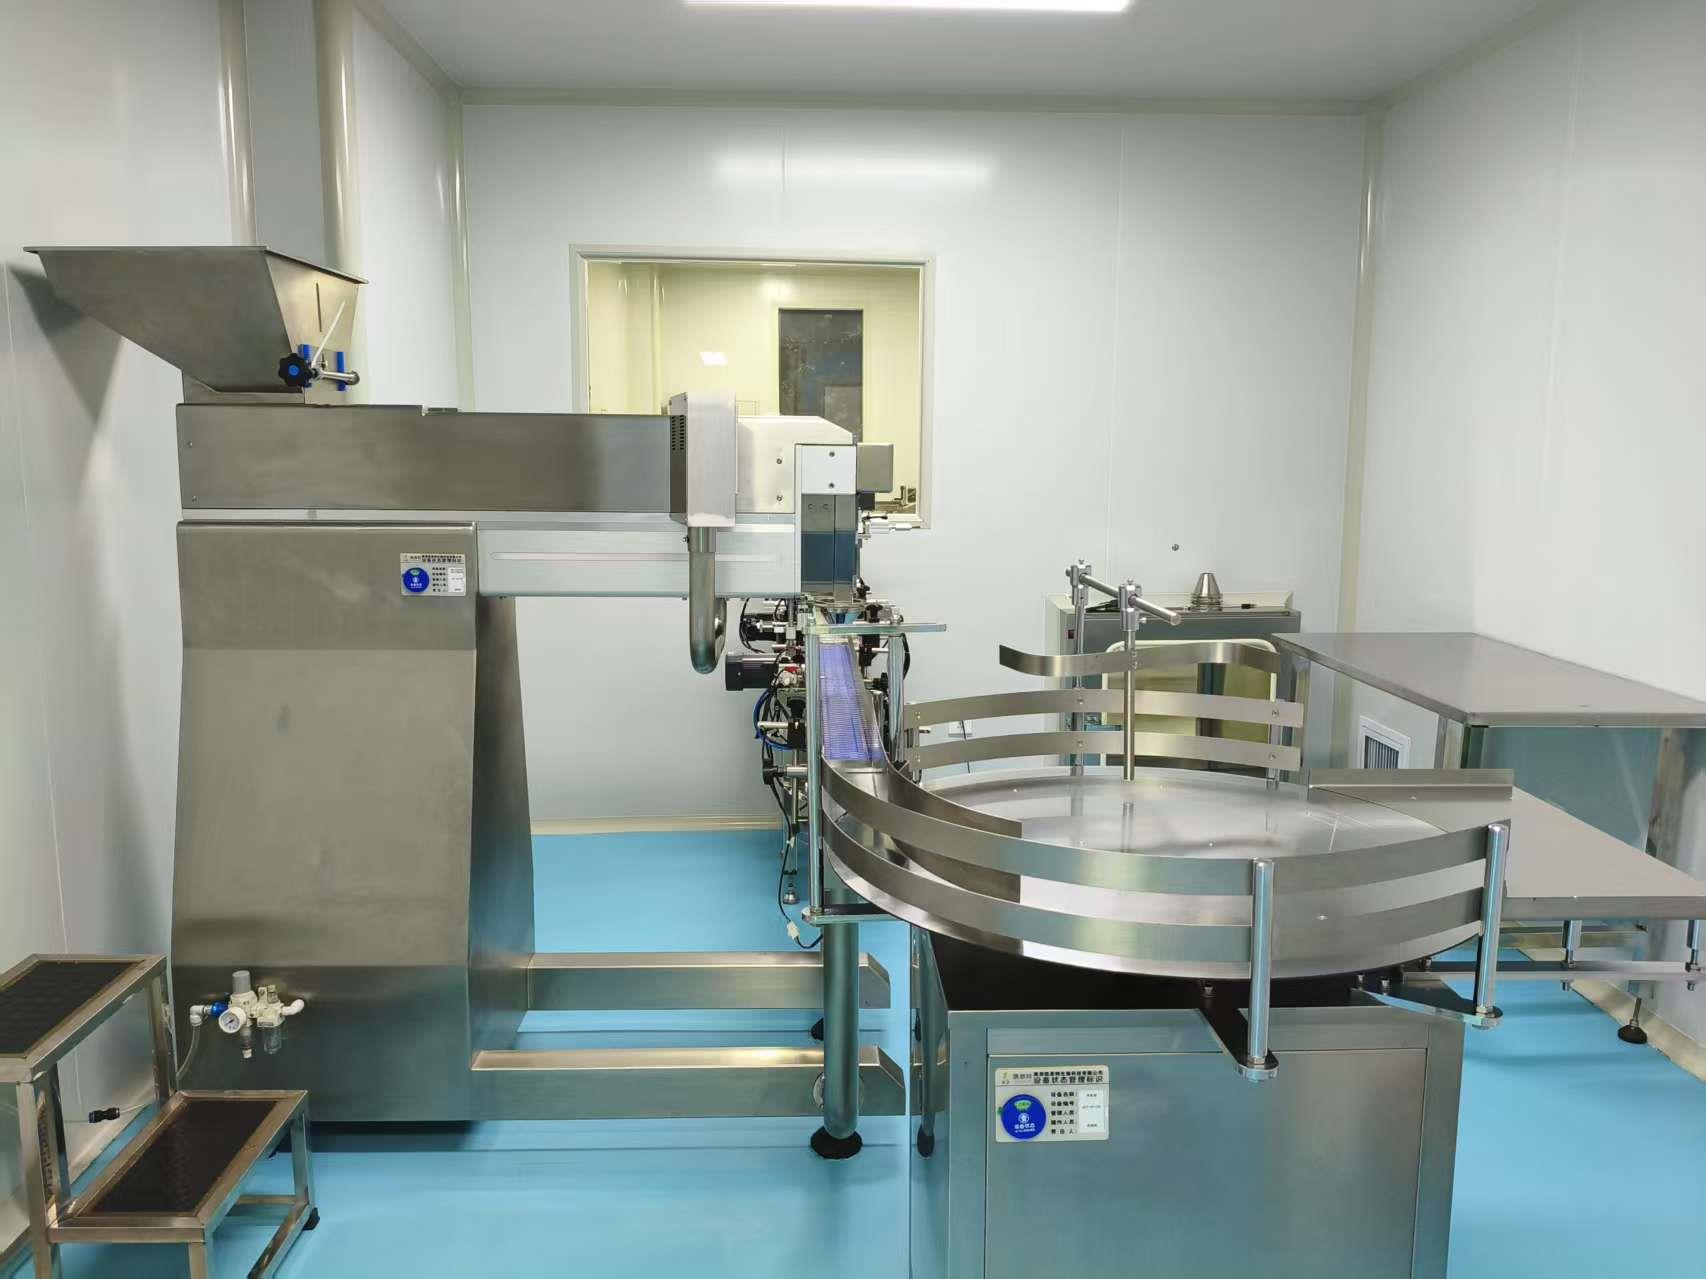
High-precision dosing for hard capsules, bottles, and sachets.
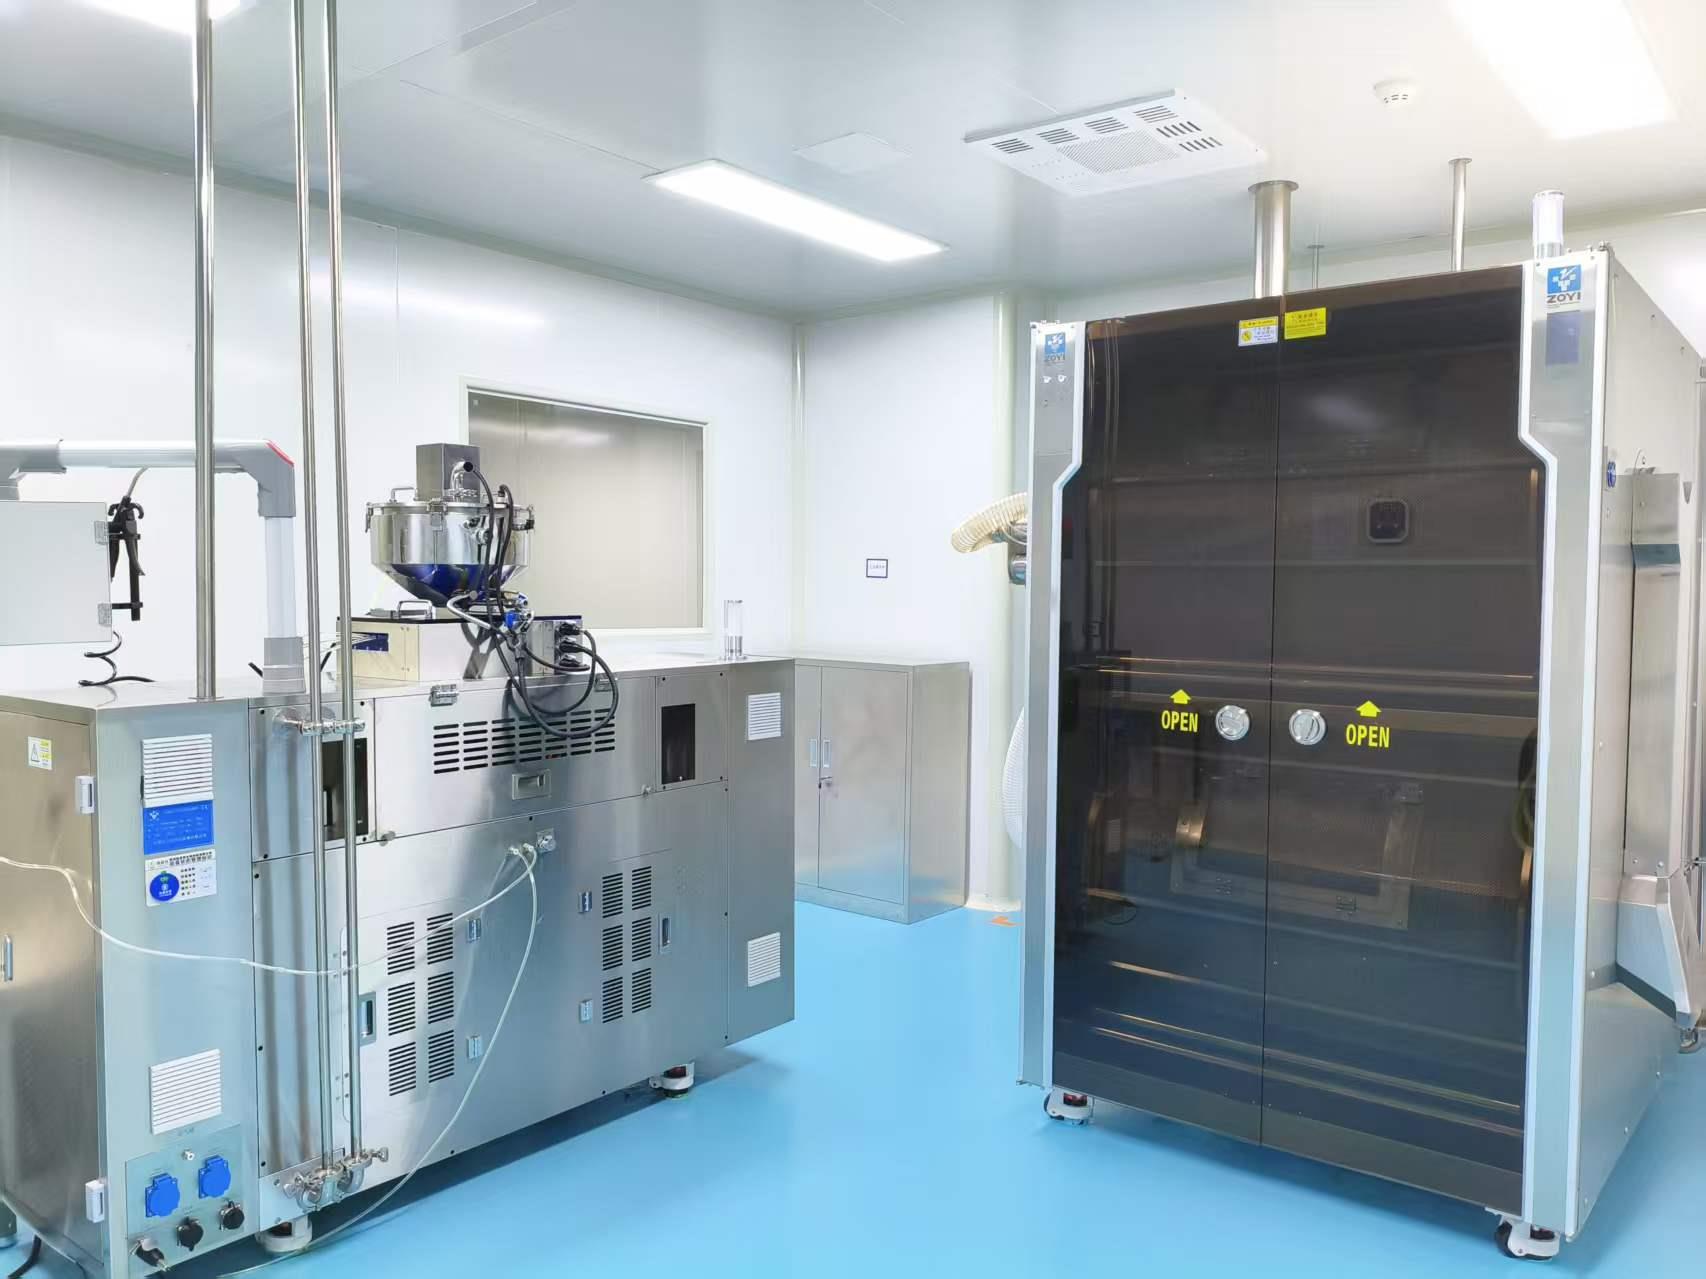
Specialty compression for shilajit balls and functional spheres.
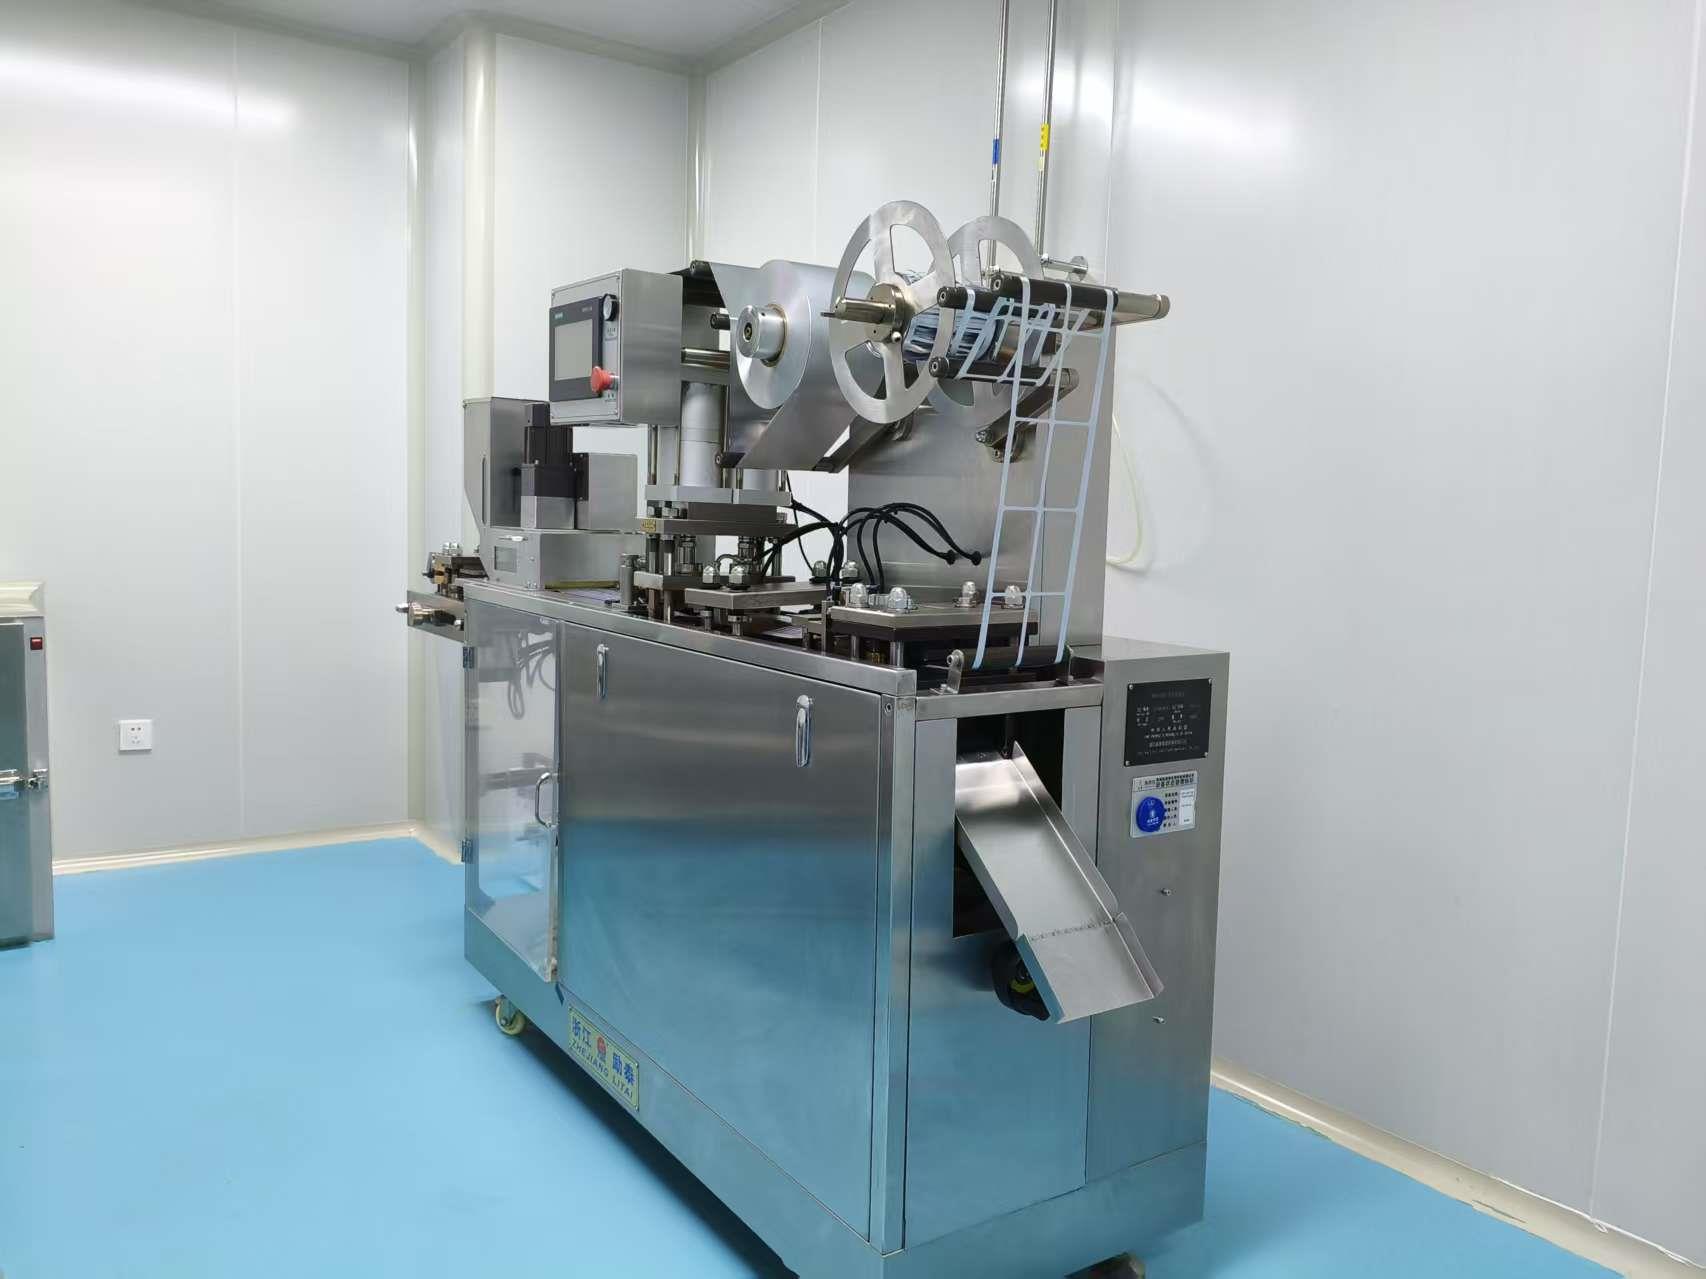
Cleanroom blister formation and foil heat-sealing operations.
Automated private labeling, batch coding, and tamper-evident sealing.
Heavy-duty master carton packing and pallet wrapping for export.
Our facility operates modern, automated pharmaceutical machinery designed to ensure batch consistency, reduce lead times, and maintain zero-defect standards.
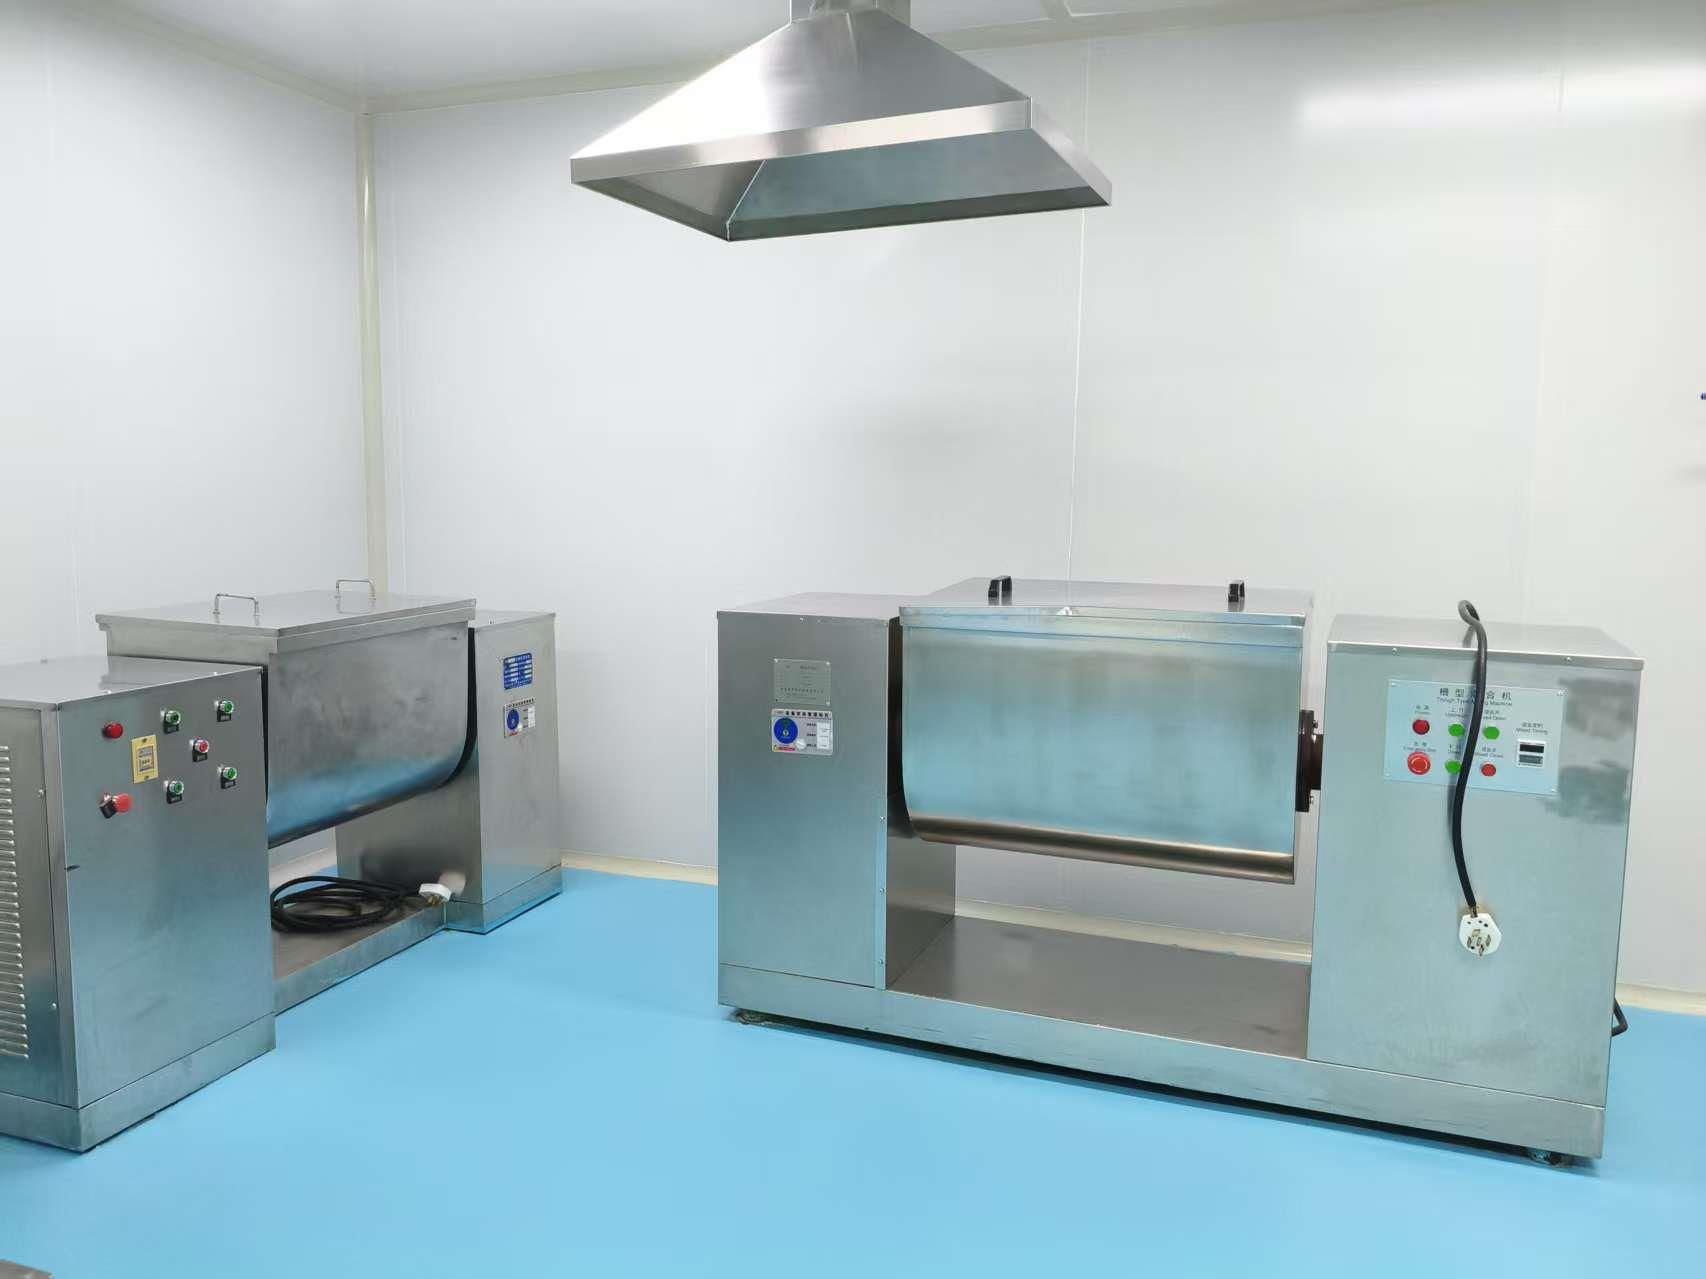
High-efficiency ribbon and V-blenders ensuring even distribution of low-dose active botanicals.
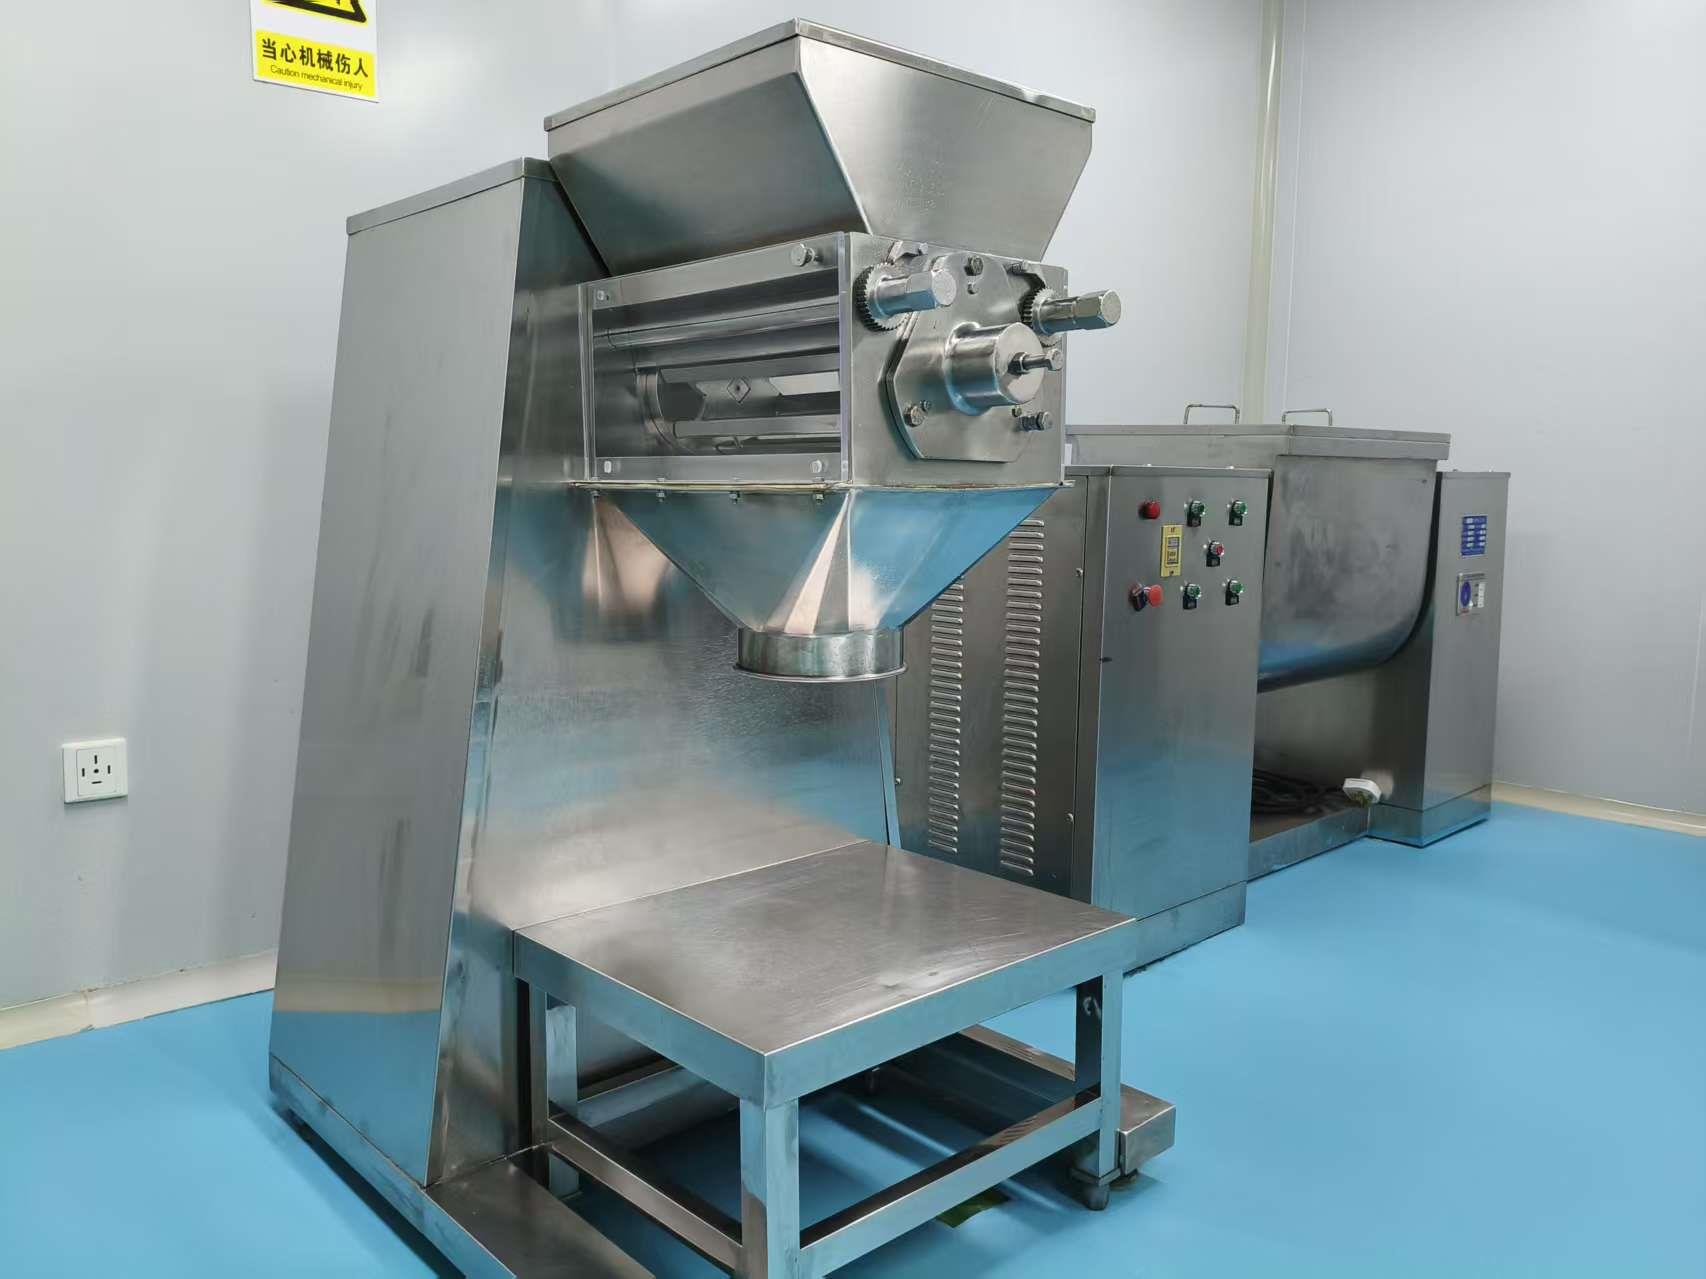
Controlled fluid-bed granulators producing uniform density granules for high-speed pressing.
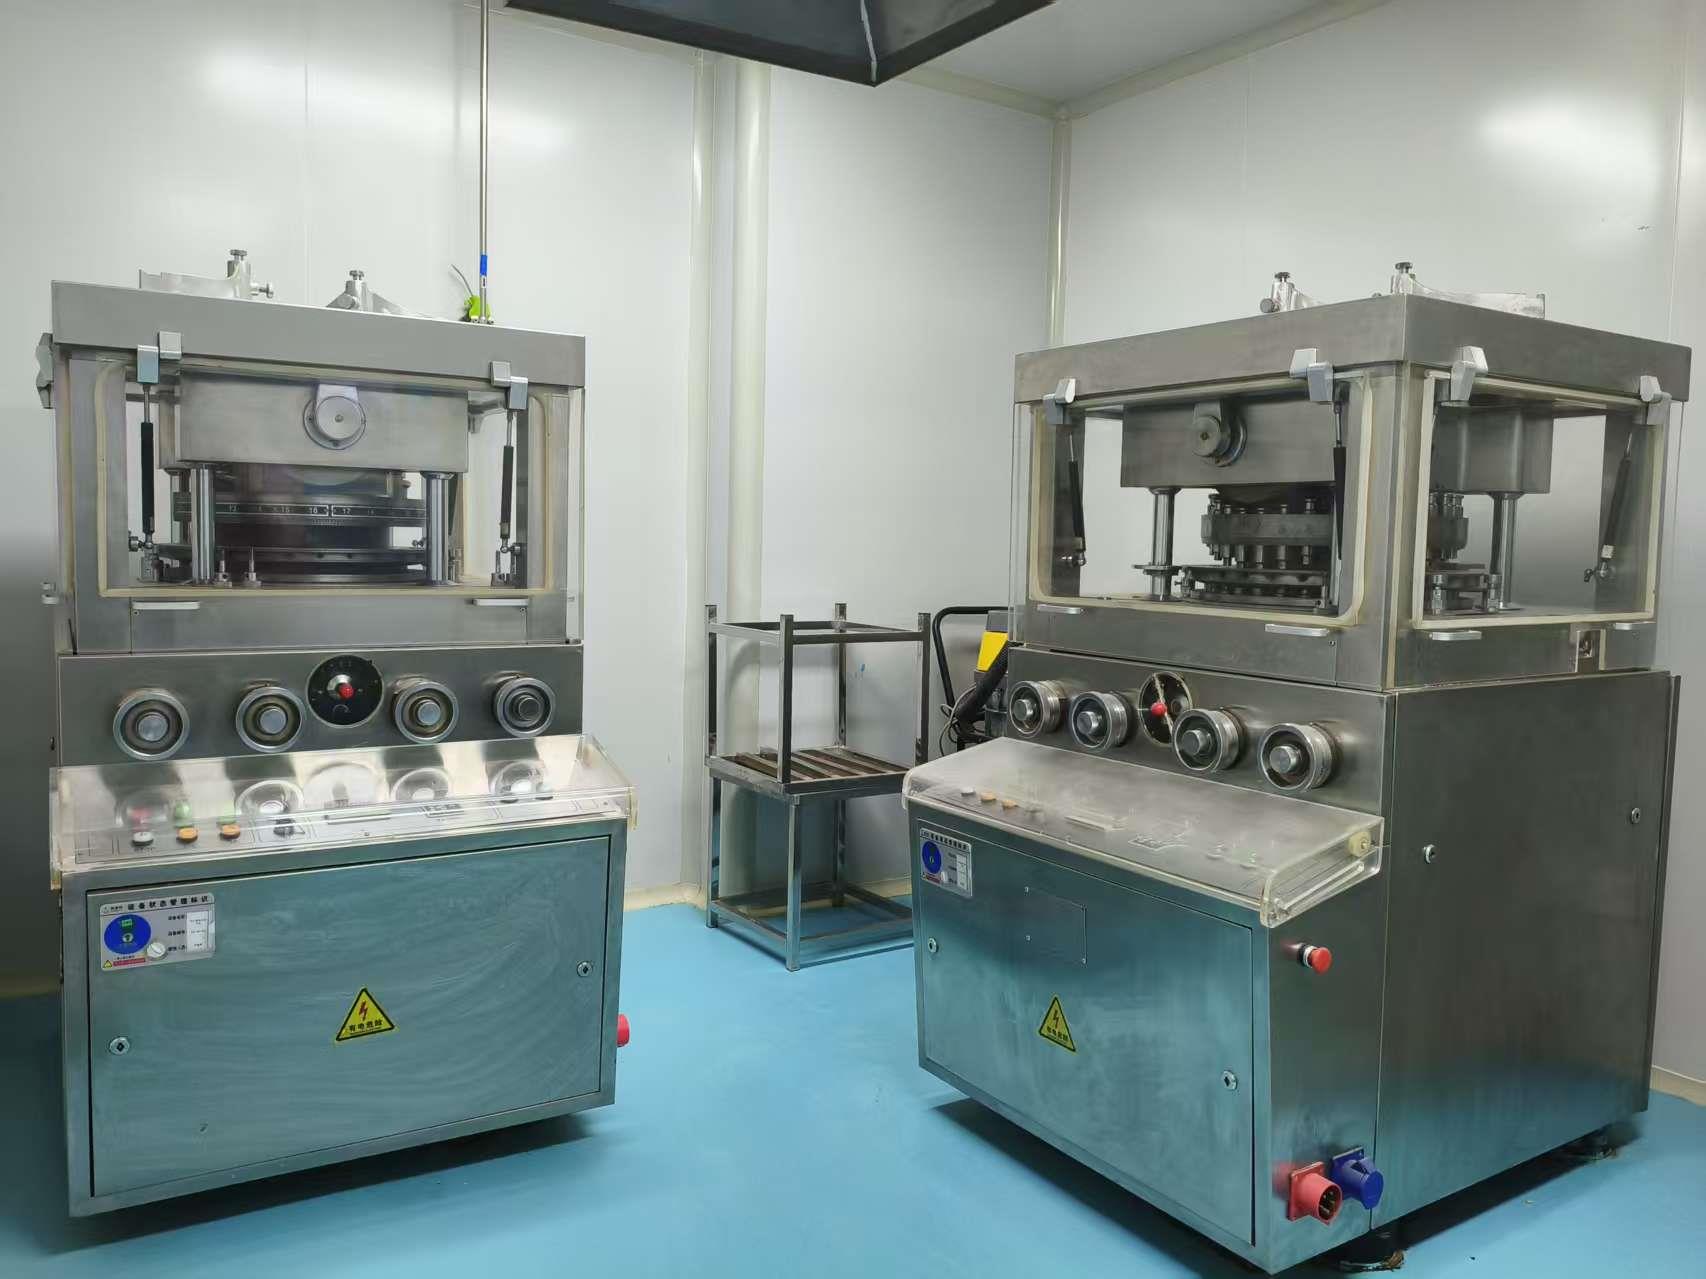
High-speed rotary presses capable of producing round, oval, and custom embossed tablets.
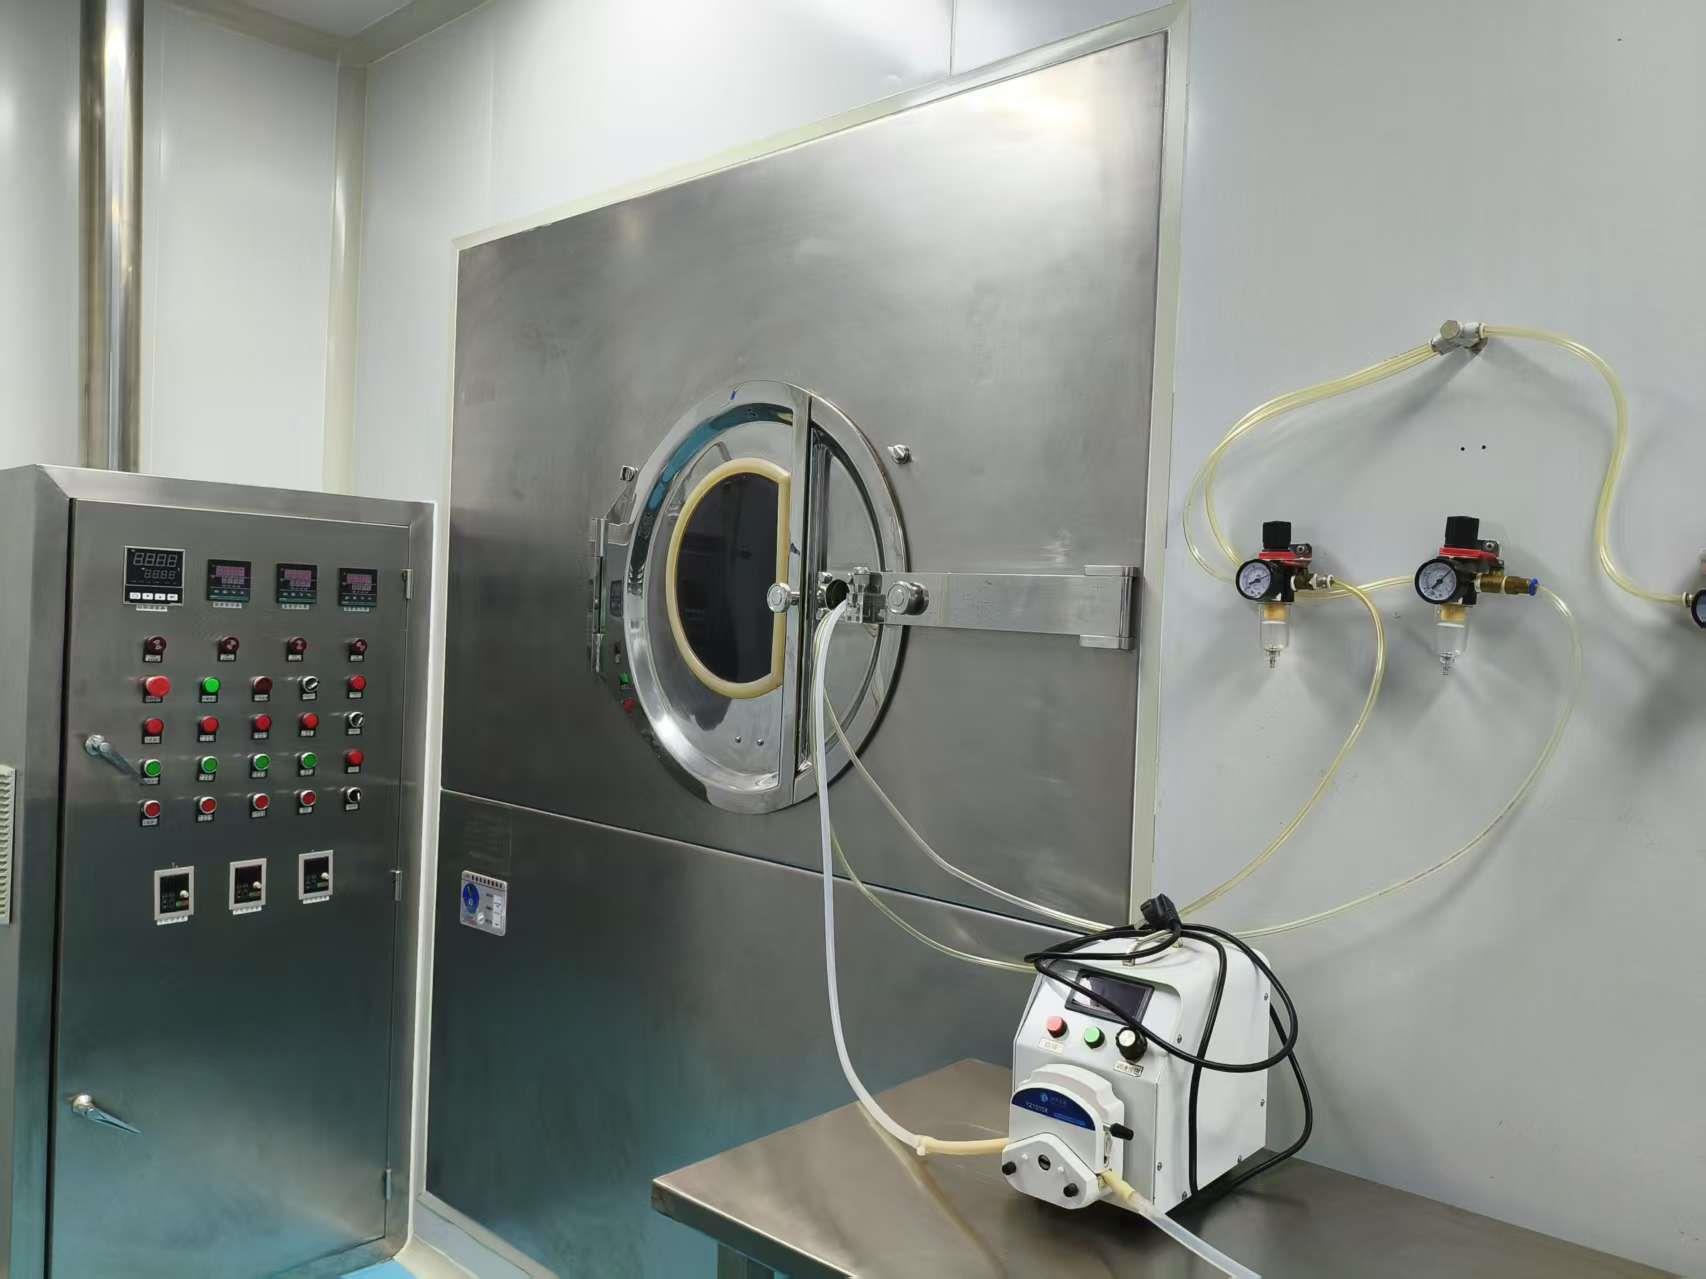
Perforated drum coaters engineered for precise aqueous film, sugar, and enteric barrier coatings.
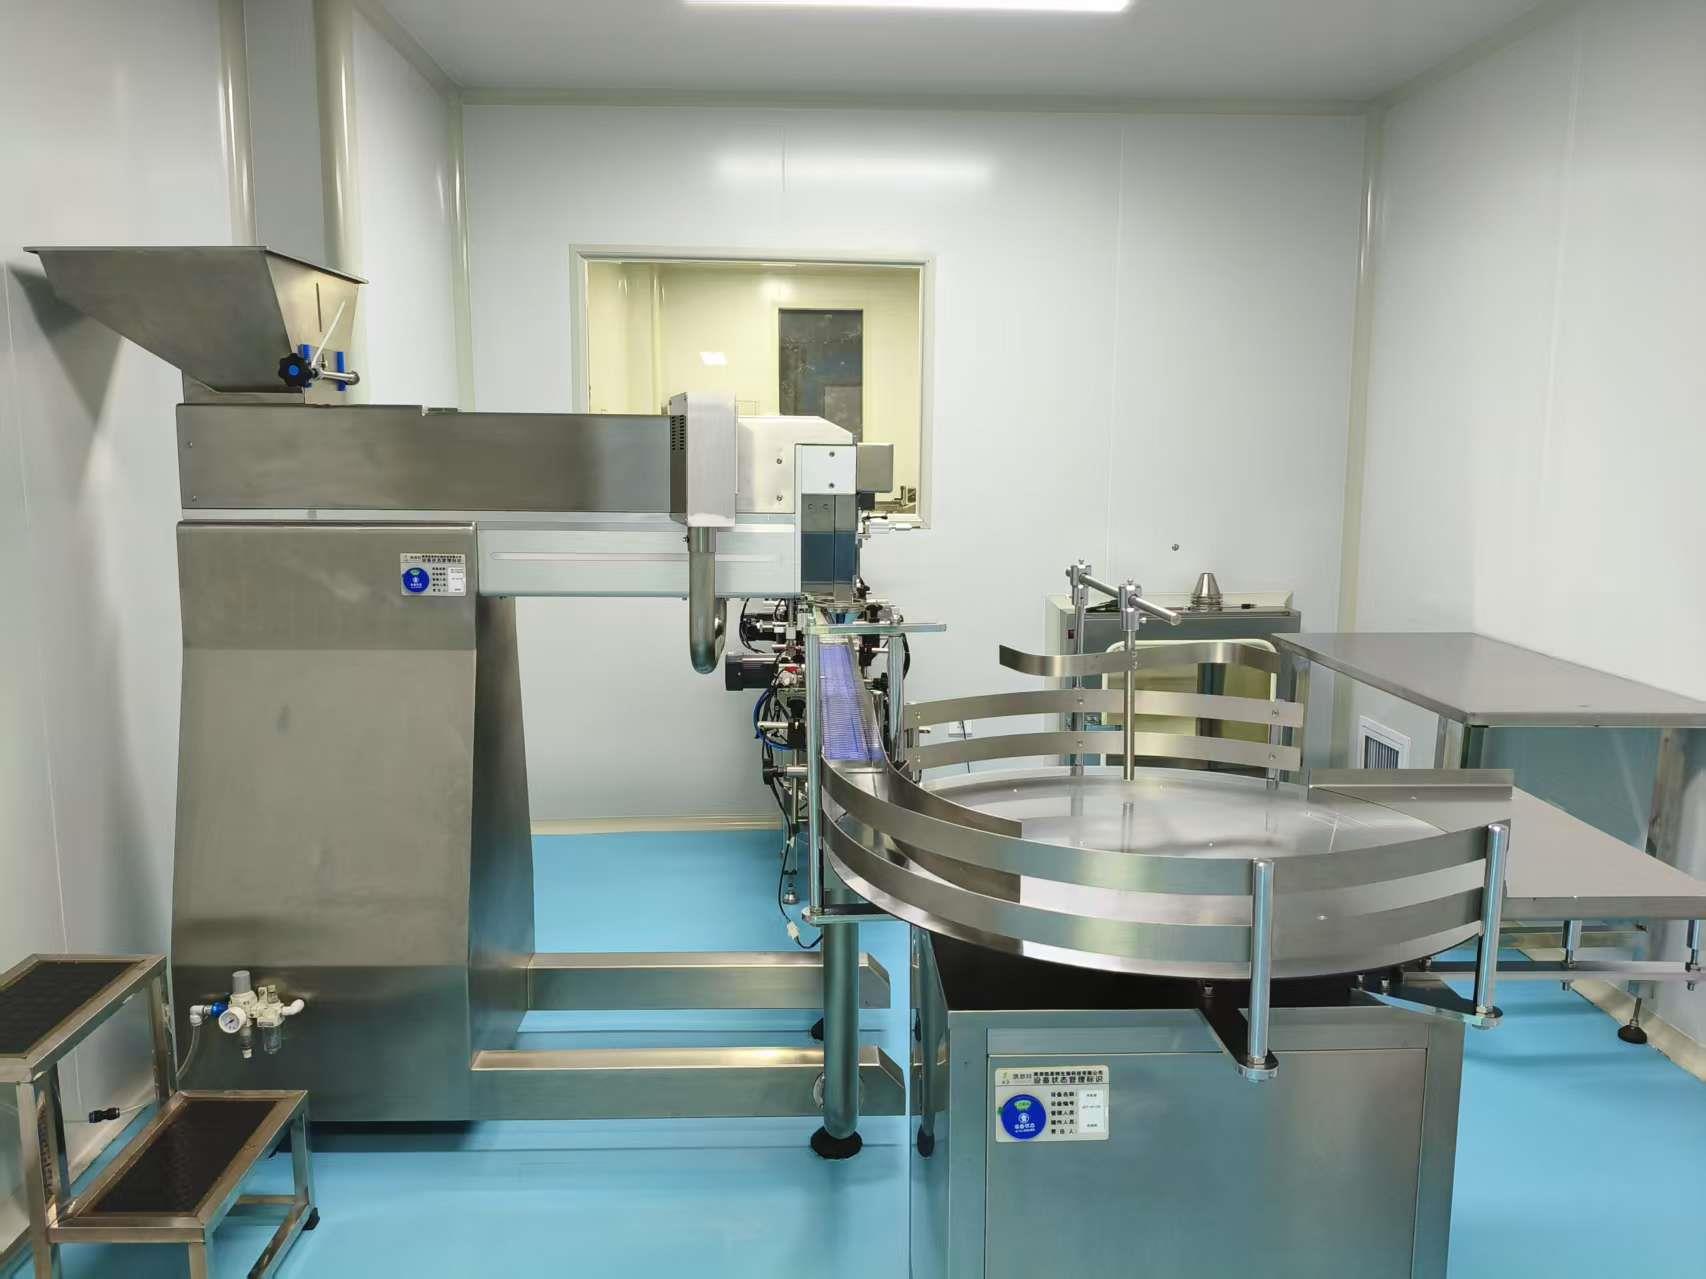
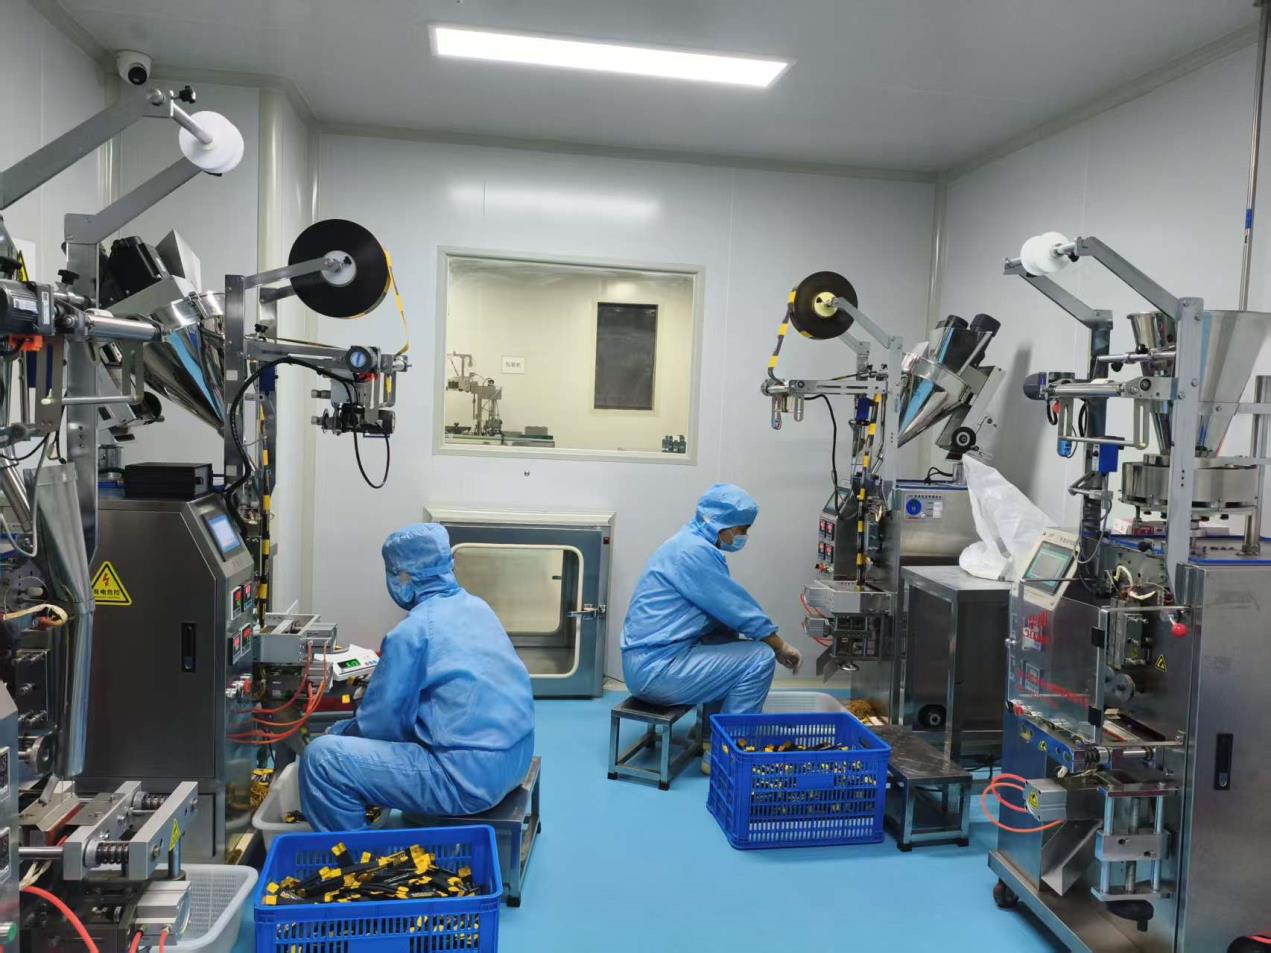
Multi-lane powder packaging machines for stick packs, tear-notch sachets, and pouches.
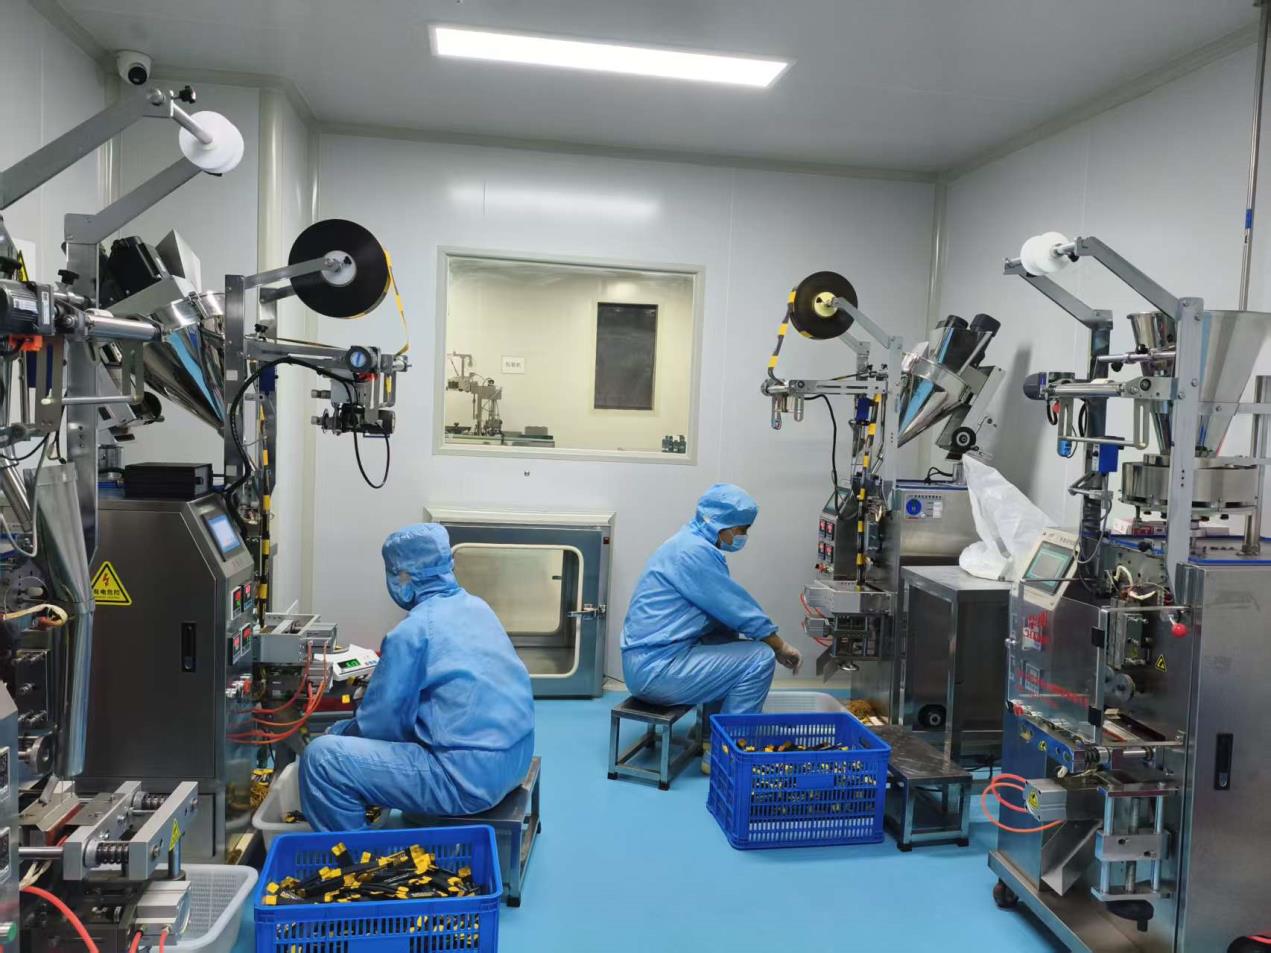
Integrated bottling lines with desiccant insertion, counting, induction sealing, and capping.
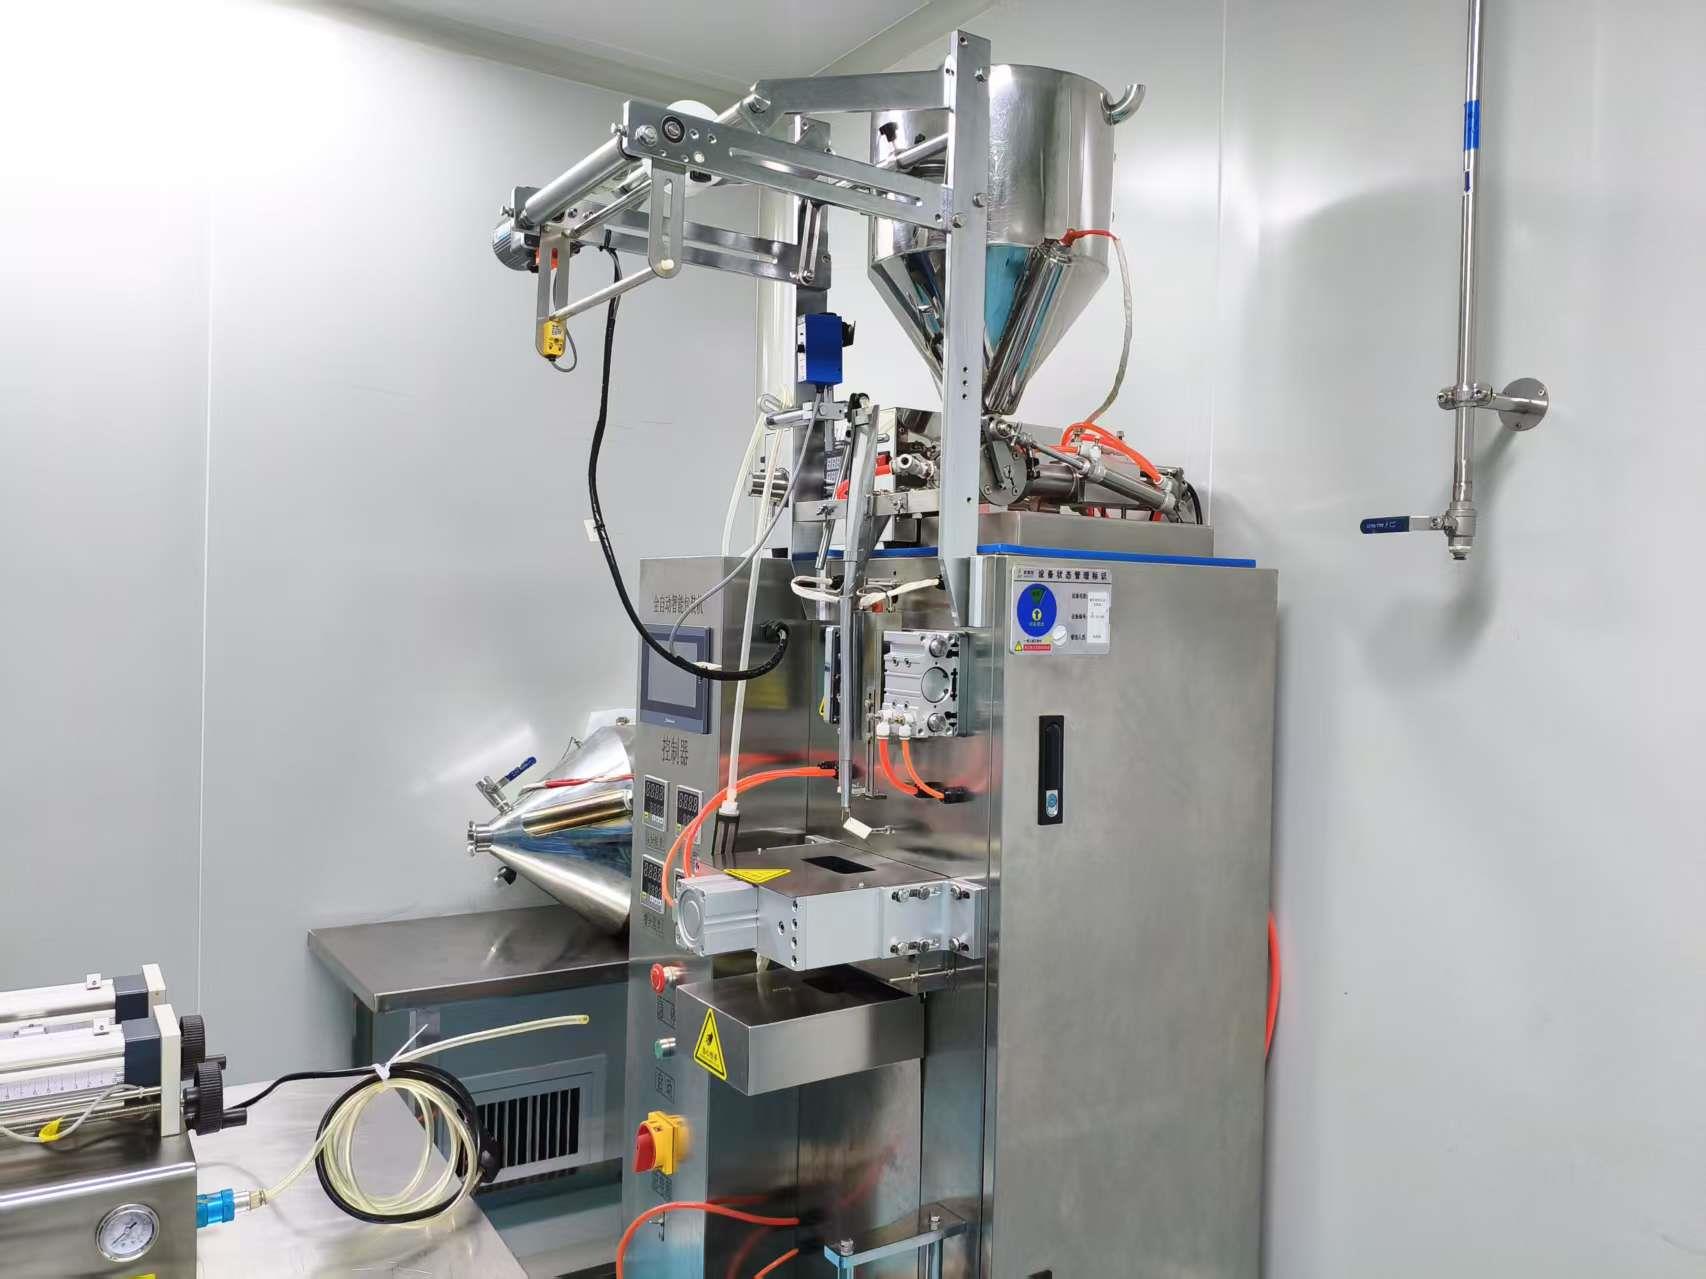
Volumetric and auger fillers ensuring minimal weight variance across capsule and bottle formats.
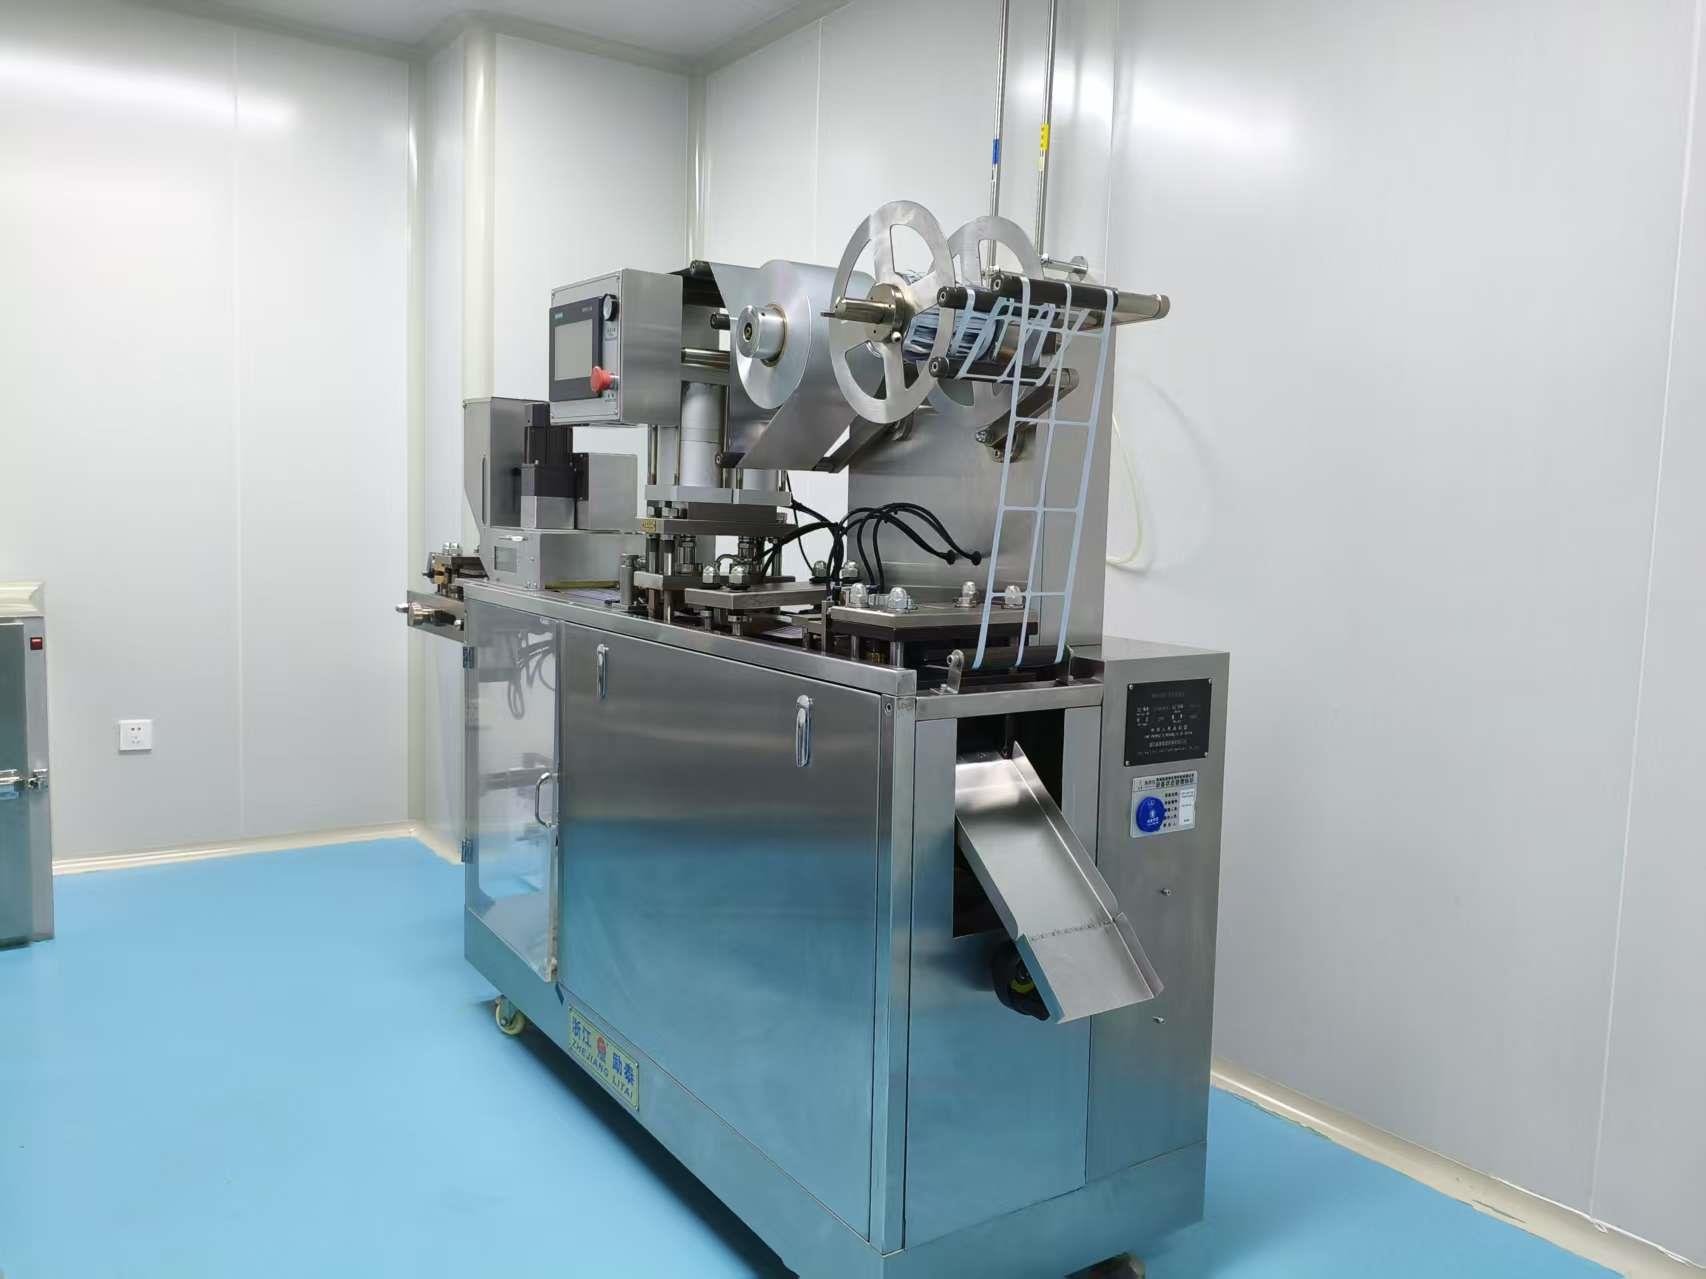
Alu-PVC and Alu-Alu thermoforming blister machines delivering hermetic moisture barriers.
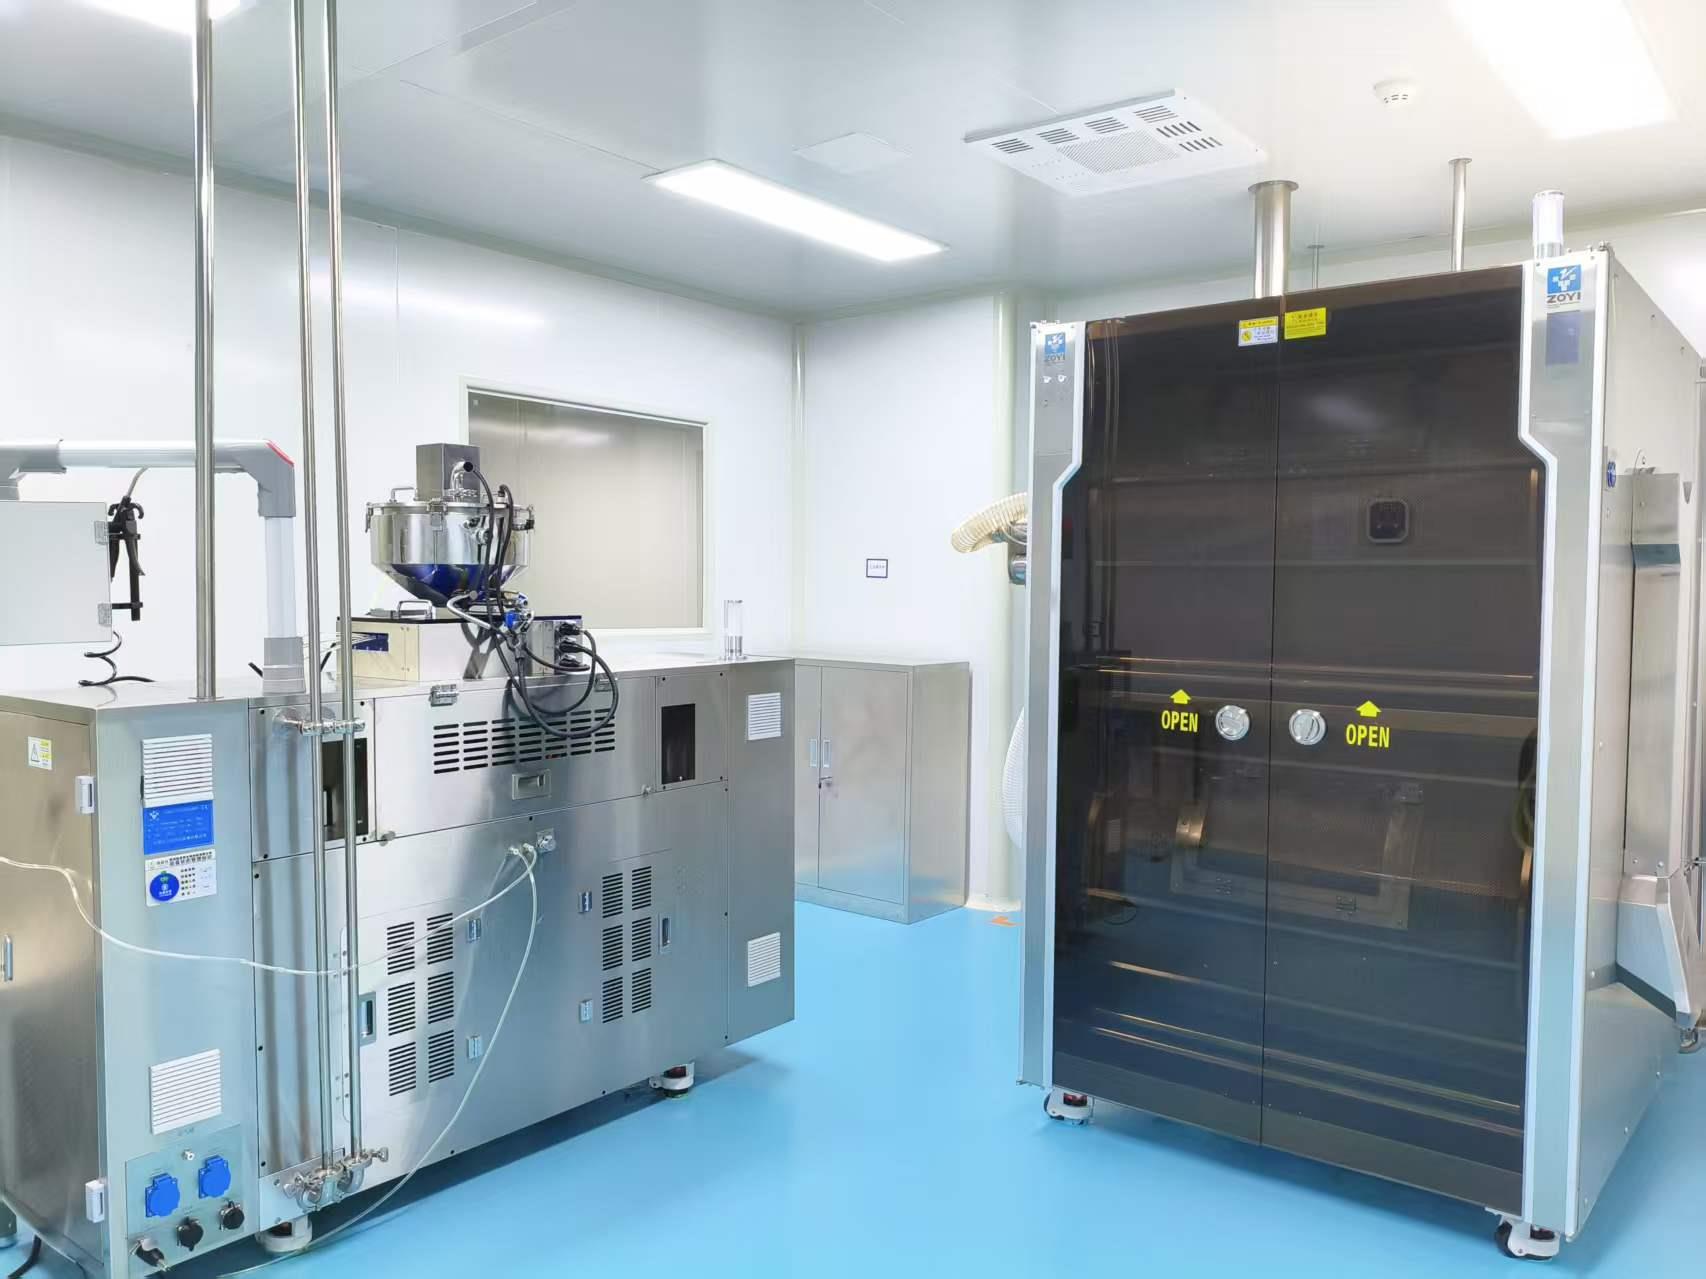
Specialized hydraulic forming equipment for dense herbal resins, drops, and sphere formats.
Our dedicated quality assurance laboratory tests raw materials, intermediate blends, and final packaged goods to certify physical specifications and microbiological safety.
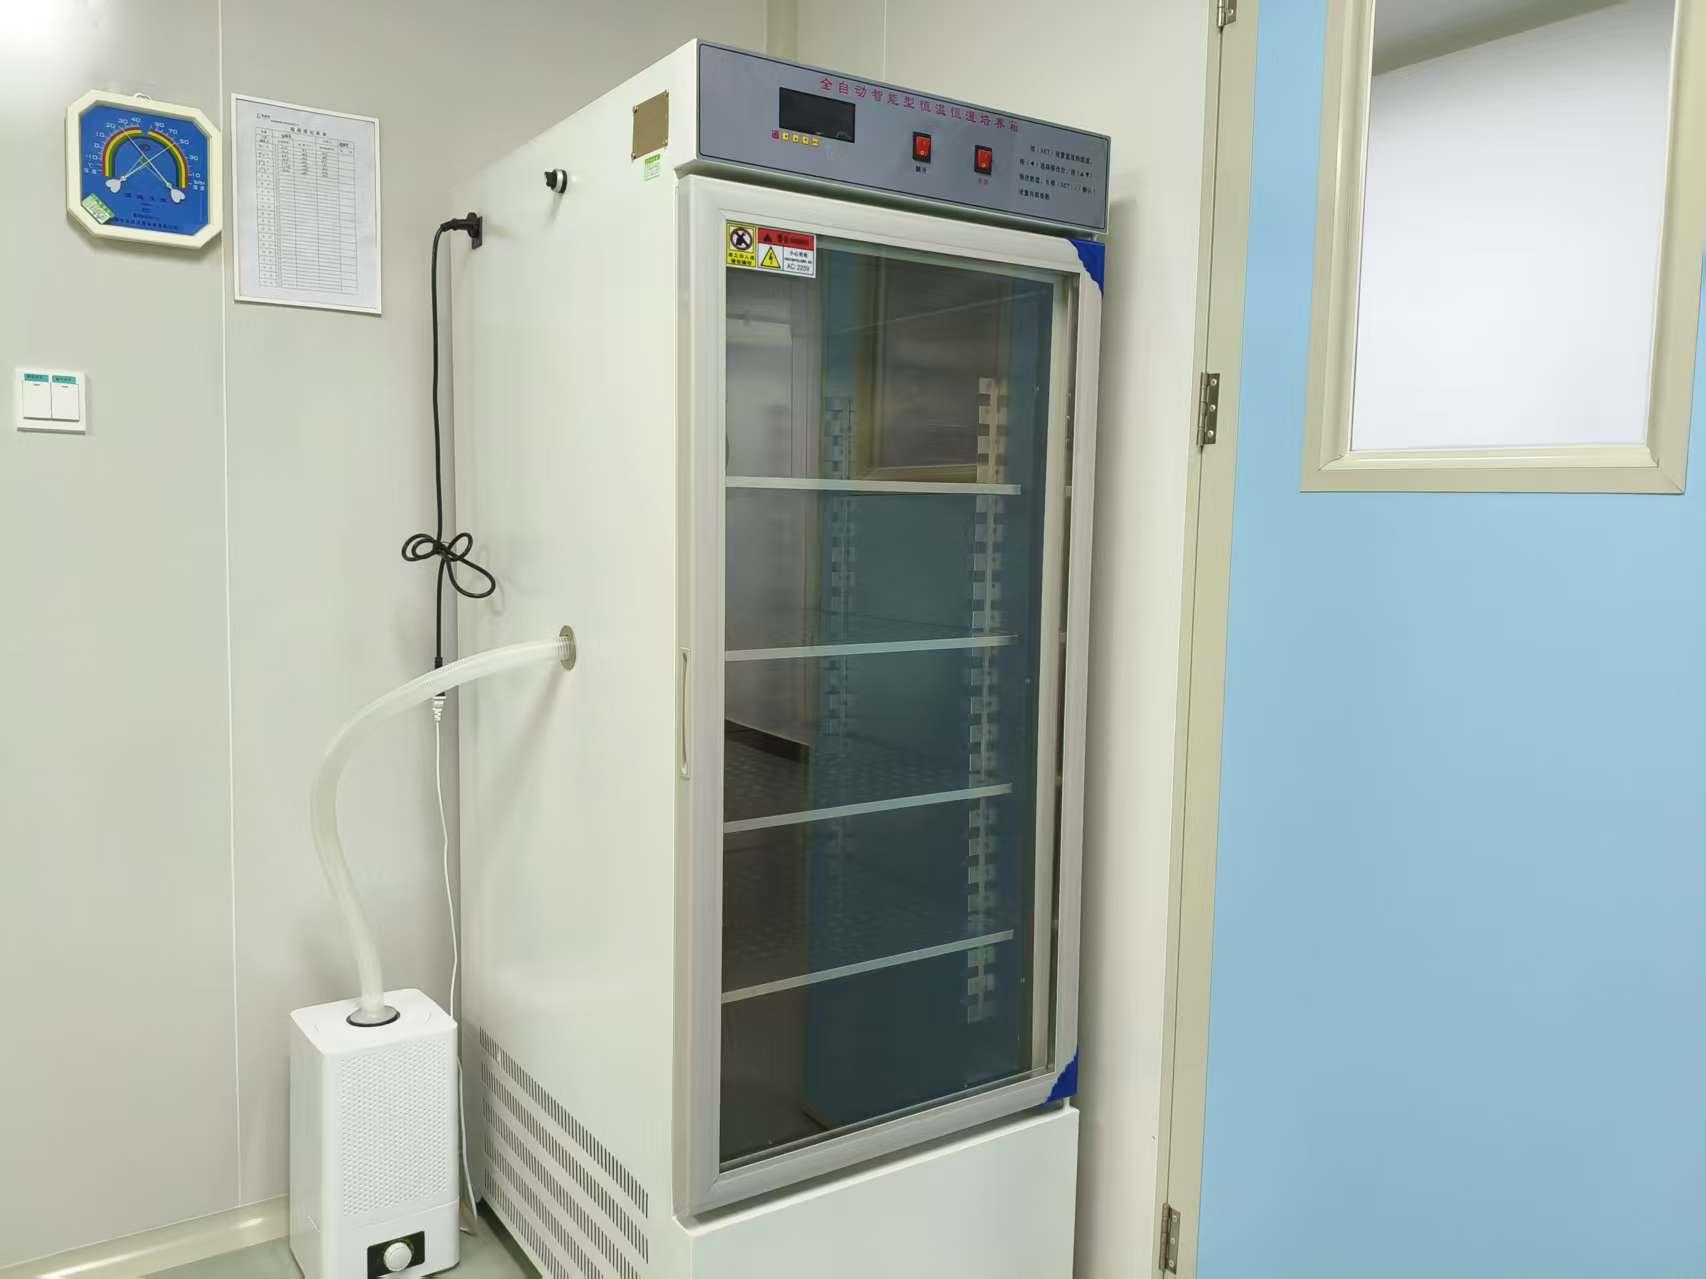
Precision temperature incubation for total plate count, yeast, mold, E. coli, and Salmonella bioburden assays.
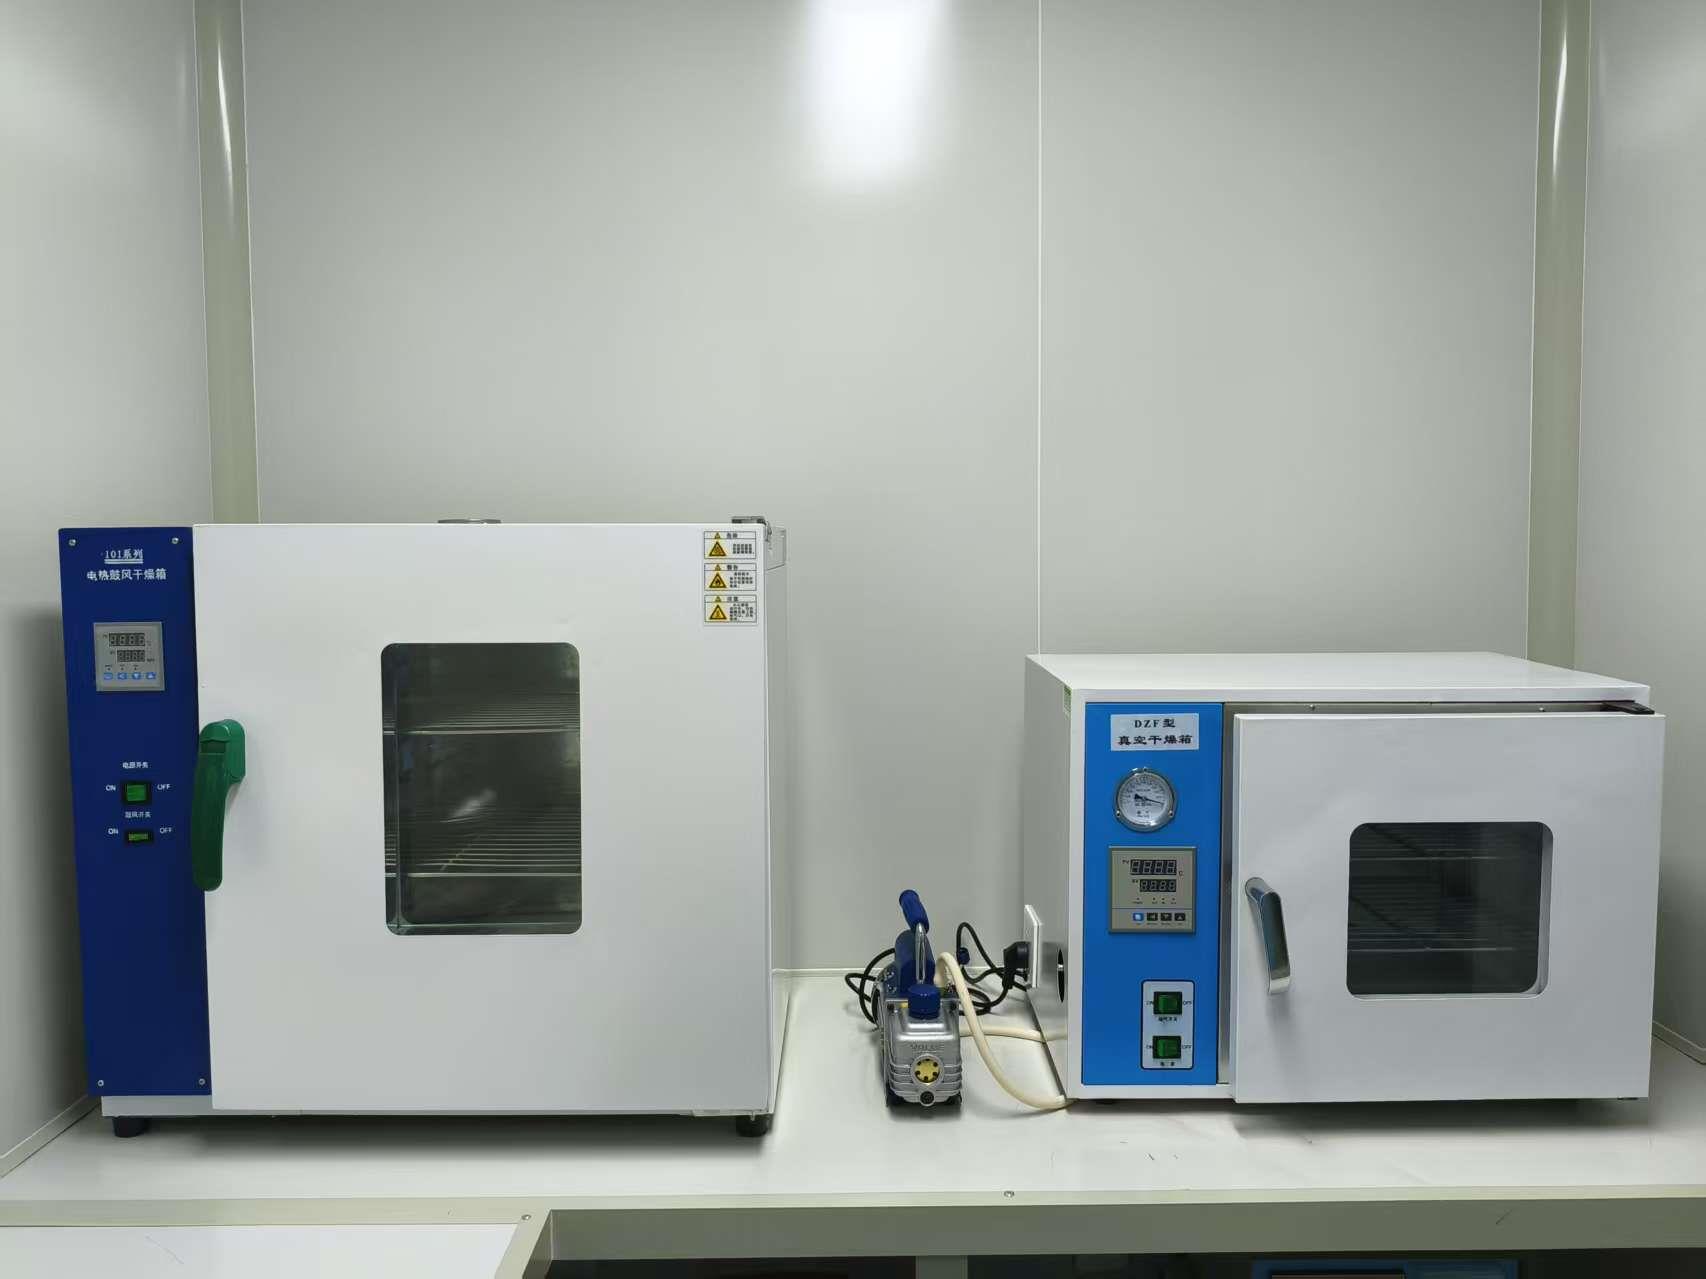
Thermal ovens utilized for loss-on-drying (LOD) and moisture determination to ensure product shelf life and stability.
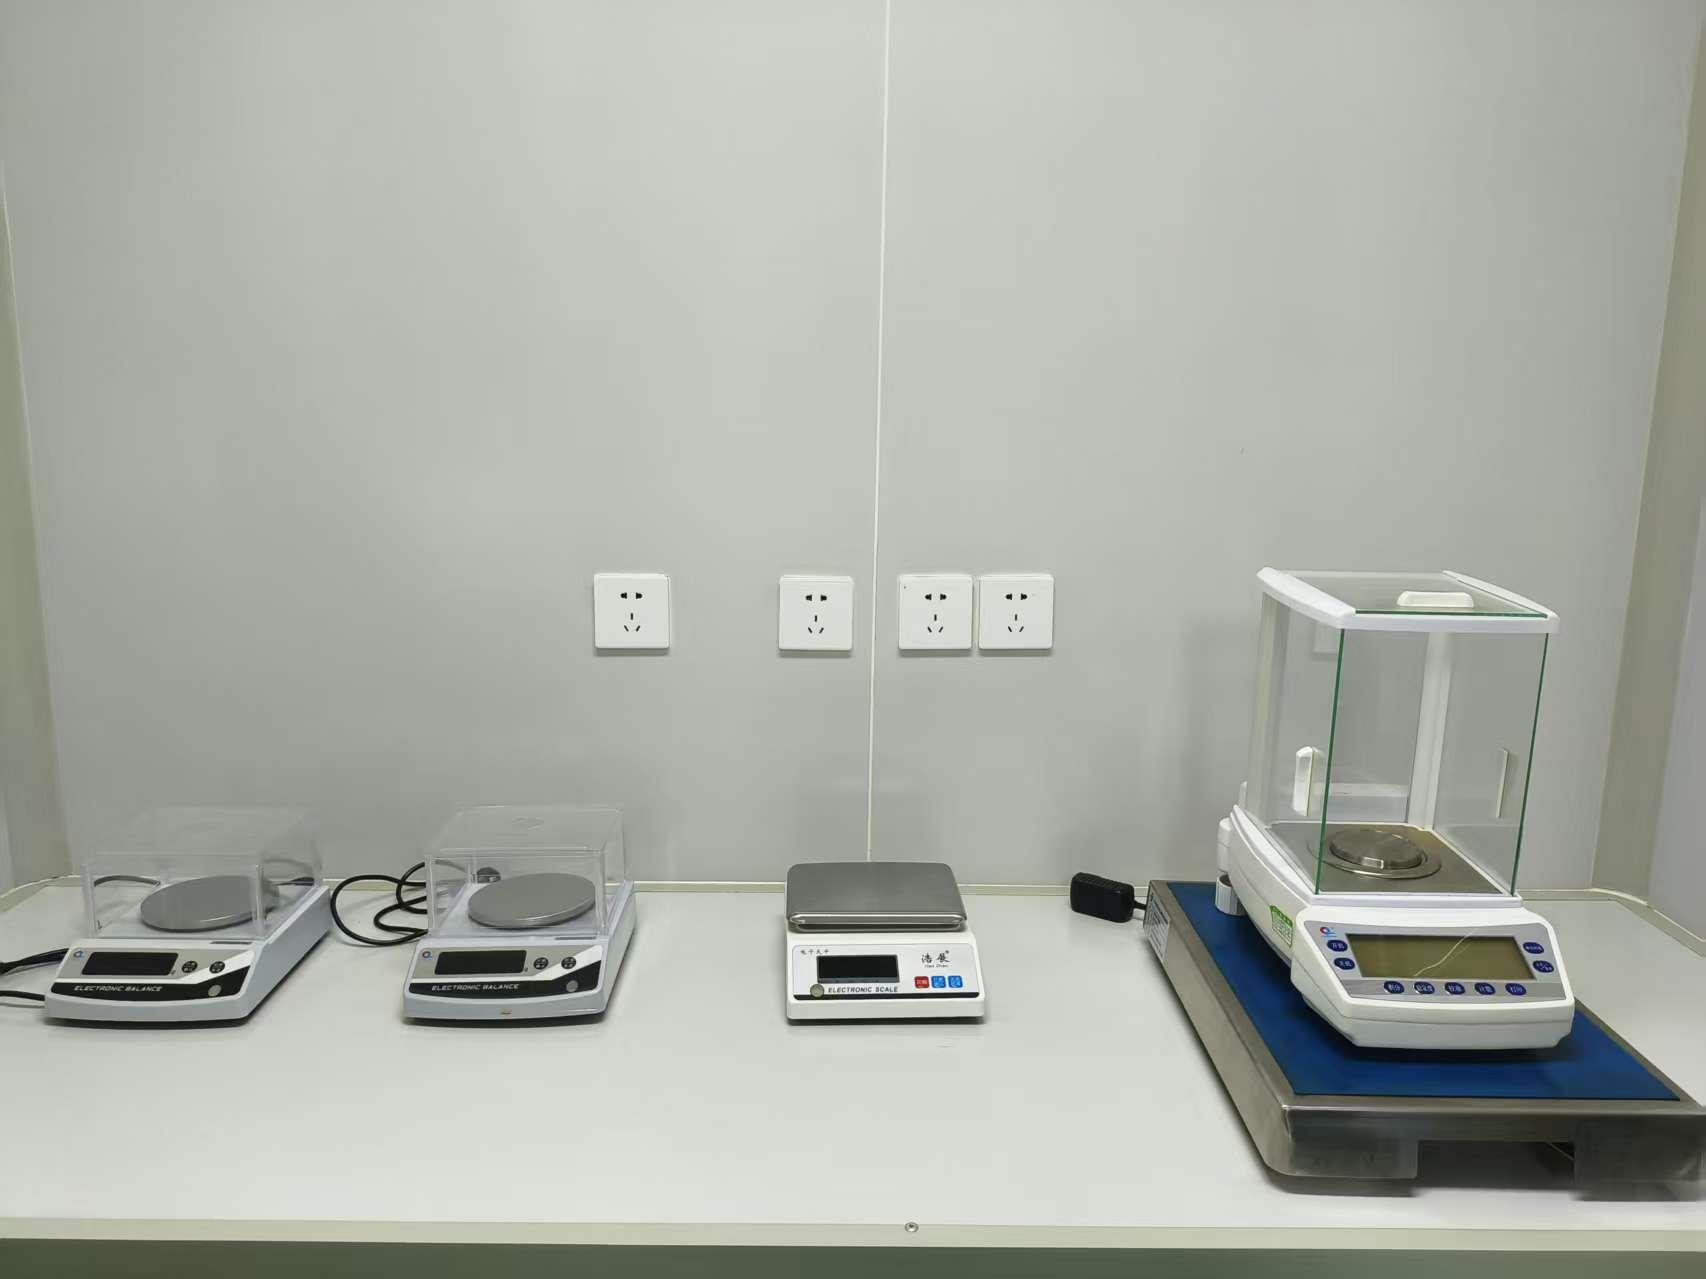
Multi-calibrated analytical balances delivering micro-gram sensitivity for chemical reagents, assays, and weight uniformity.
Our documented quality systems meet the legal entrance requirements for major retail, pharmaceutical, and health distribution channels across the globe.
Good Manufacturing Practice compliance covering dietary supplement production, environmental air handling, and traceability systems.
Systemic food safety management system covering plant extracts, functional tablets, powders, and private label health formulas.
Hazard Analysis and Critical Control Points preventive framework eliminating biological, chemical, and physical foreign matter.
Verified compliance with NOP (National Organic Program) and European Union organic regulations for botanical ingredients.
Full auditing of raw materials, cleanroom cleaning regimens, and excipients in compliance with strict Islamic dietary standards.
Inspection verified adherence to kosher dietary law, ensuring clean equipment, unadulterated ingredients, and kosher-grade production.