STEP 01 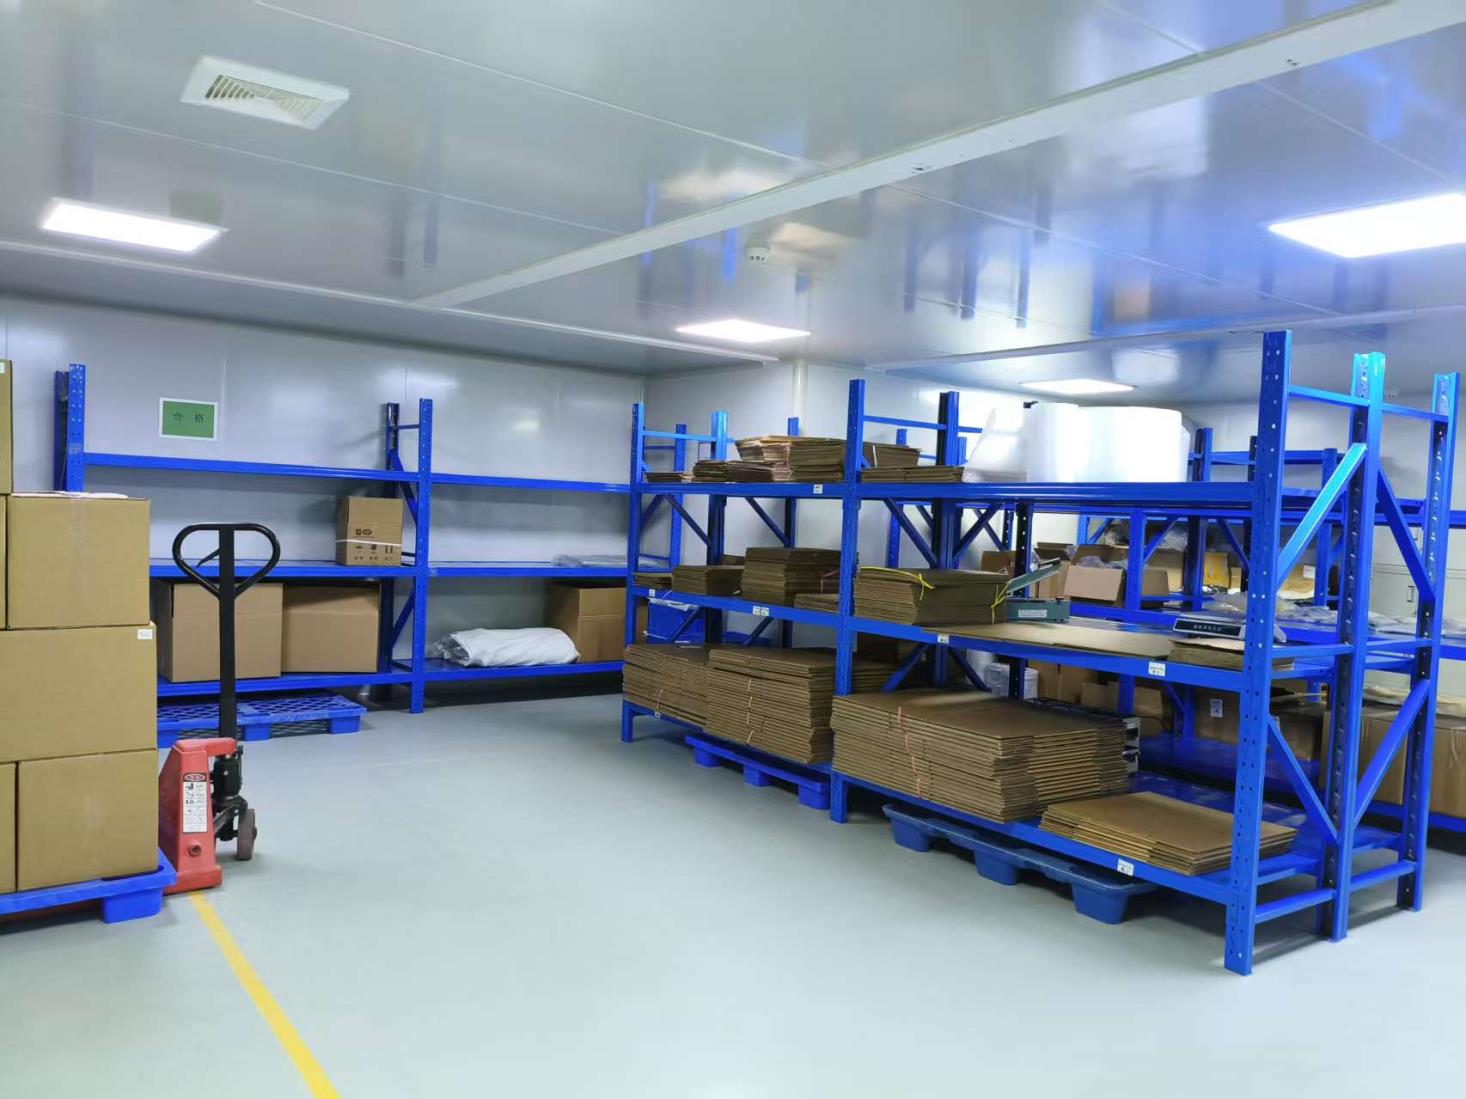
Raw Material
All active botanical powders, vitamins, and minerals undergo quarantine, sensory appraisal, and laboratory identity testing before entering batch dispensing.
Shaanxi ESNO Biotech Co., Ltd. is a high-tech nutraceutical enterprise founded in 2006, located in the High-Tech Industrial Development Zone of Xi'an, Shaanxi, China. We specialize in custom contract manufacturing (OEM/ODM) of dietary supplements, botanical extracts, functional nutritional formulations, tablets, capsules, and powder sachets for brand owners across North America, Europe, Oceania, and Southeast Asia.
Our operations have undergone rigorous on-site qualification and auditing by independent third-party inspection authorities, including TÜV Rheinland. With strict adherence to international GMP standards, we maintain full chain-of-custody traceability from identity-authenticated botanical raw materials to final packaging.
Every batch produced at Shaanxi ESNO Biotech Co., Ltd. follows standardized, auditable procedural steps to ensure potency, purity, and formulation consistency.
All active botanical powders, vitamins, and minerals undergo quarantine, sensory appraisal, and laboratory identity testing before entering batch dispensing.
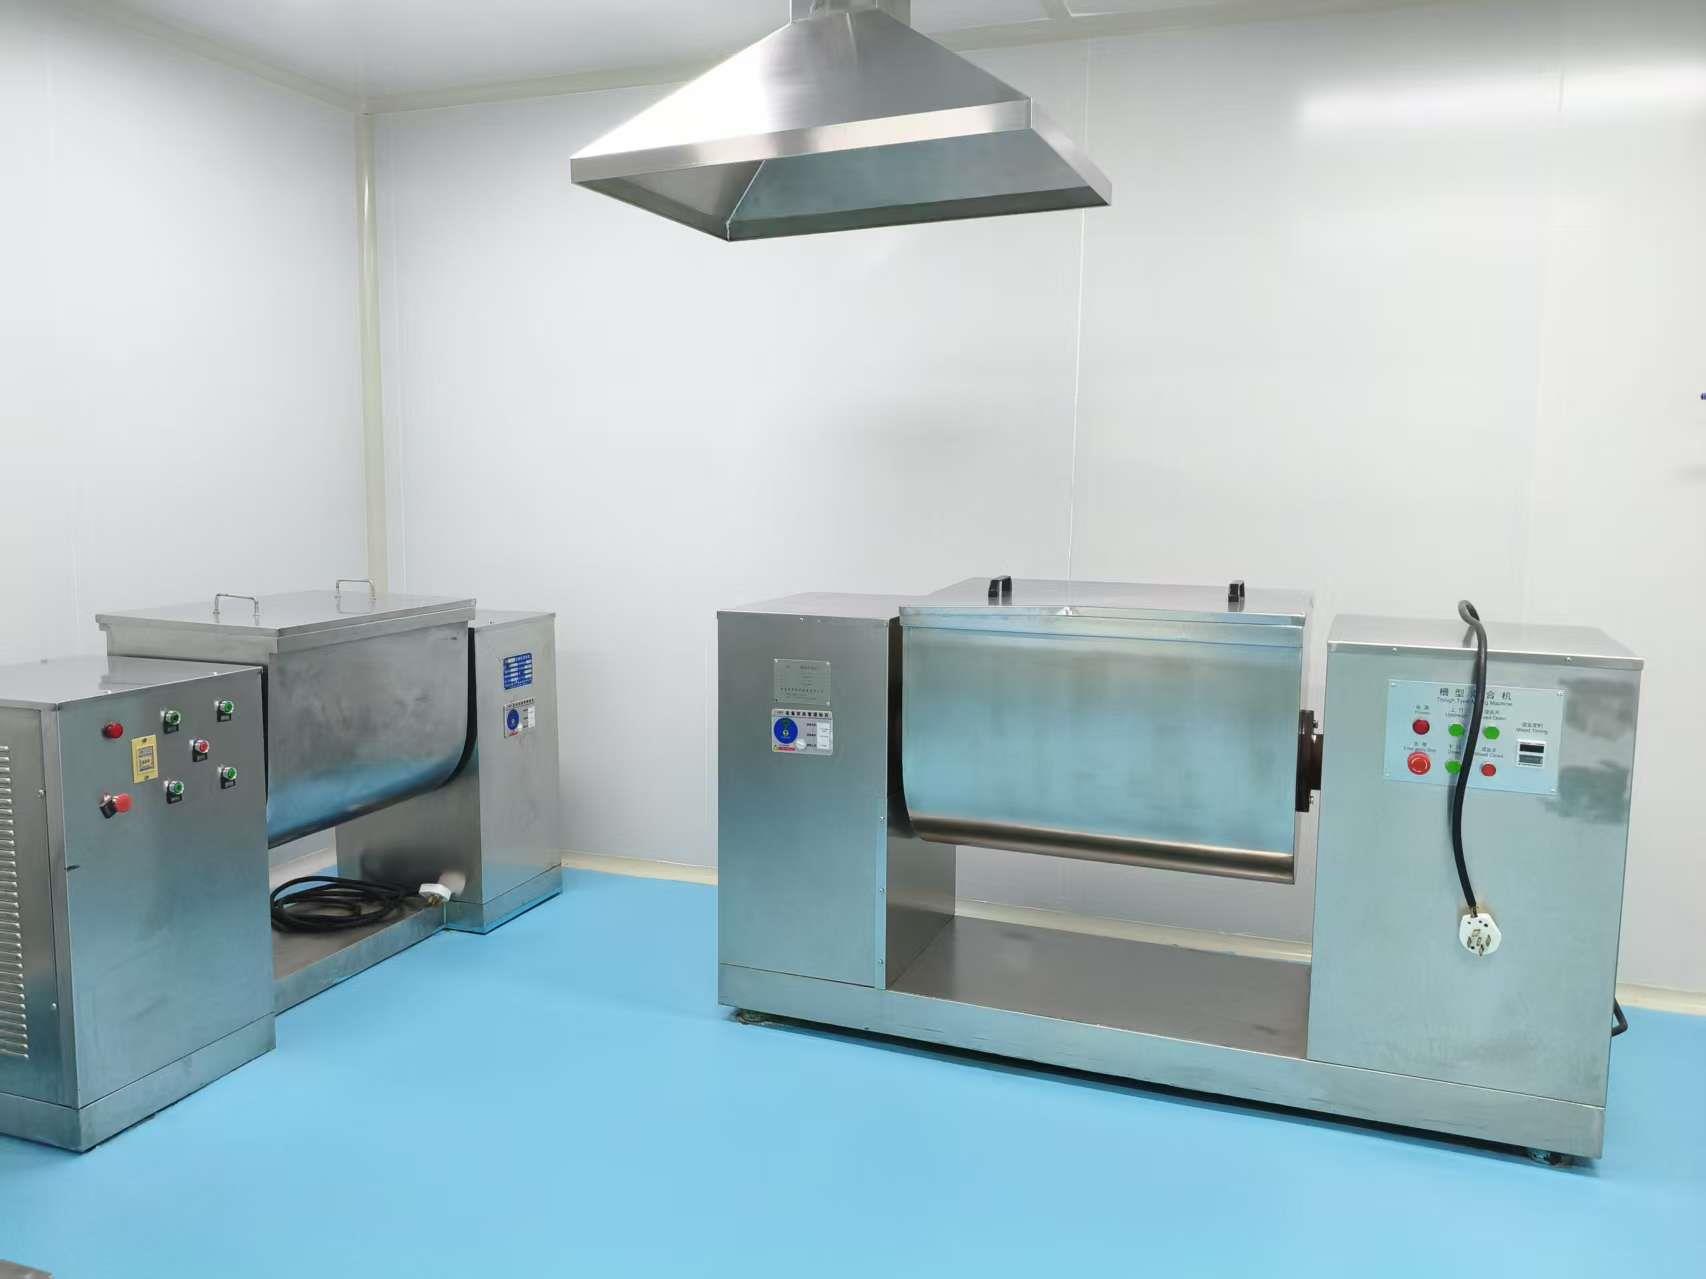
High-efficiency industrial mixers homogenize active botanical extracts and excipients to achieve uniform dispersion across large volume batches.
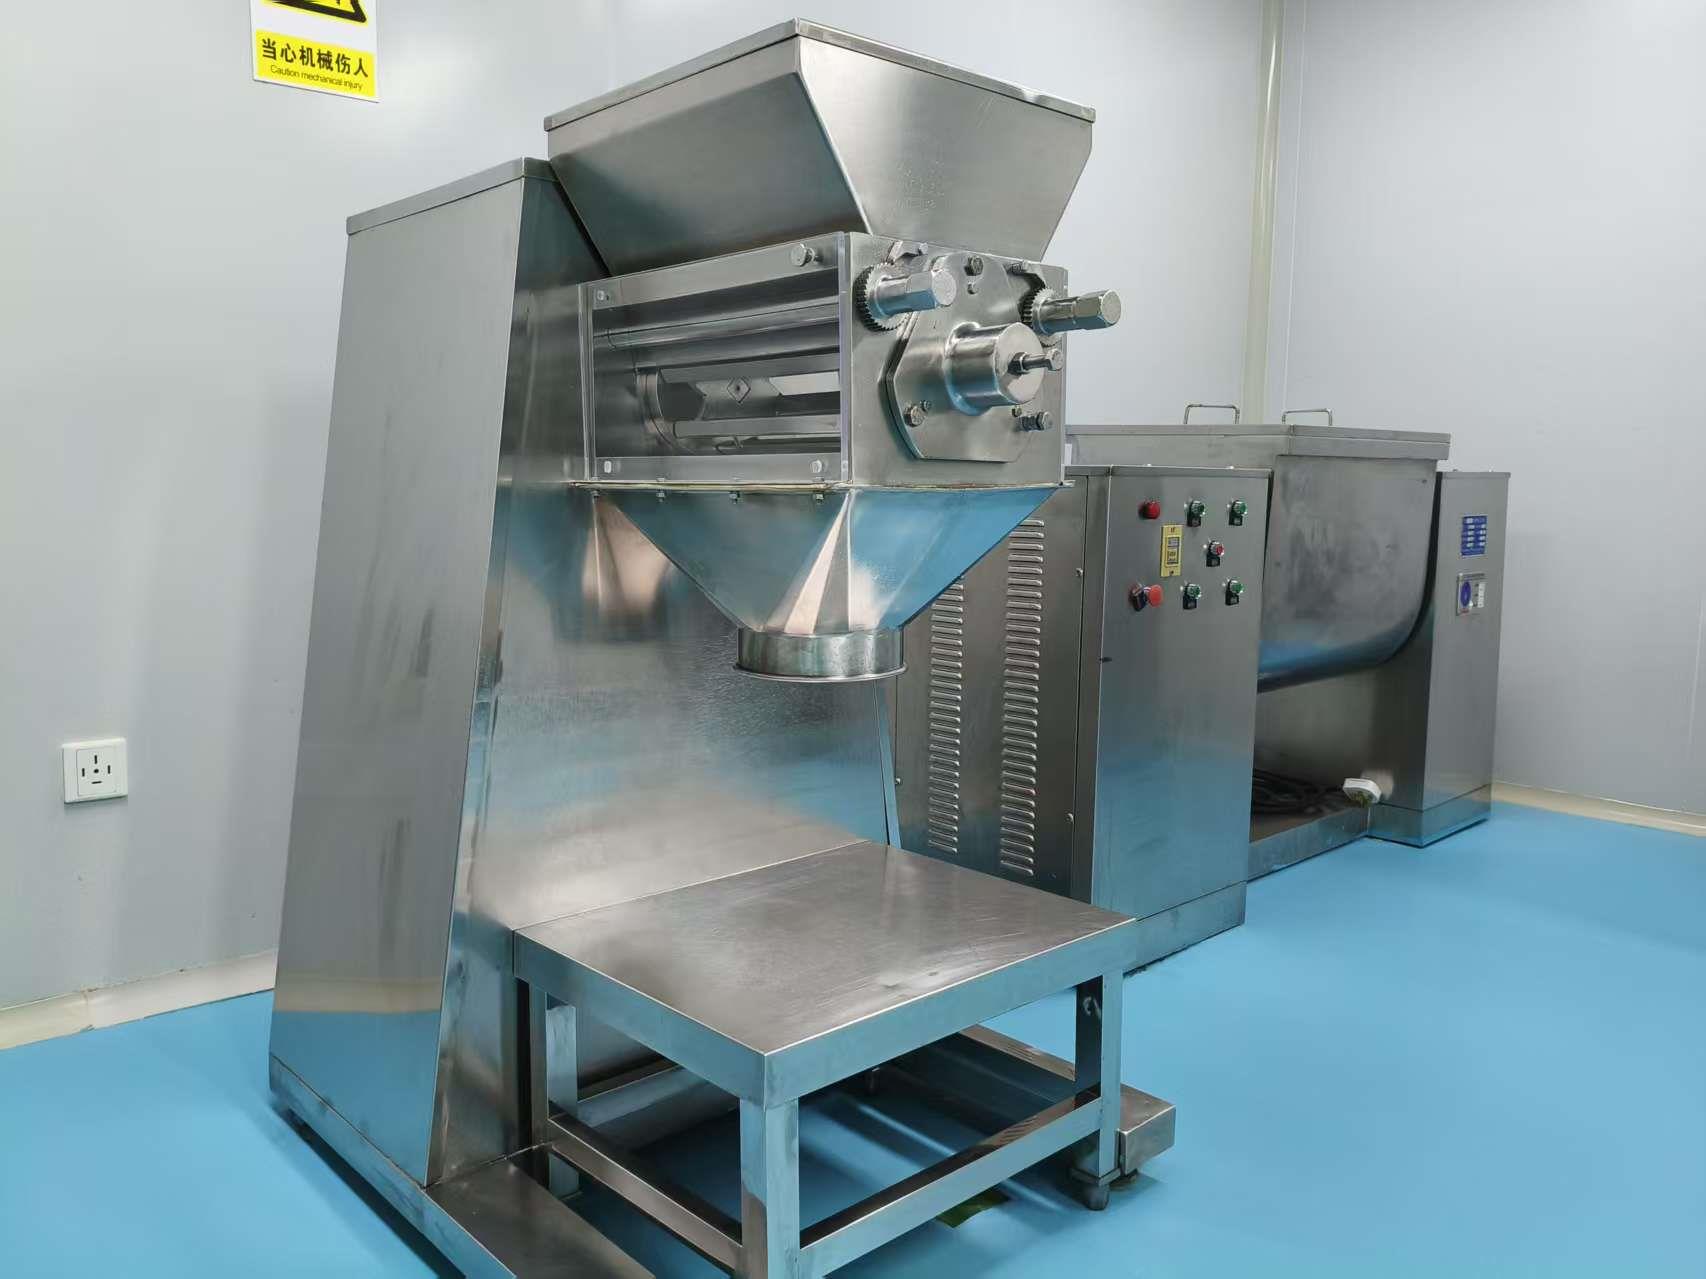
Precision granulation converts fine powders into free-flowing, high-density granules suitable for continuous compression and uniform filling weight.
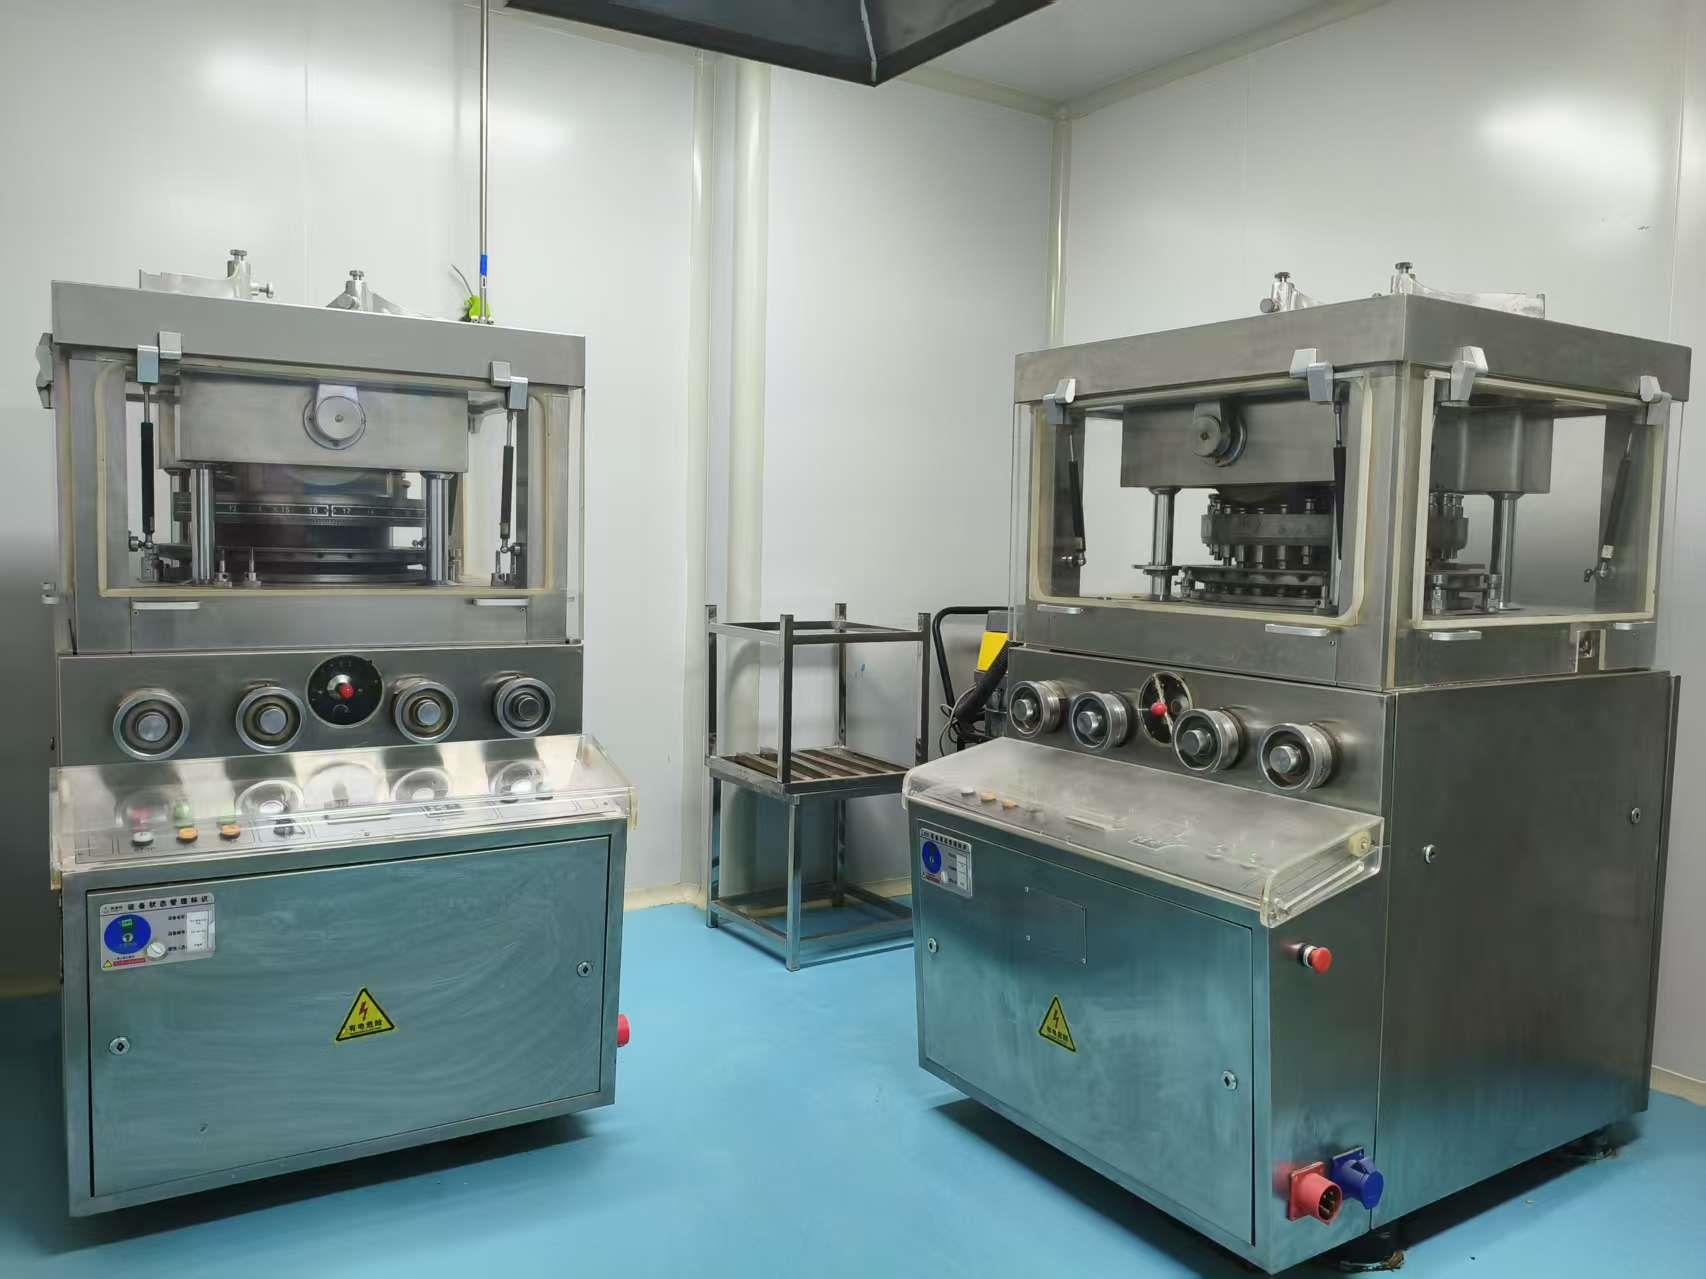
High-speed rotary presses produce uniform round, oval, or embossed tablets with continuous in-line monitoring of hardness, weight variation, and friability.
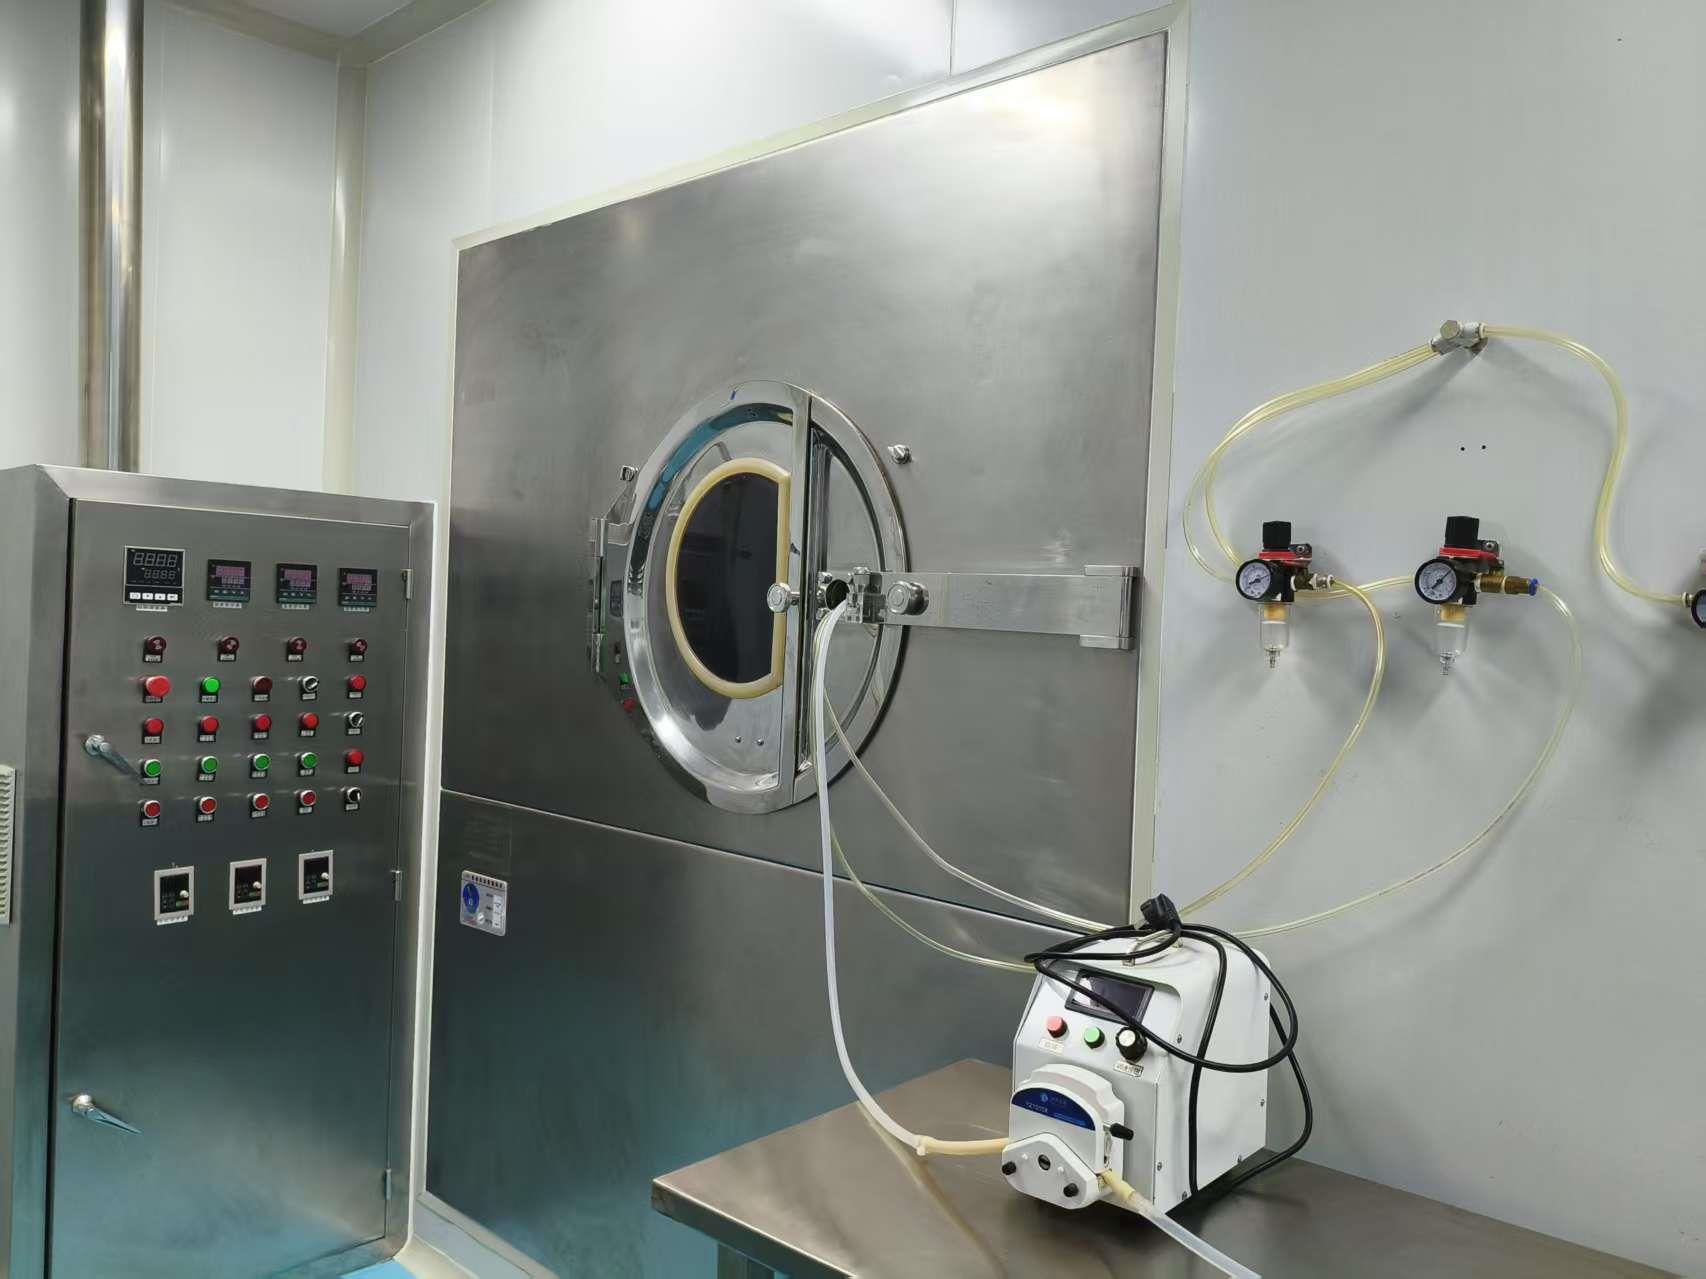
Aqueous film coating provides moisture barriers, masks bitter botanical tastes, enables enteric delivery, and customizes aesthetic brand colors.
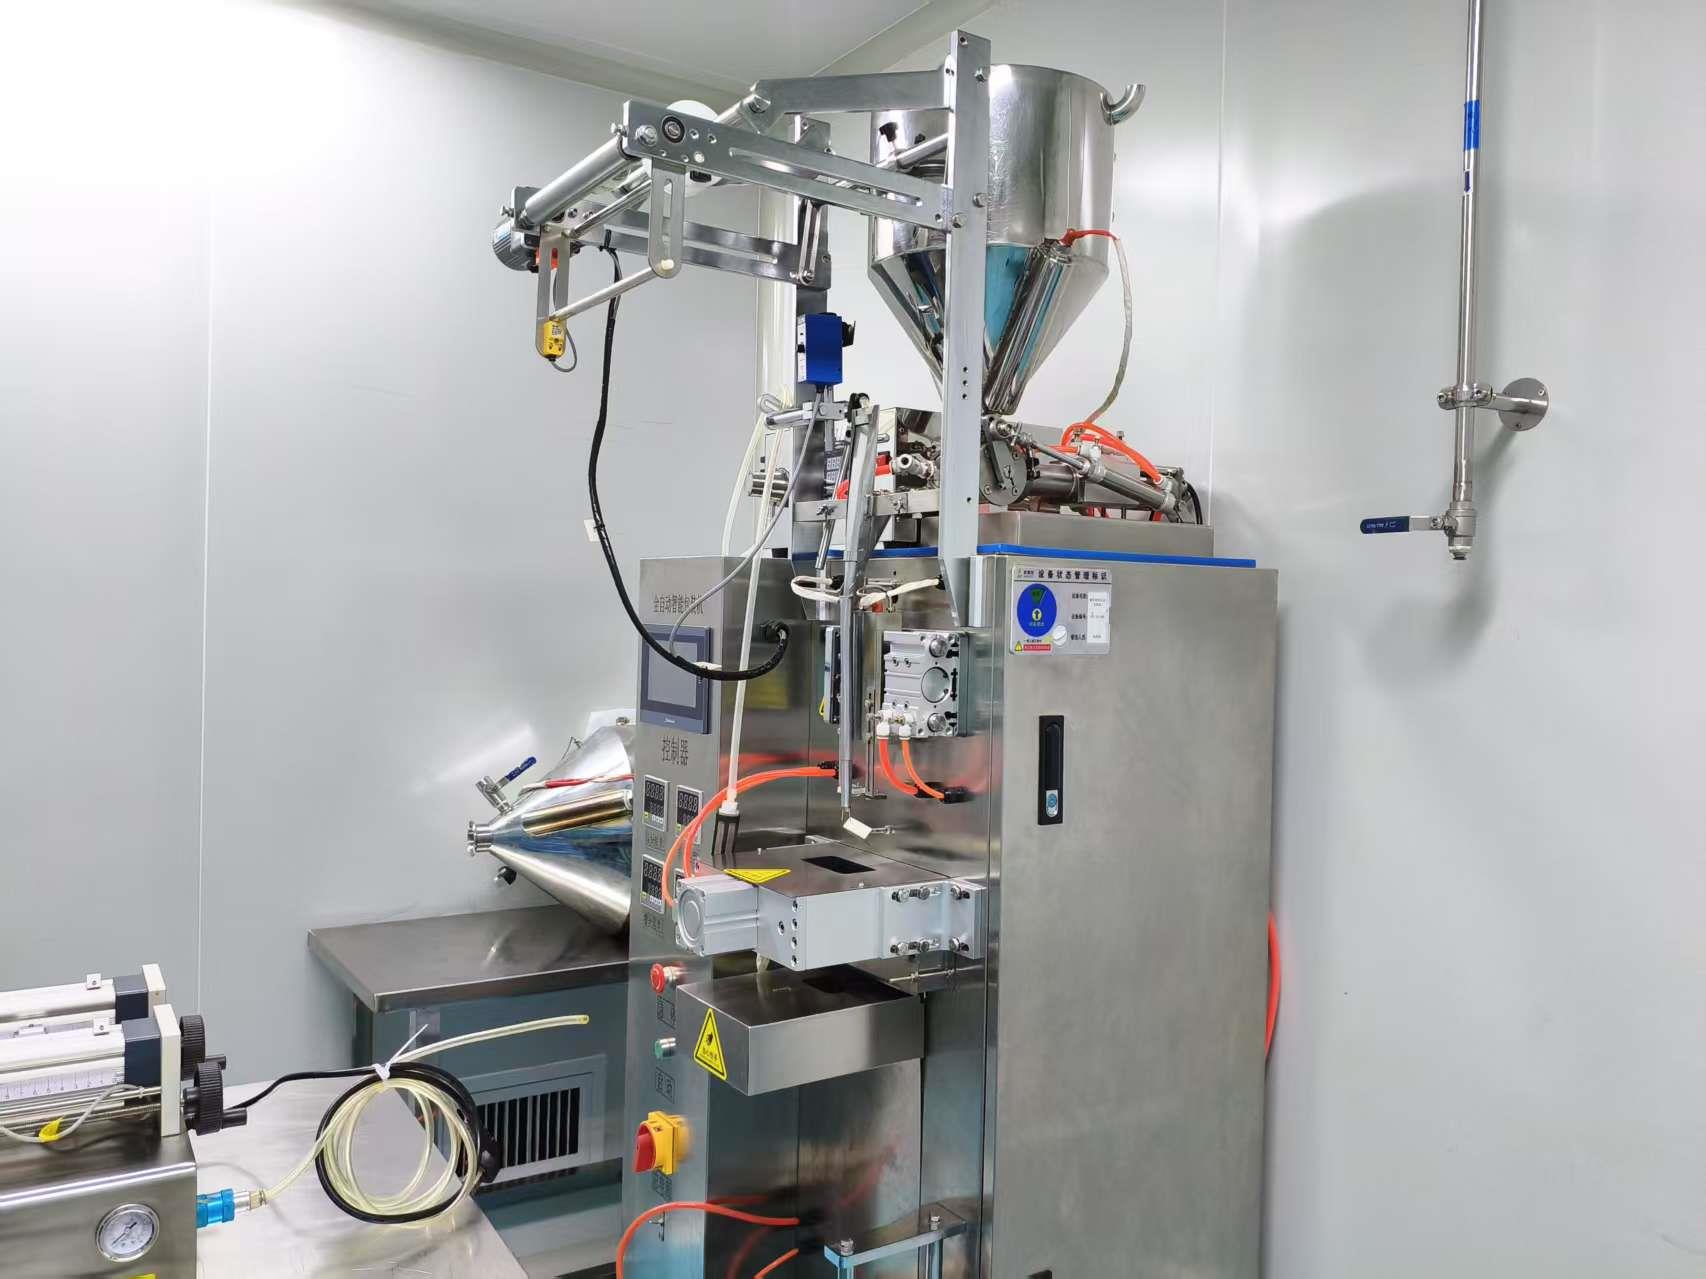
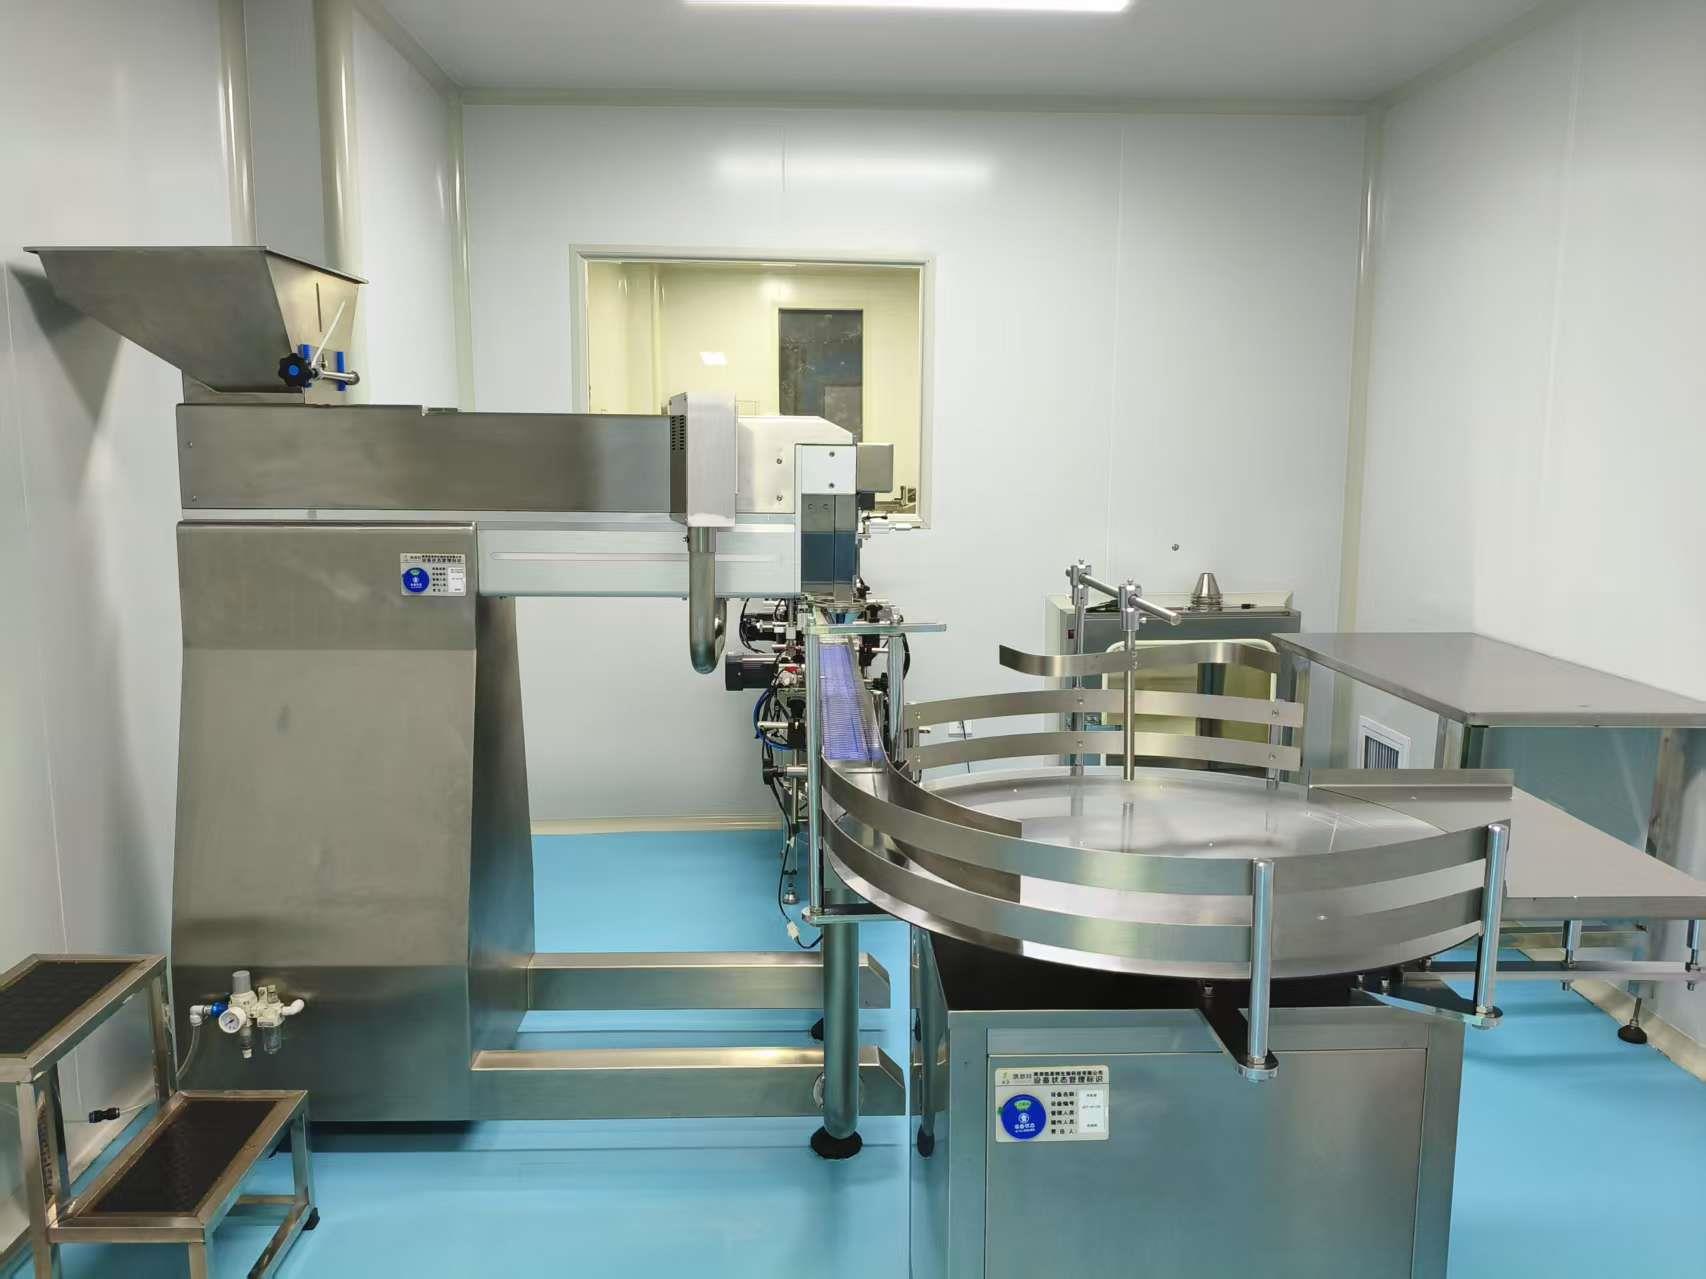
Automated precision dosing units fill hard capsules, bottles, and liquid formats under controlled environmental temperature and relative humidity.
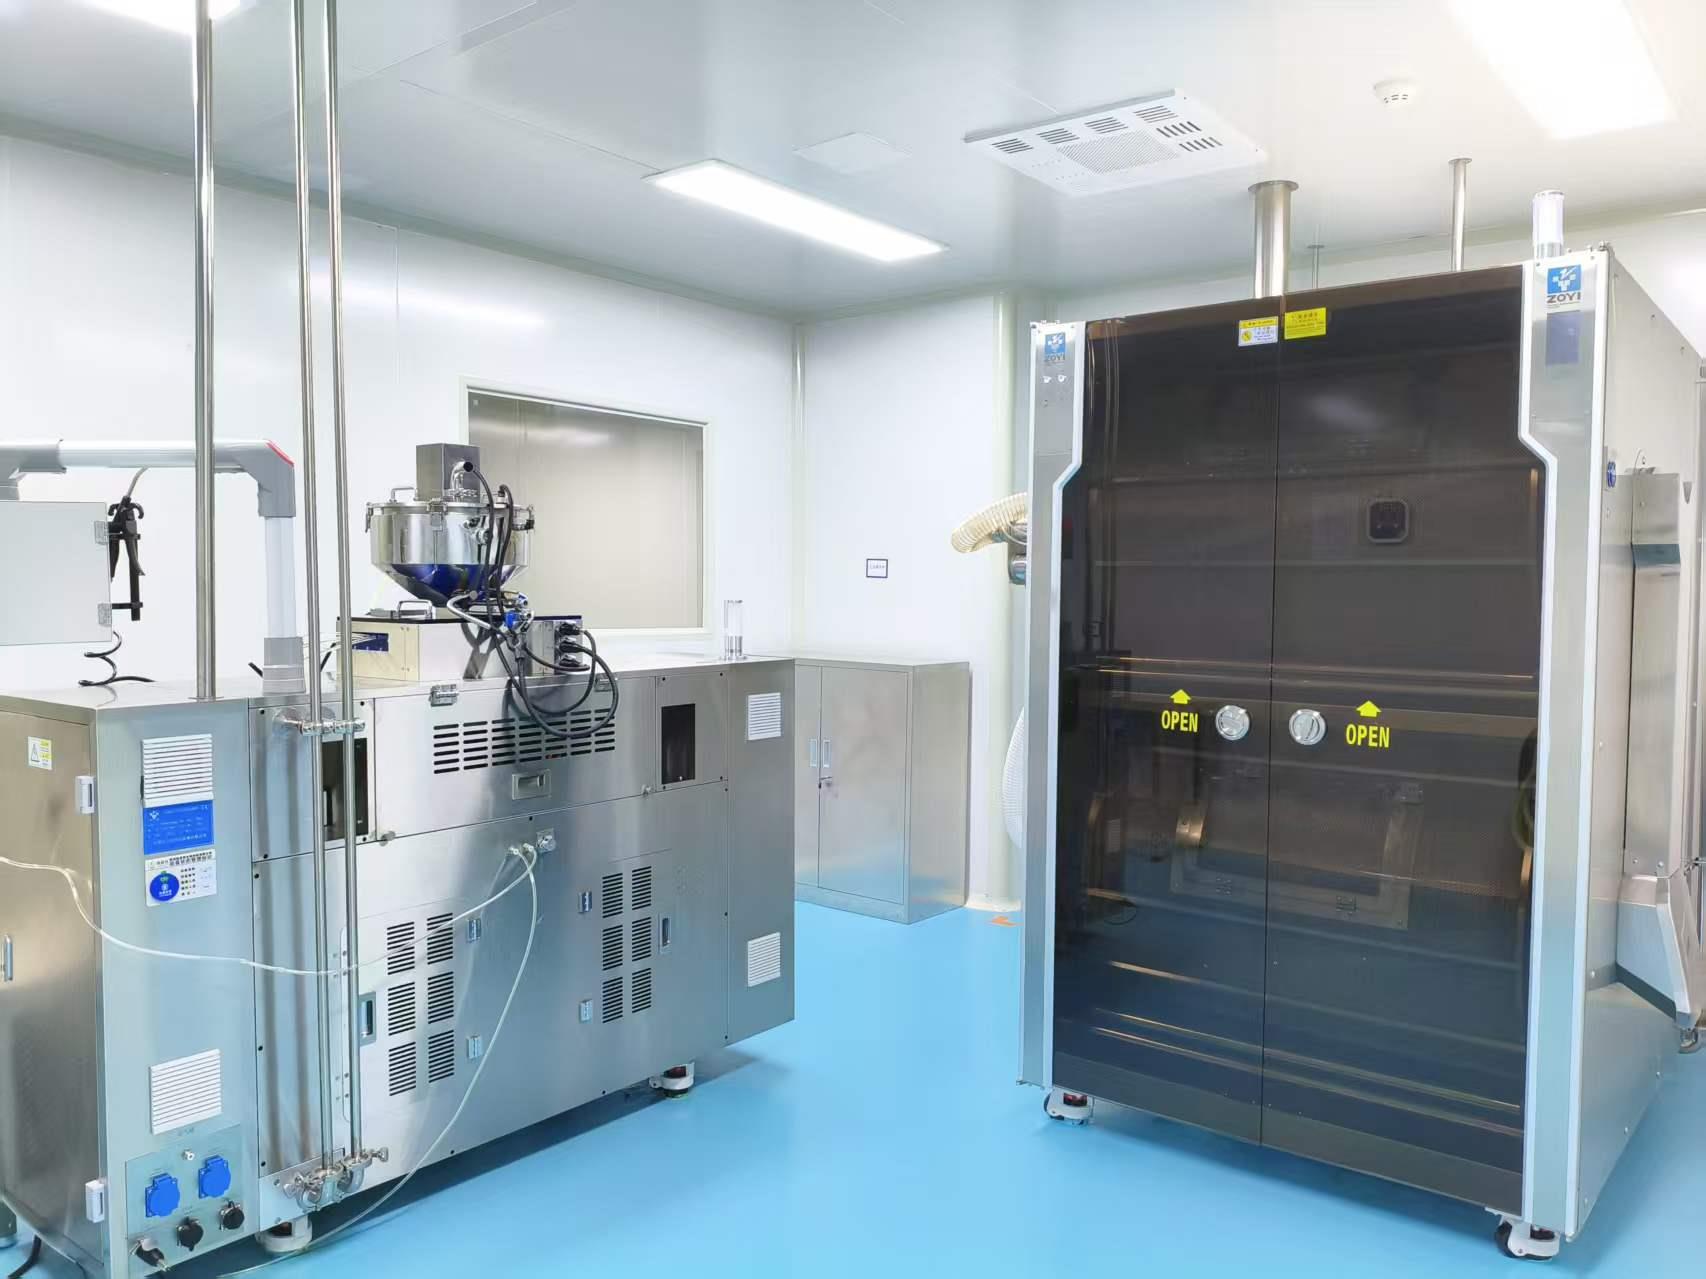
Specialized hydraulic forming equipment produces shilajit balls, herbal drops, and compressed spherical nutraceutical configurations.
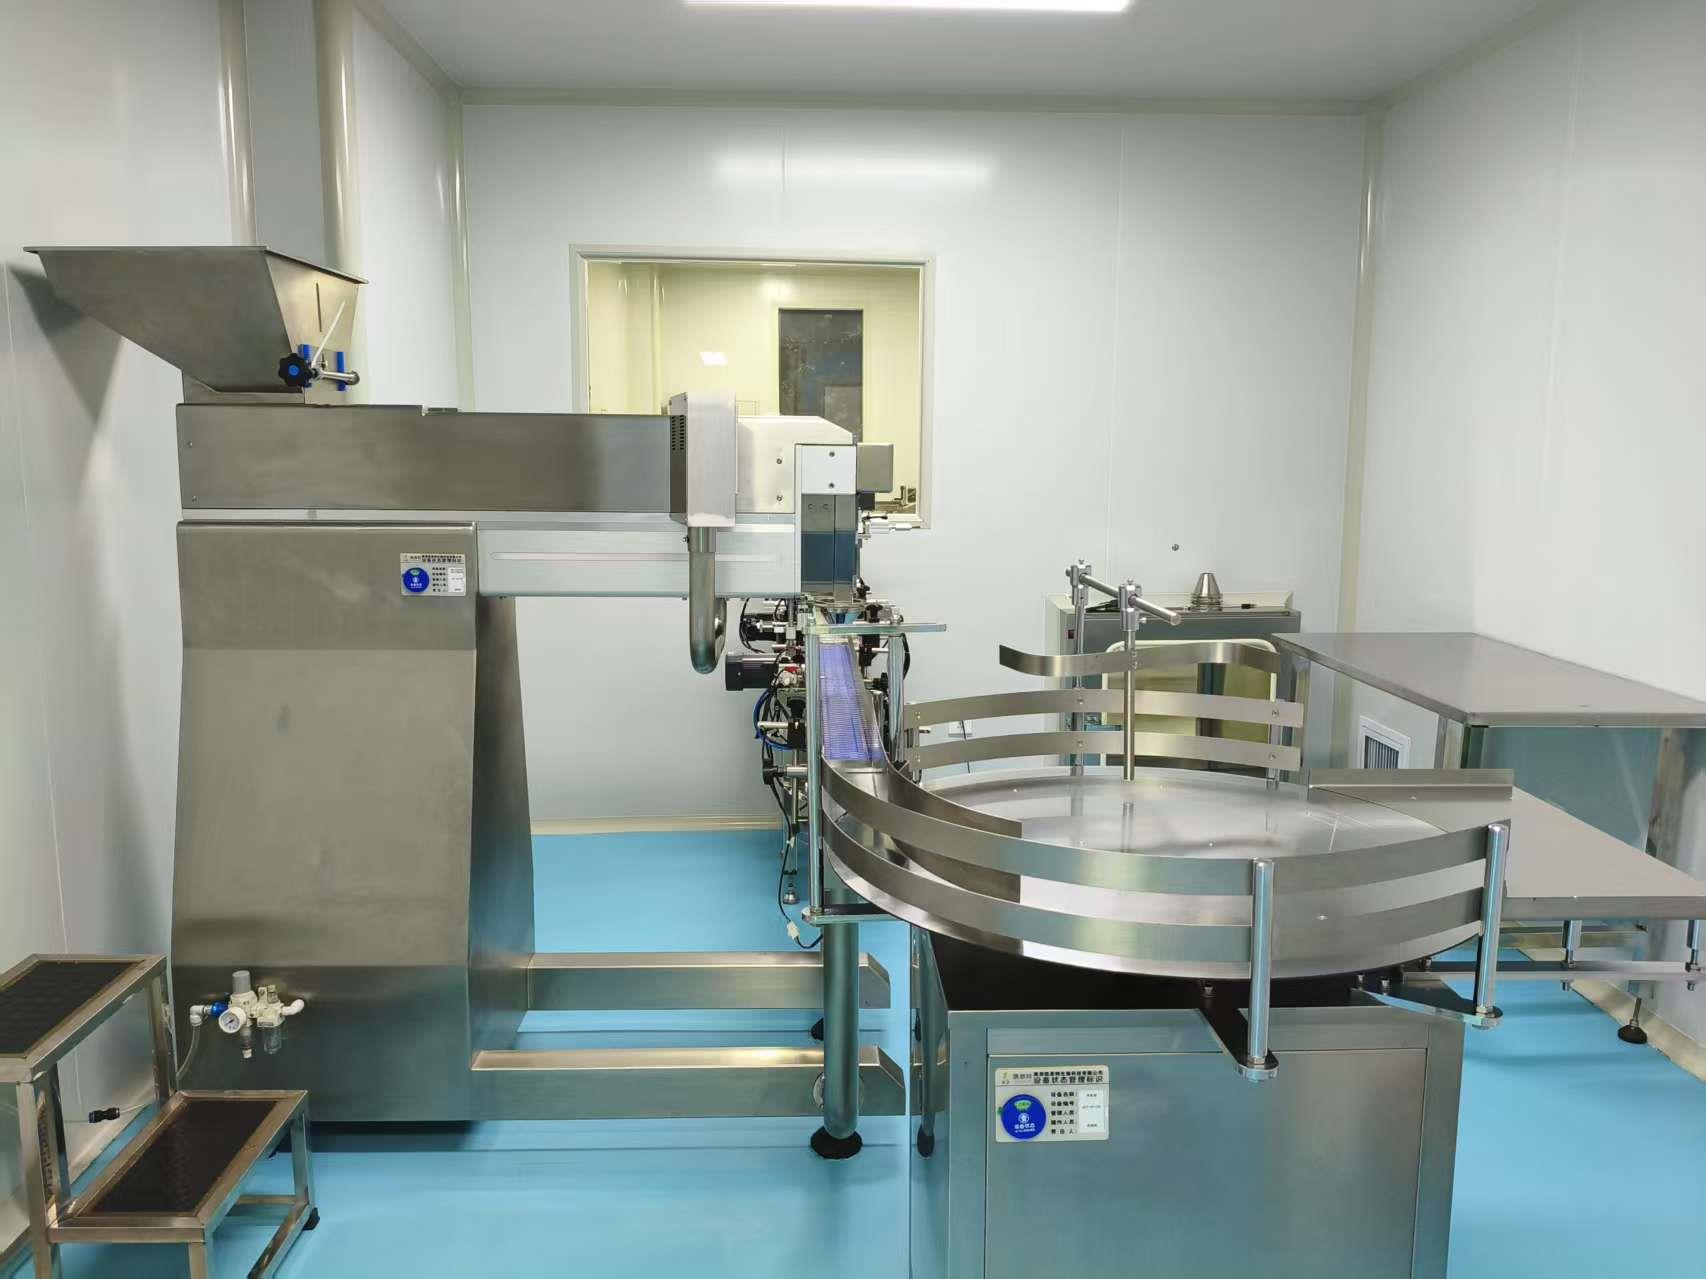
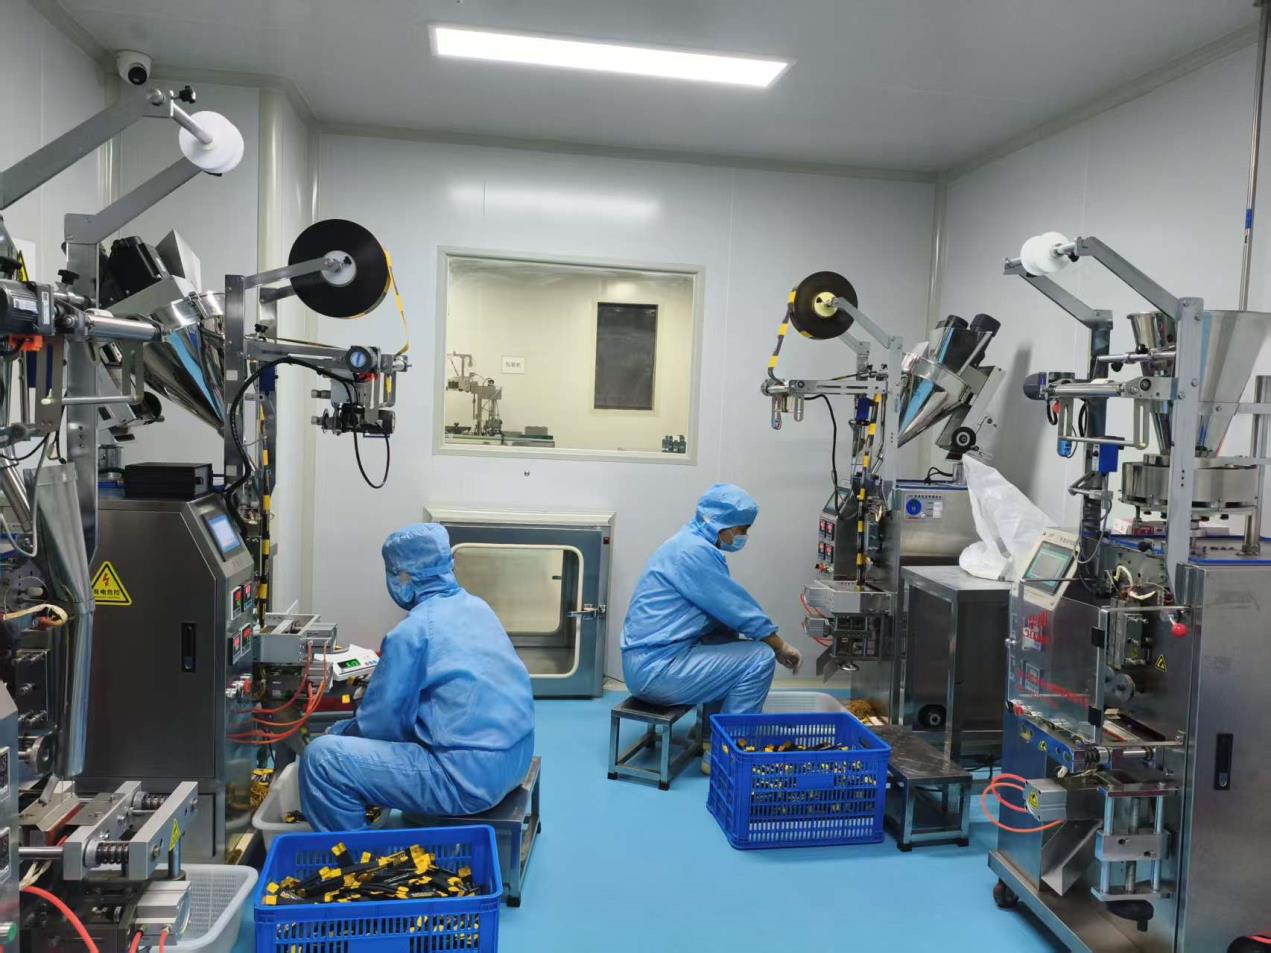
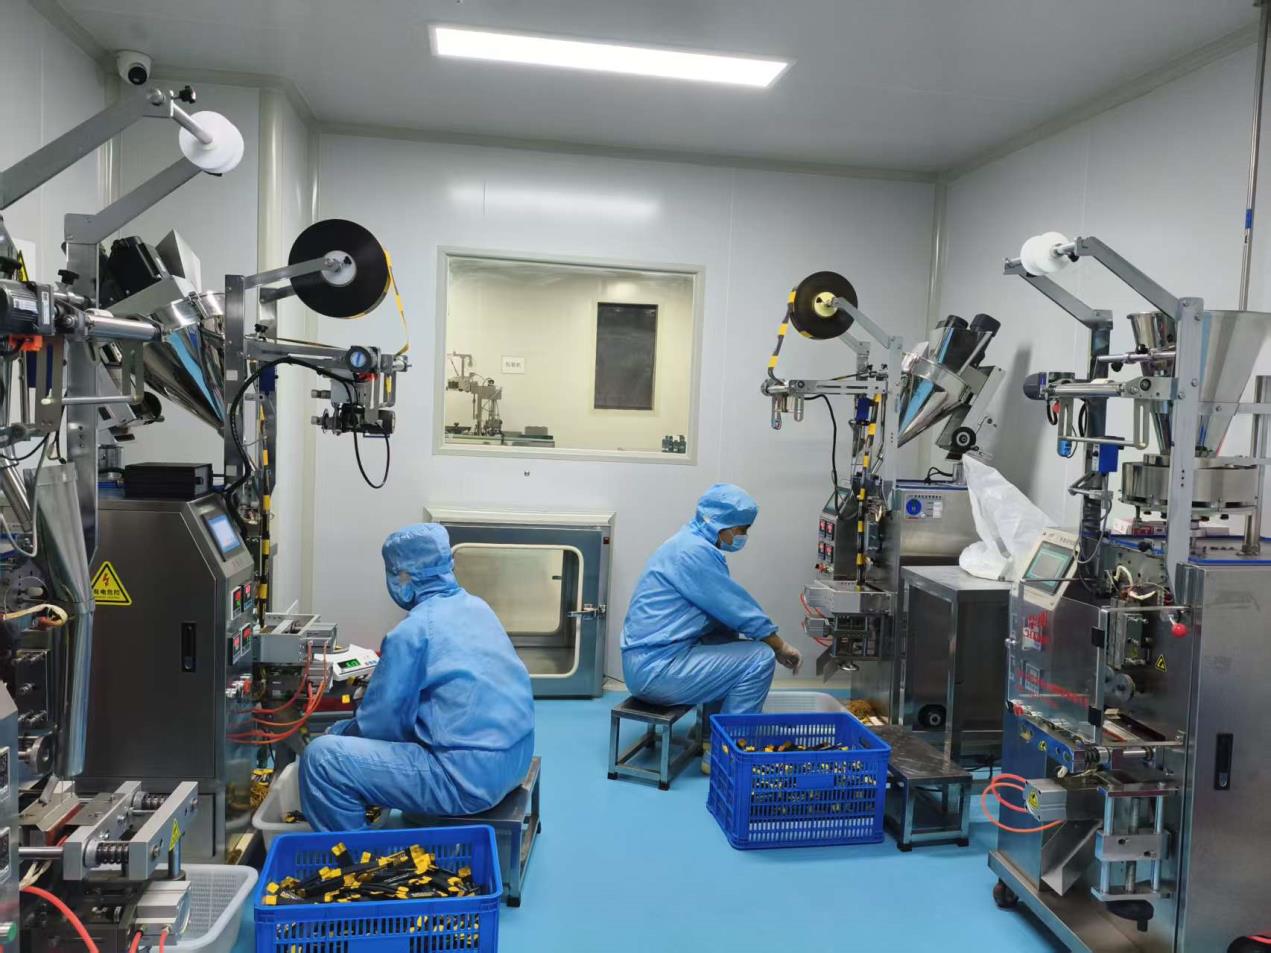
Immediate cleanroom packaging into pharmaceutical-grade PVC/PVDC blisters, HDPE/PET bottles, or aluminum foil moisture-resistant sachets.
Precision cartoning, tamper-evident security sealing, regulatory barcode application, and batch lot coding for retail-ready shelf displays.
Heavy-duty corrugated master cartons, pallet stretch wrapping, and container securing designed to withstand air and sea freight logistics.
Shaanxi ESNO Biotech Co., Ltd. invests in automated machinery designed for high throughput, minimal human intervention, and strict repeatability.
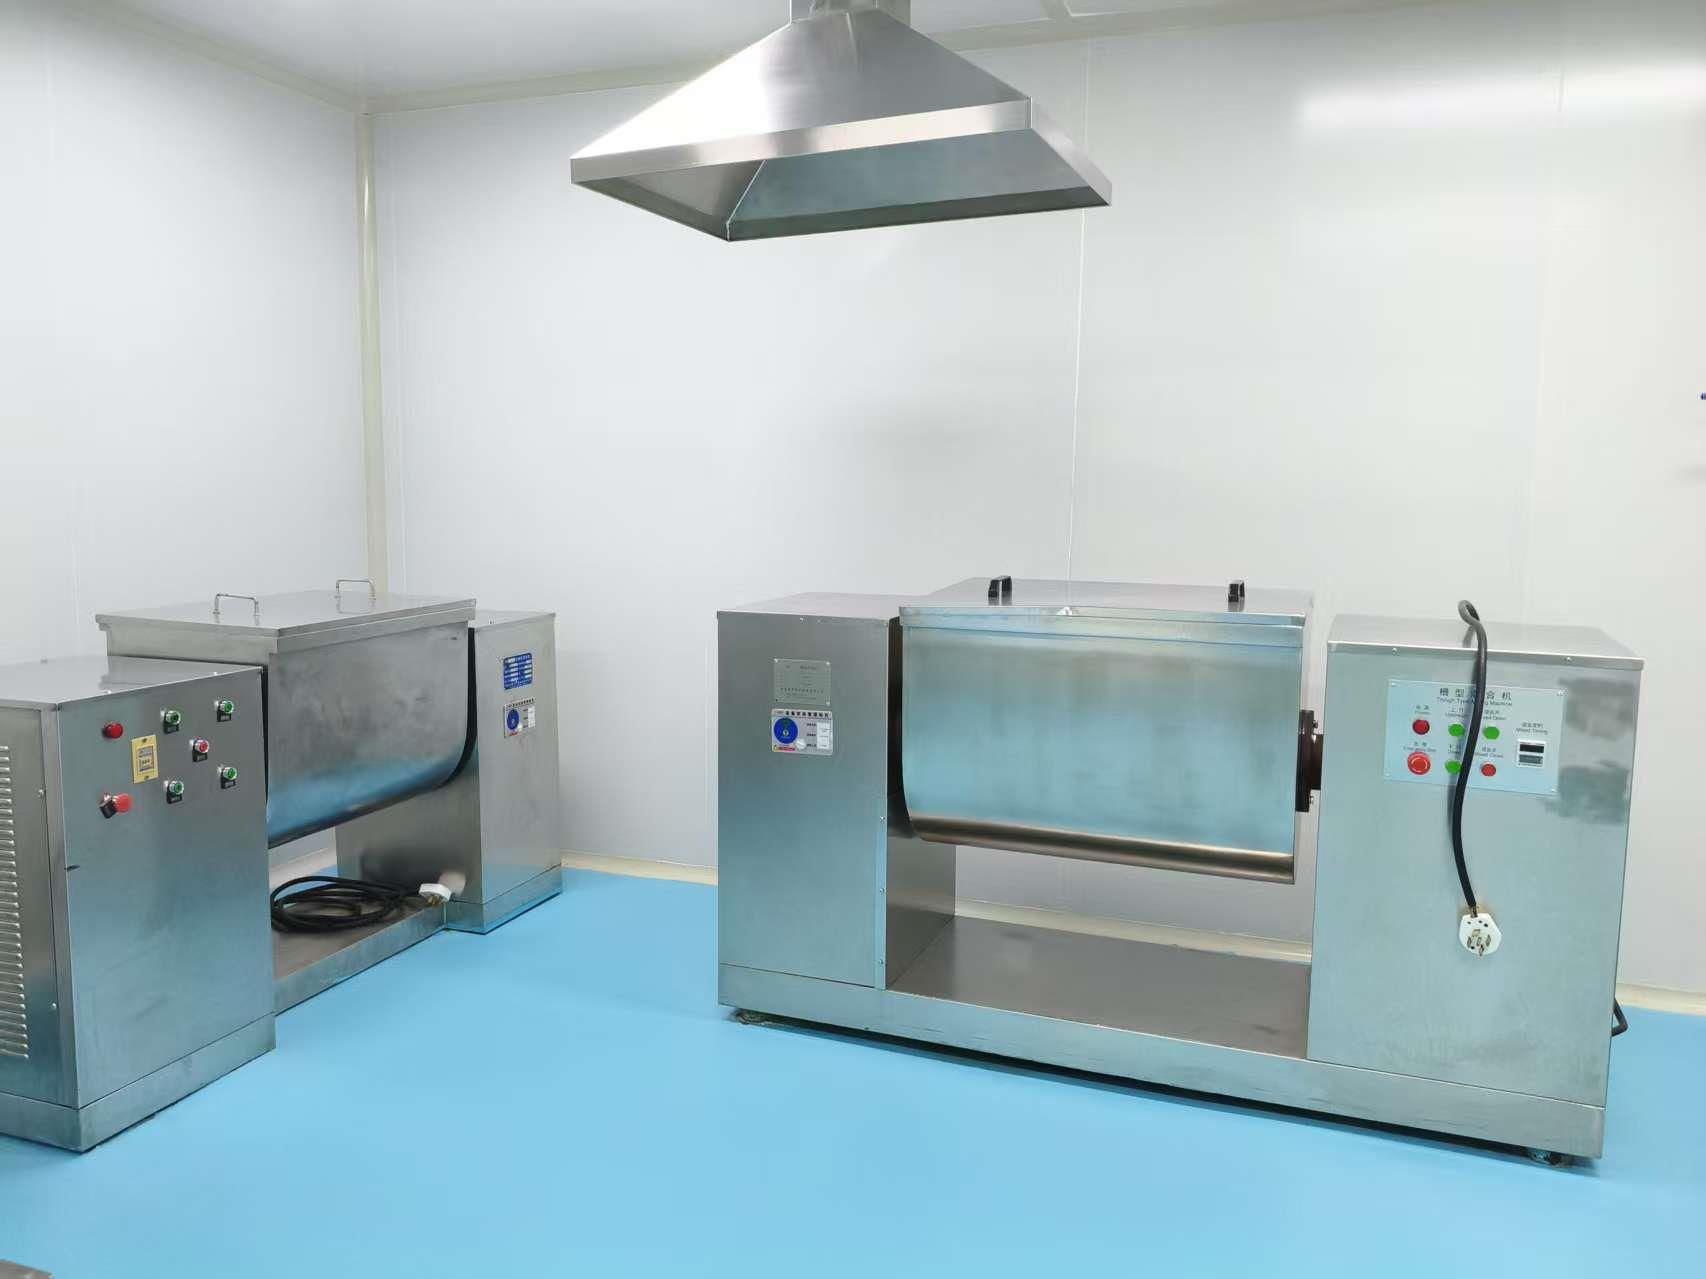
Sanitary stainless-steel industrial blenders designed for uniform cross-blend coefficient of variation, preventing ingredient separation.
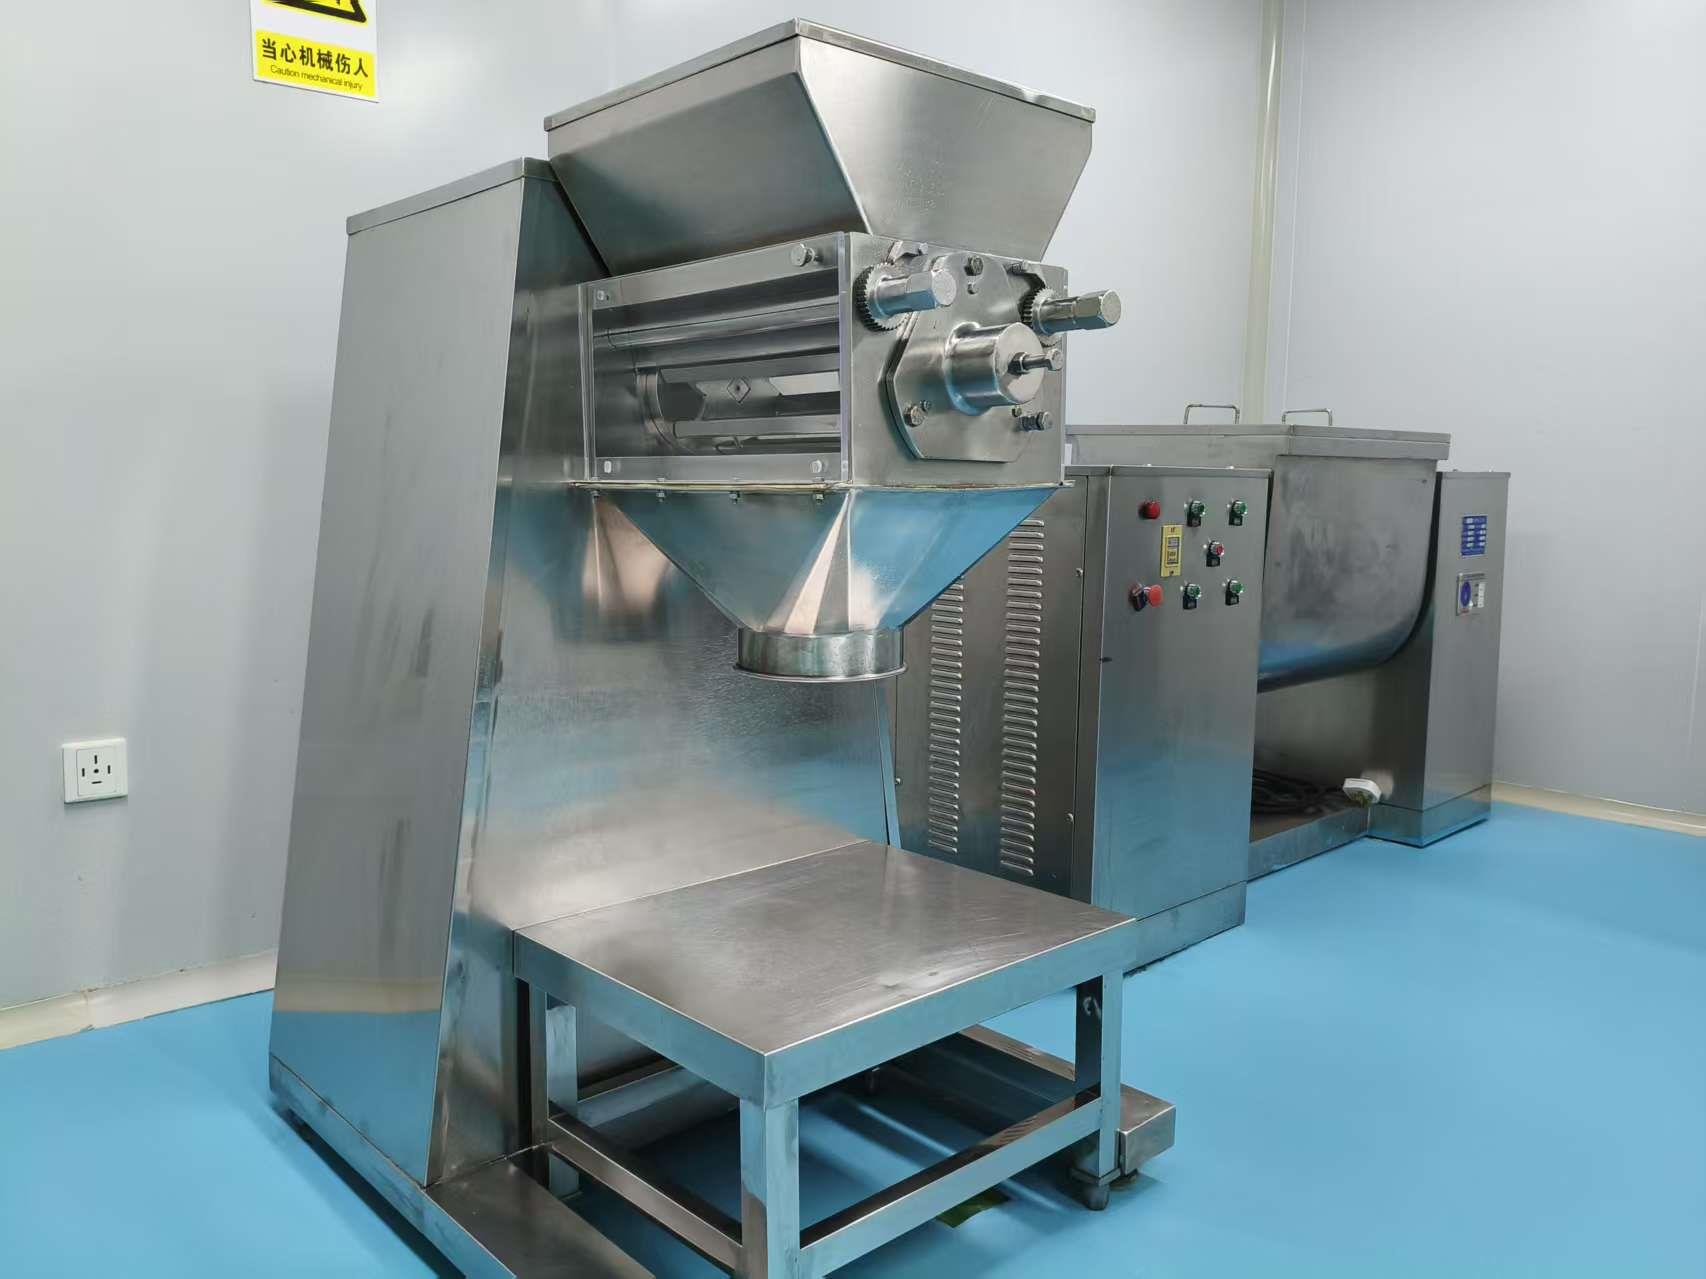
High-shear wet and dry granulation apparatus establishing tight granule size distributions to ensure smooth downstream tablet compression.
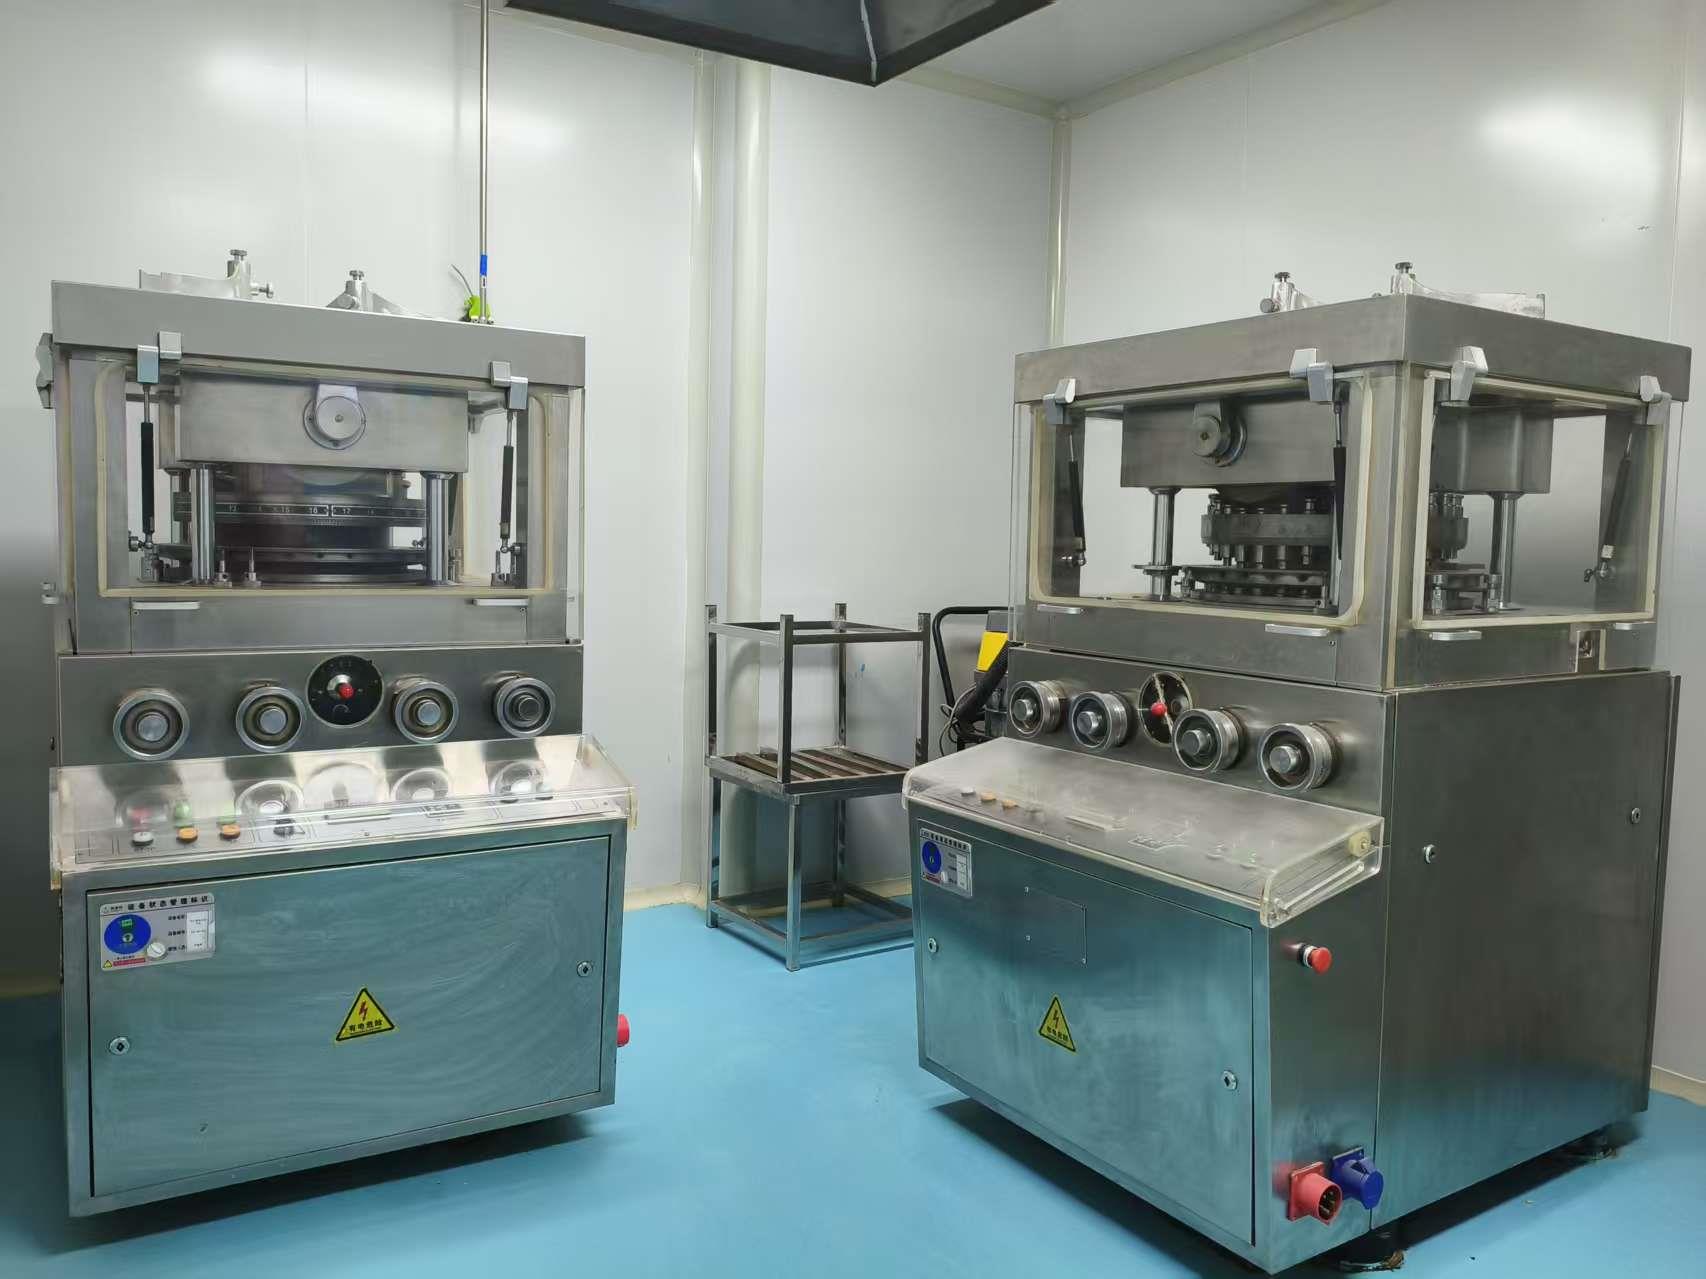
Multi-station rotary compression presses with automated tooling protection, pressure sensors, and high output capacity for diverse shapes.
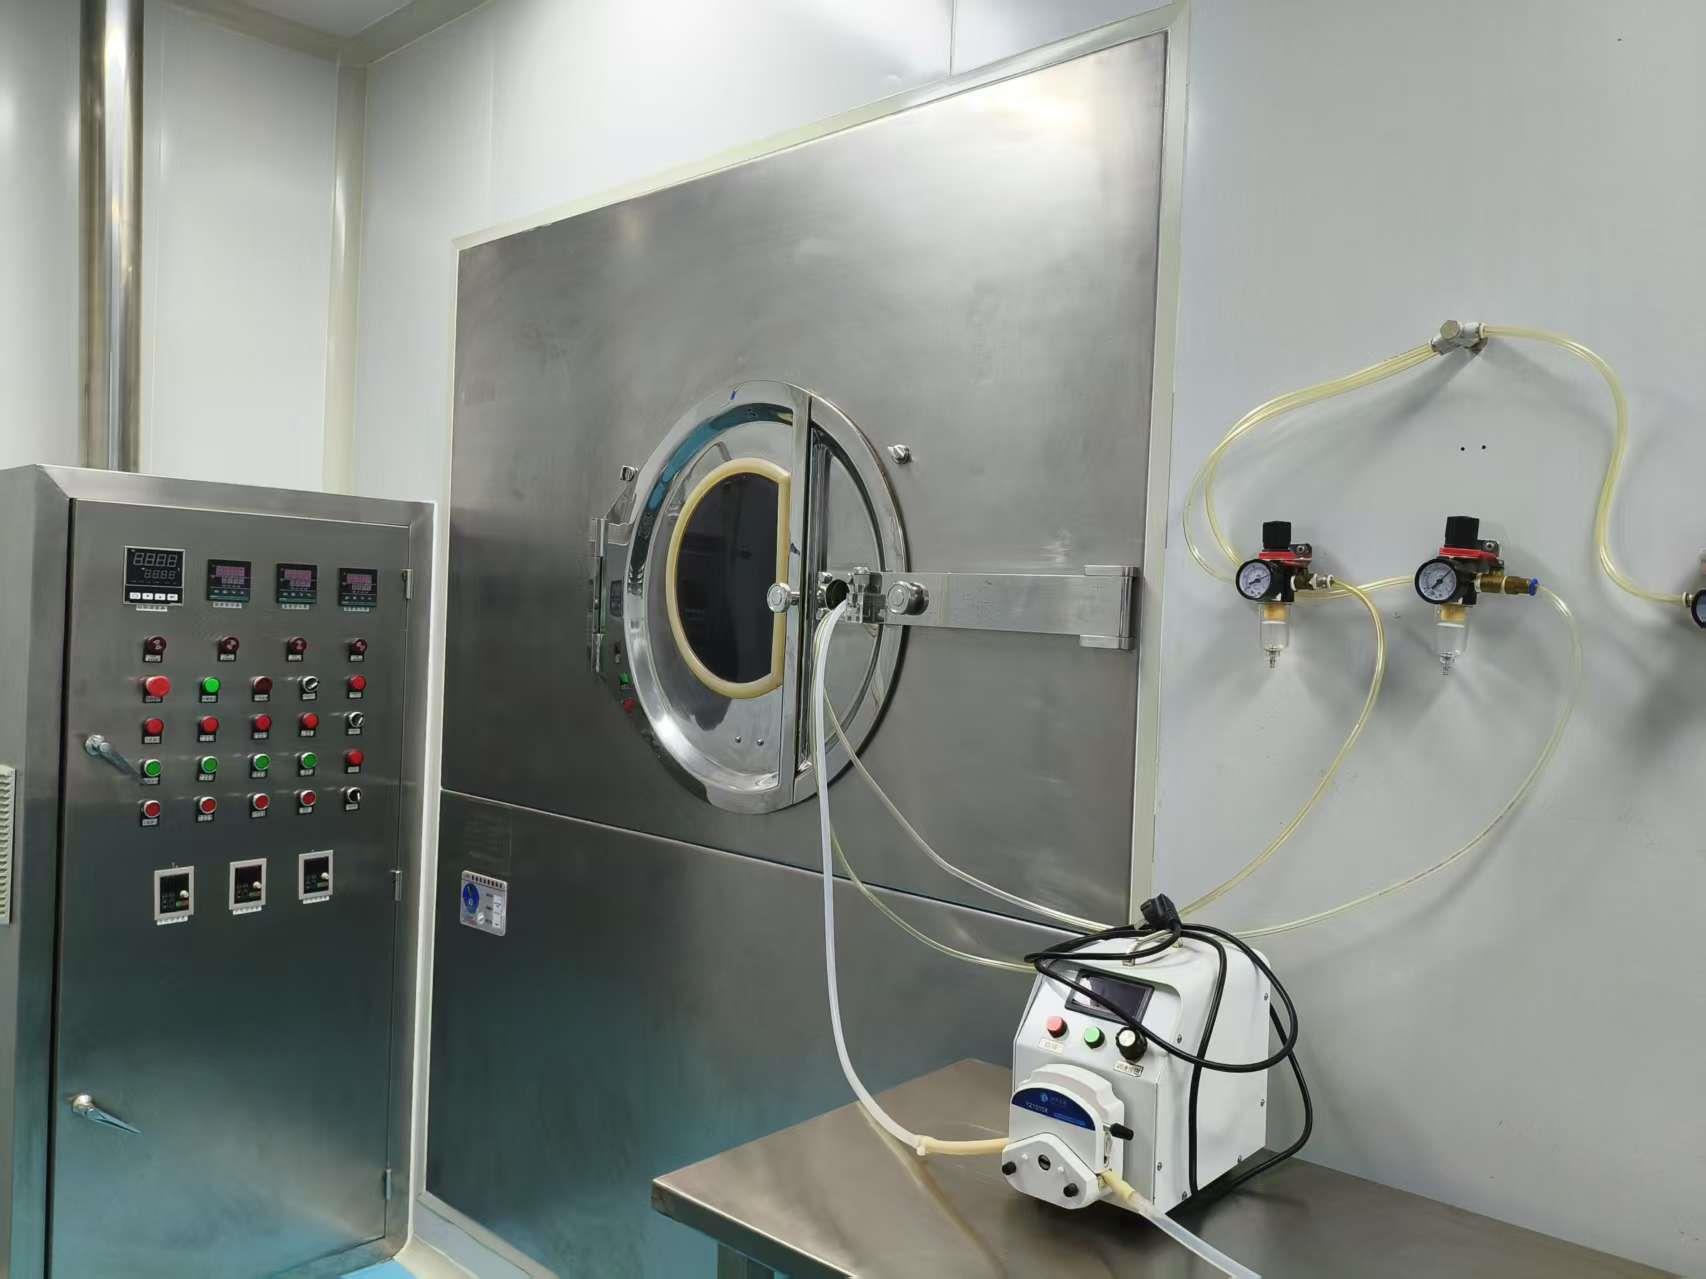
Perforated drum coating units featuring automated spray guns, negative pressure ventilation, and thermal control for flawless film application.
Multi-lane vertical form fill seal machinery producing air-tight sachet packaging and stick packs for pre-measured powders and formulations.
Integrated packaging conveyor with automated bottle unscramblers, electronic tablet counters, desiccant inserters, and torque cappers.
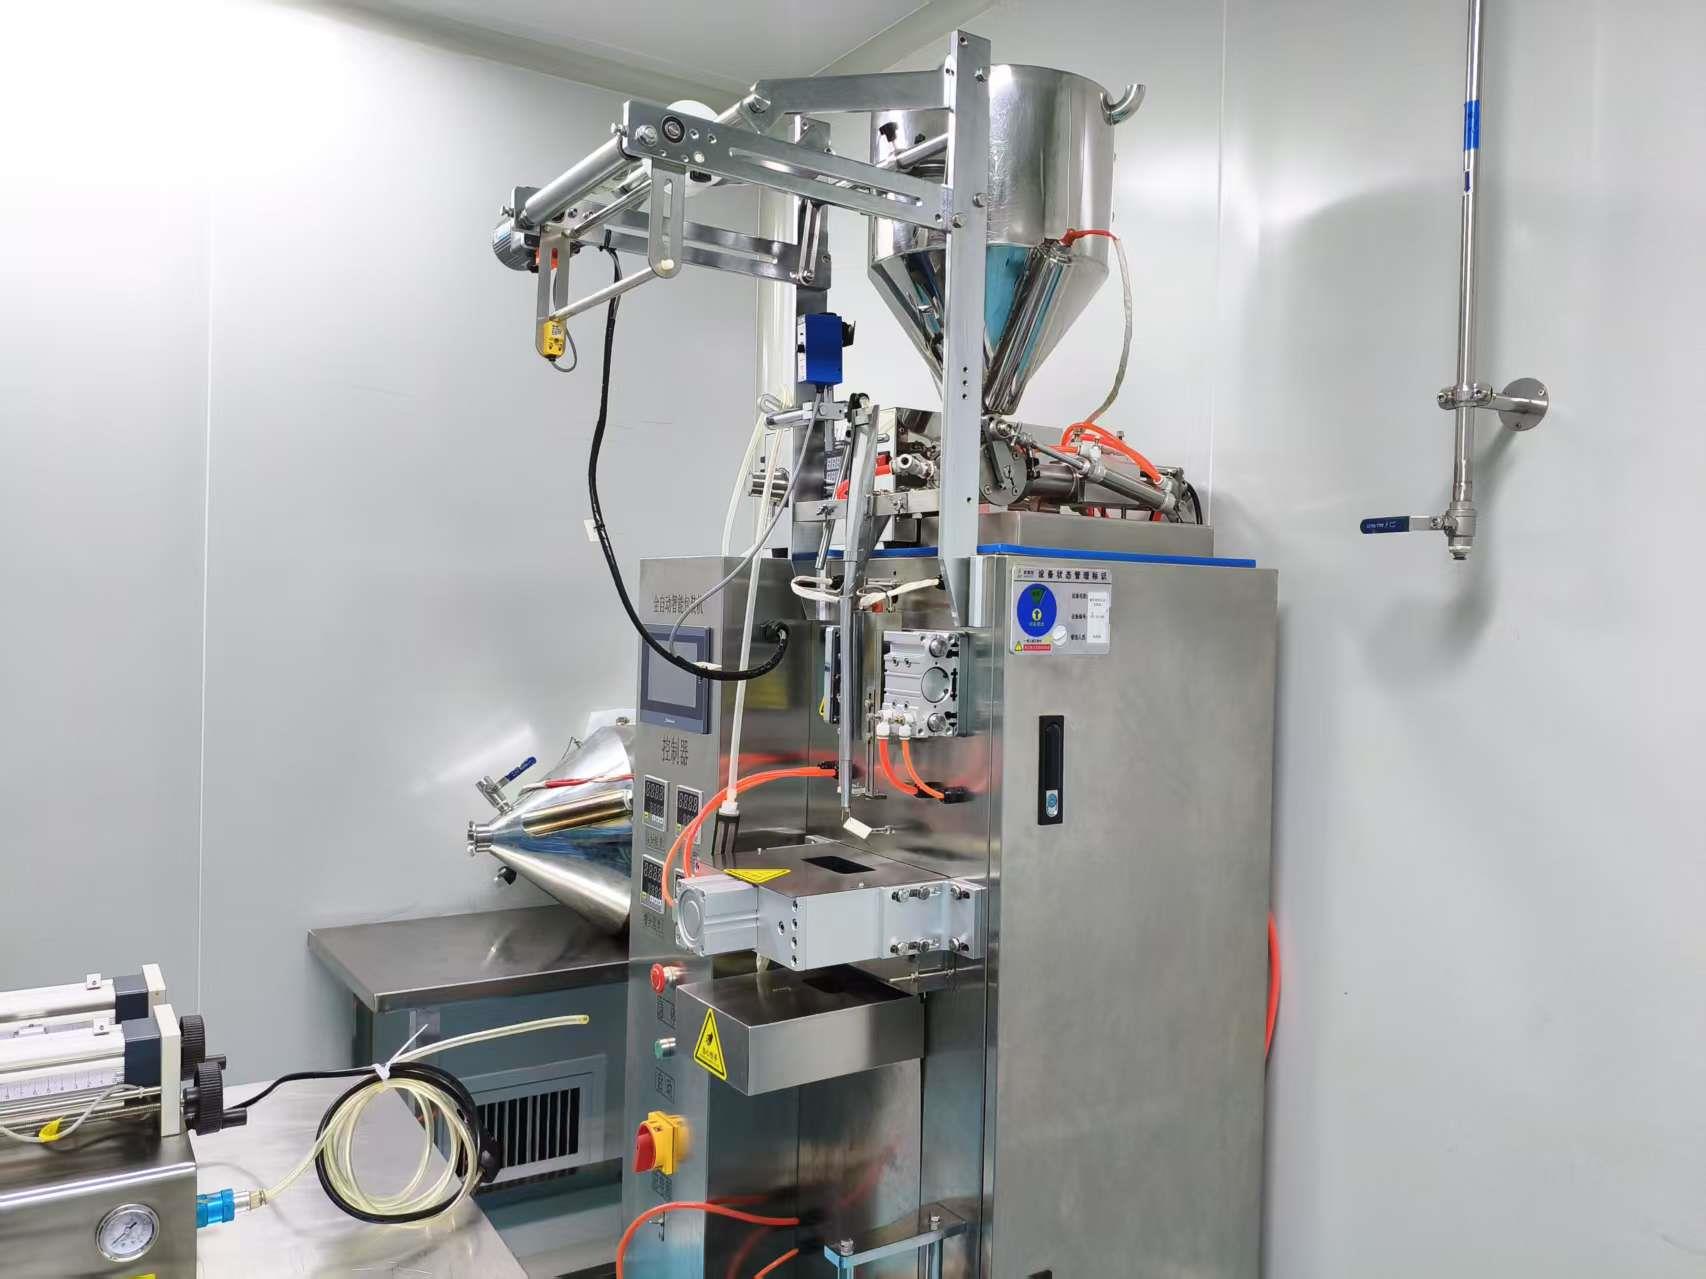
High-precision volumetric and auger filling systems guaranteeing exact fill weight for powders, capsules, and specialty herbal preparations.
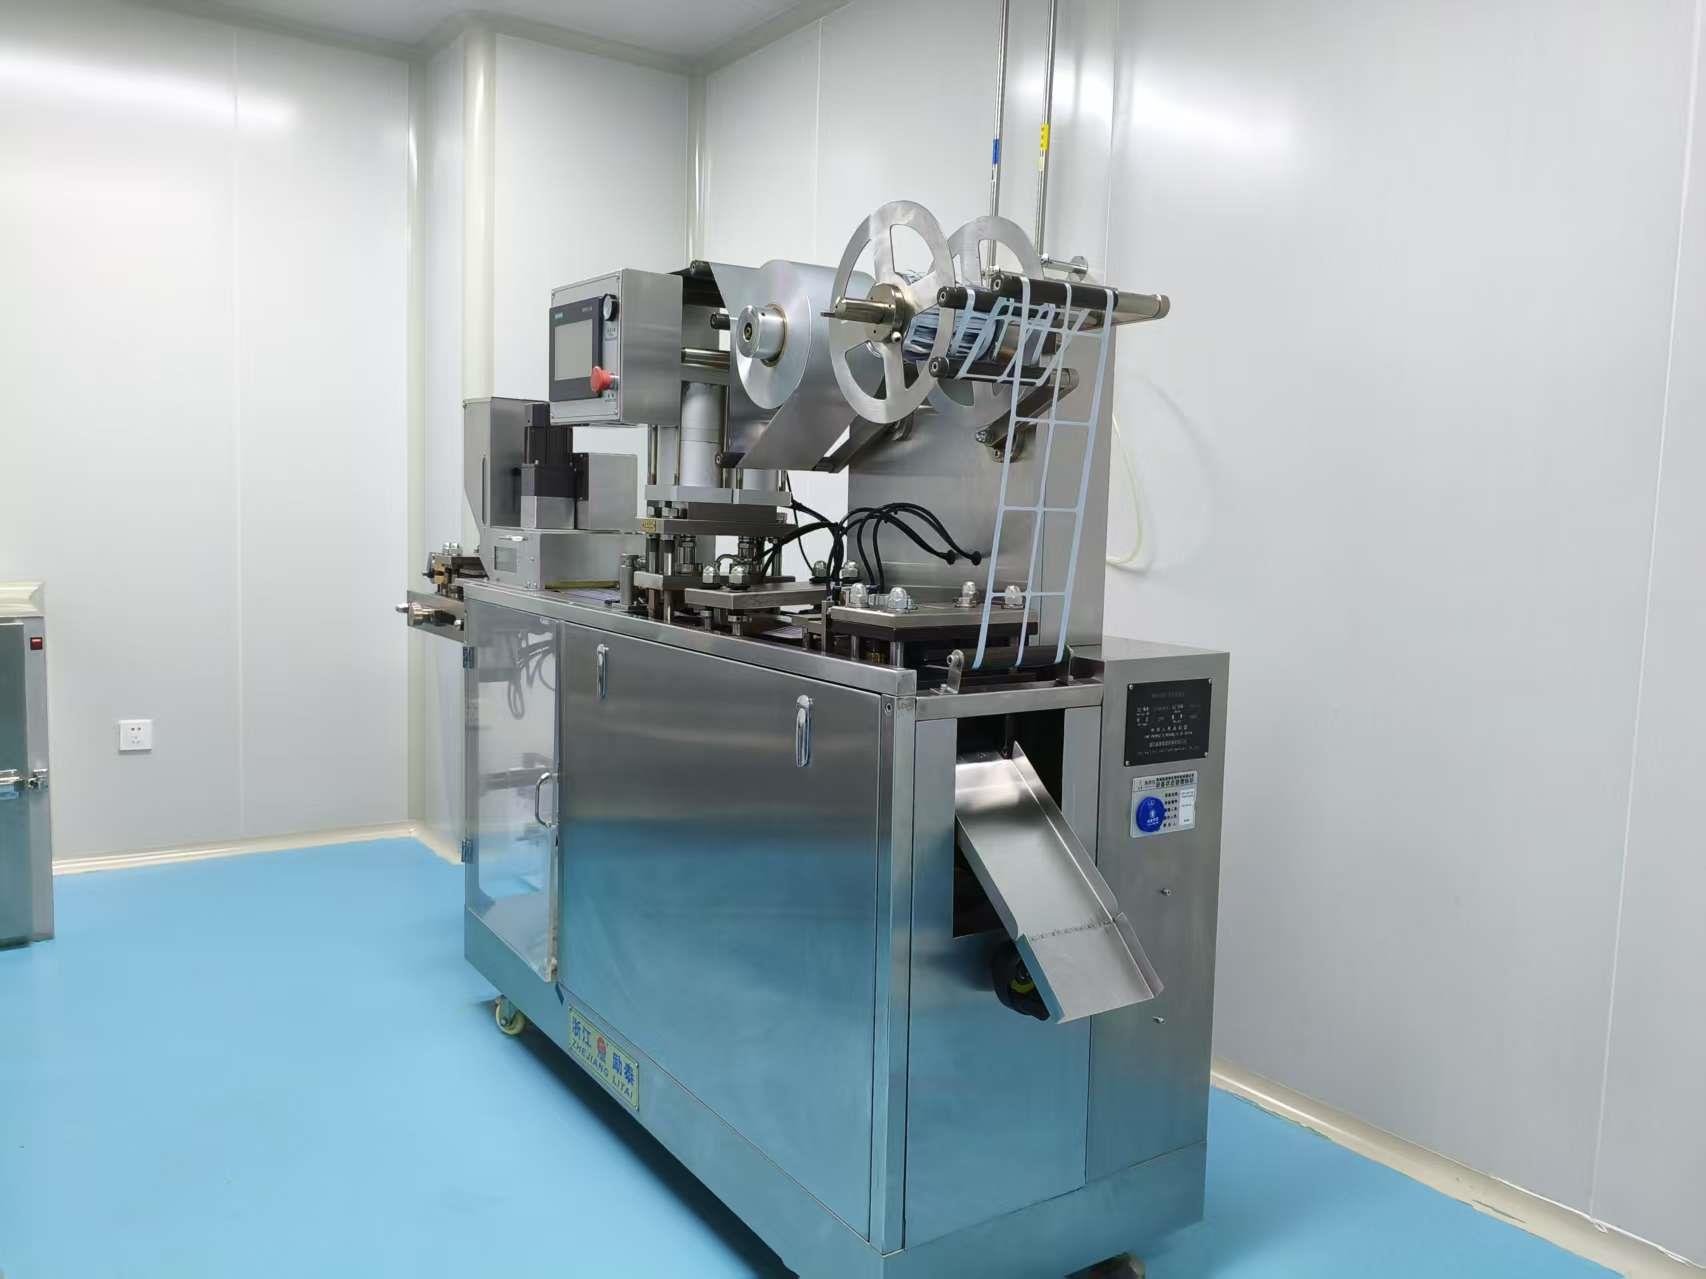
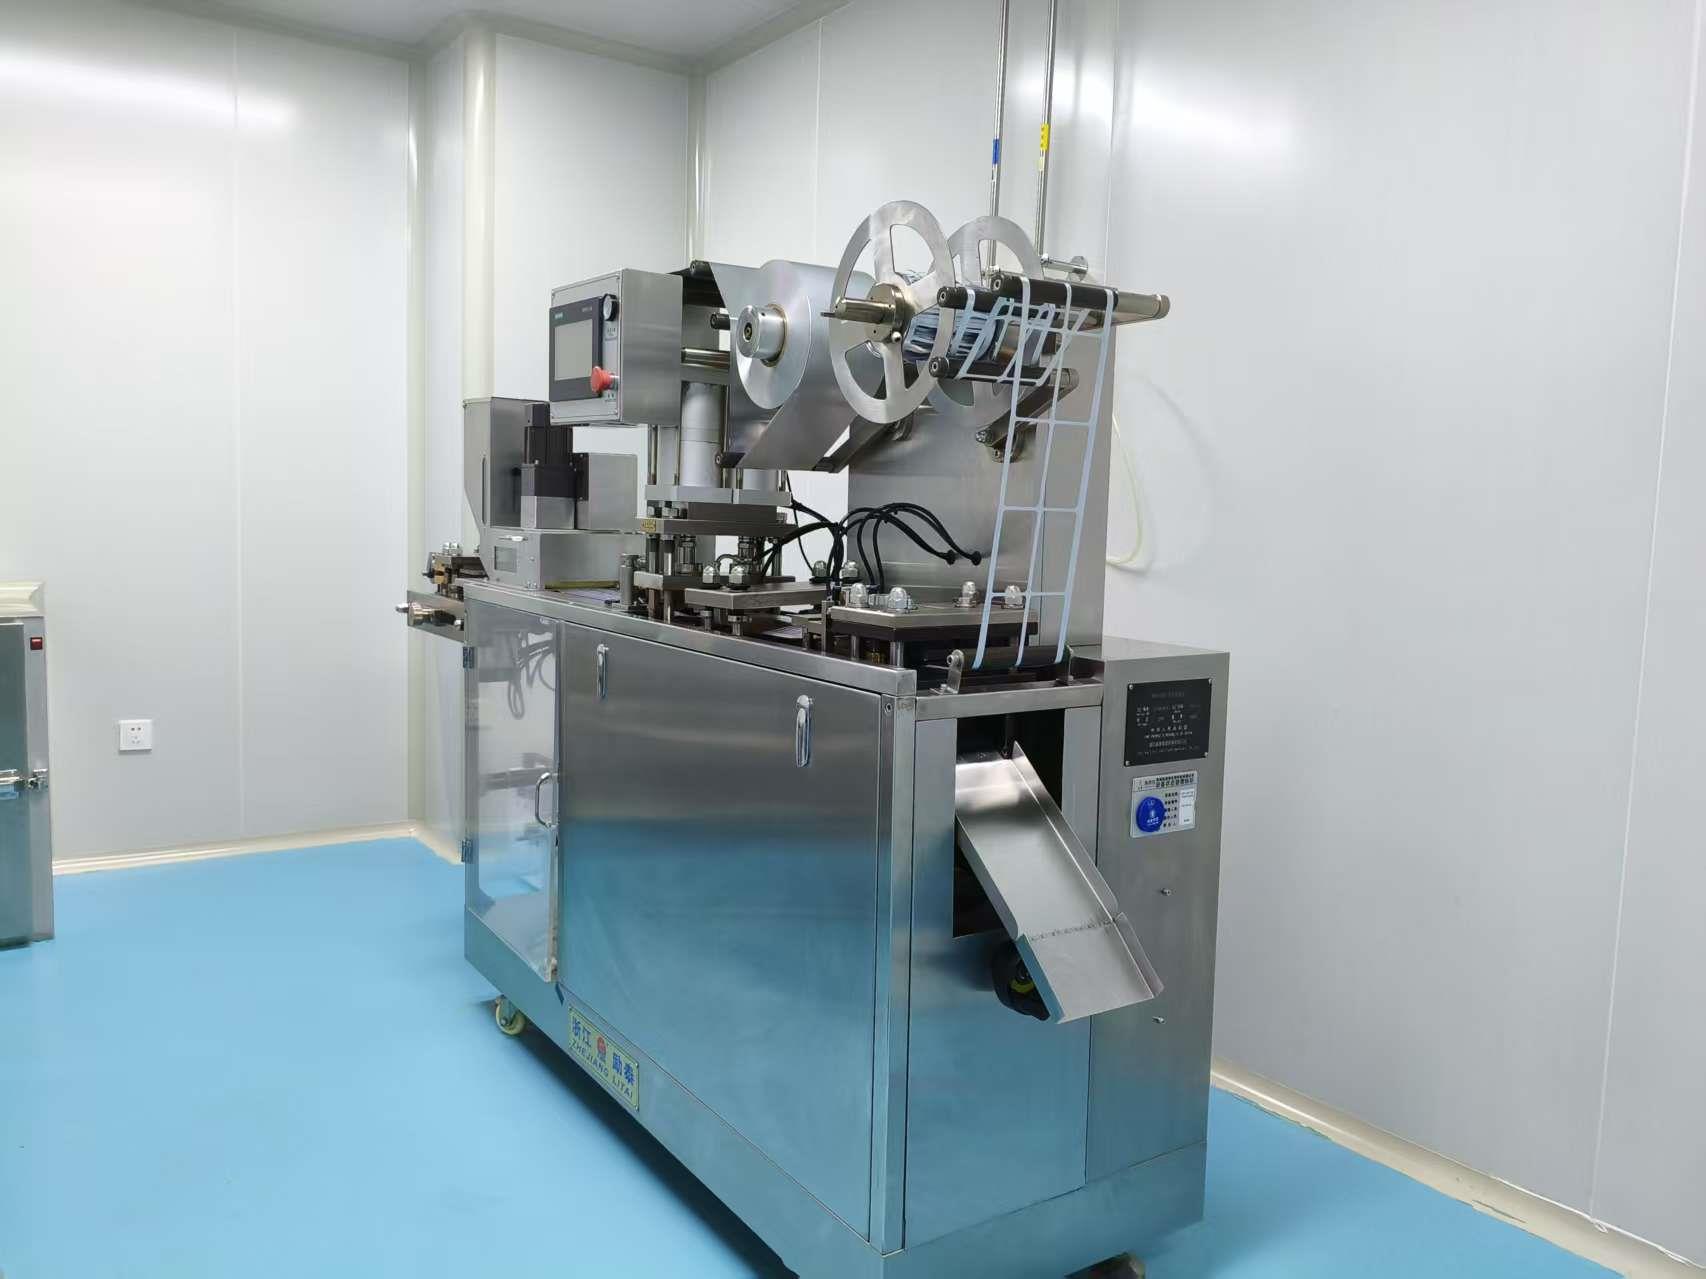
High-speed thermoforming Alu-PVC blister machinery delivering hermetic seals to protect active compounds against humidity and oxidation.
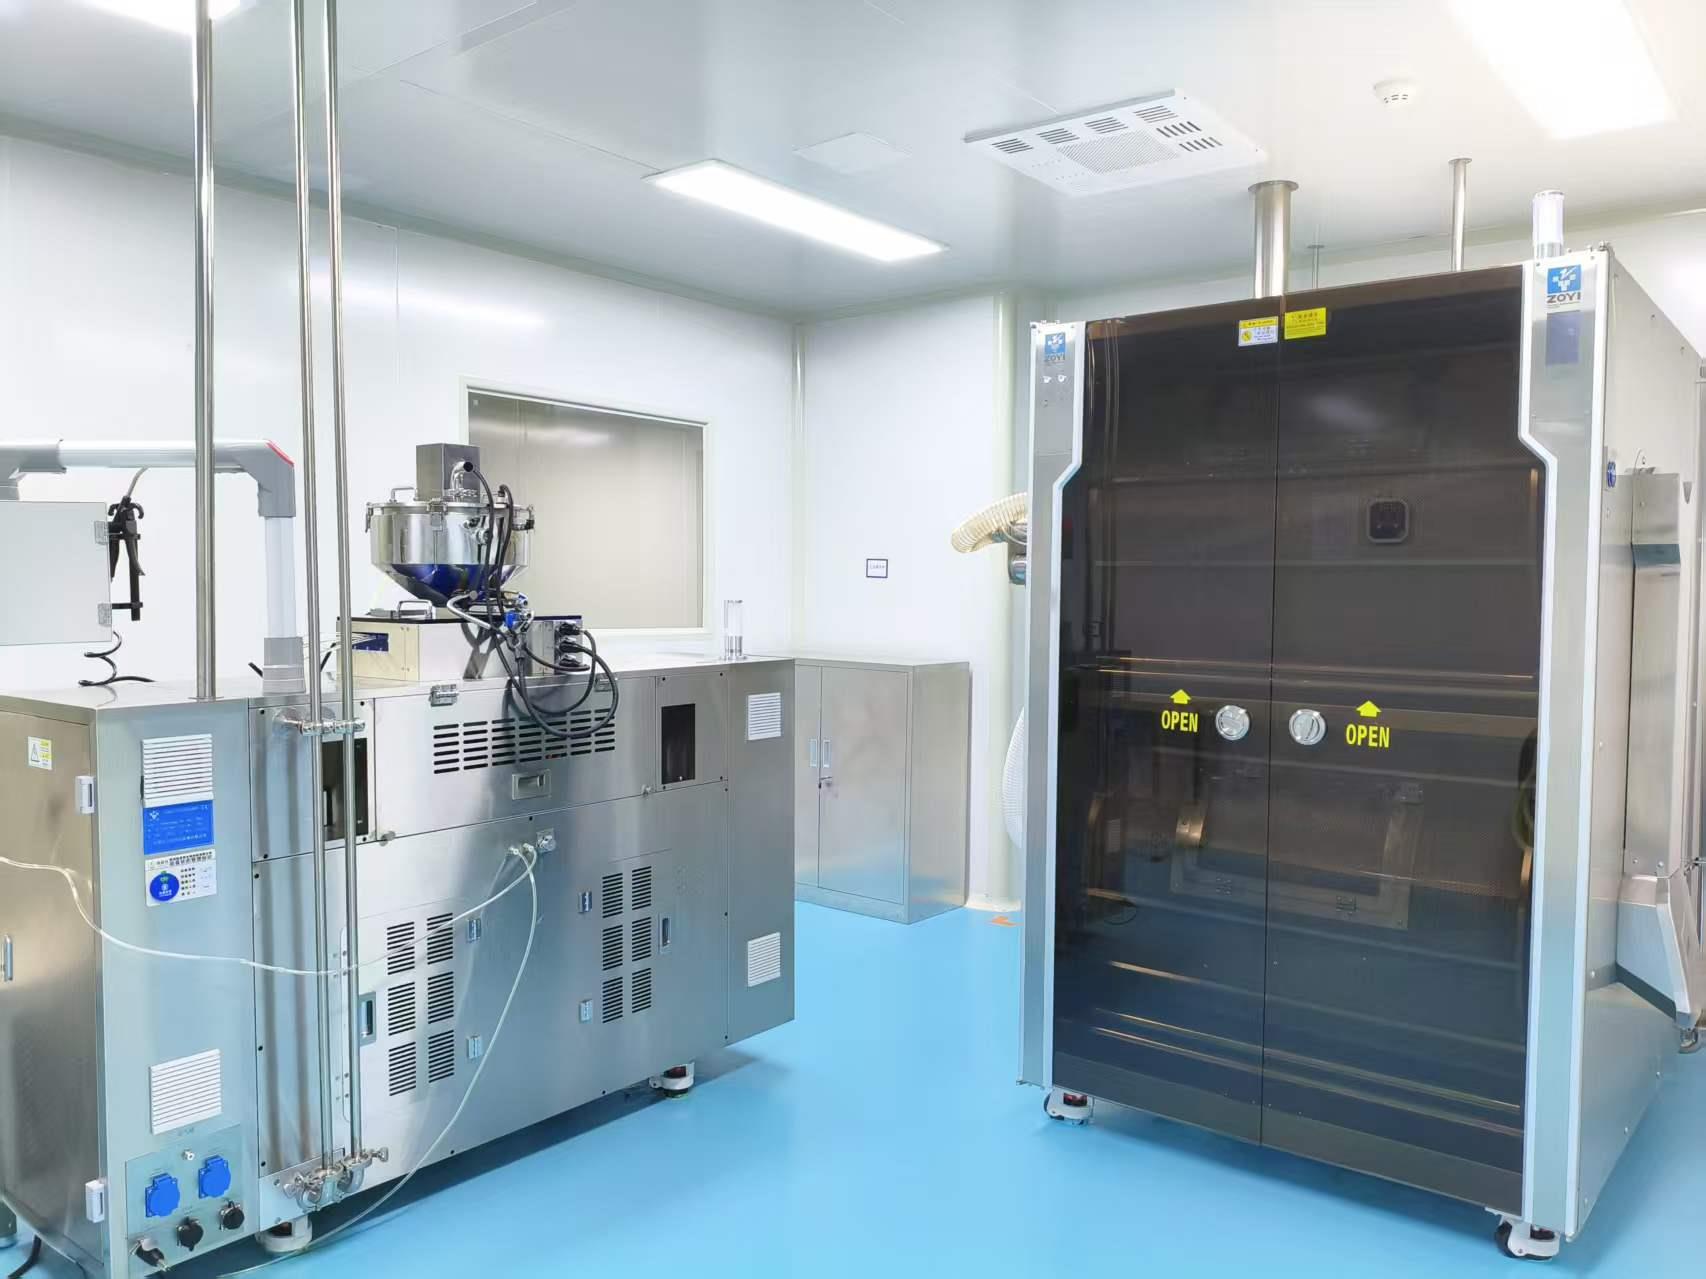
Custom engineering units engineered specifically for shaping dense resin concentrates and compressed drops with consistent unit weight.
Our in-house analytical laboratories are staffed by certified chemists and technicians running comprehensive microbial, physical, and chemical evaluations.
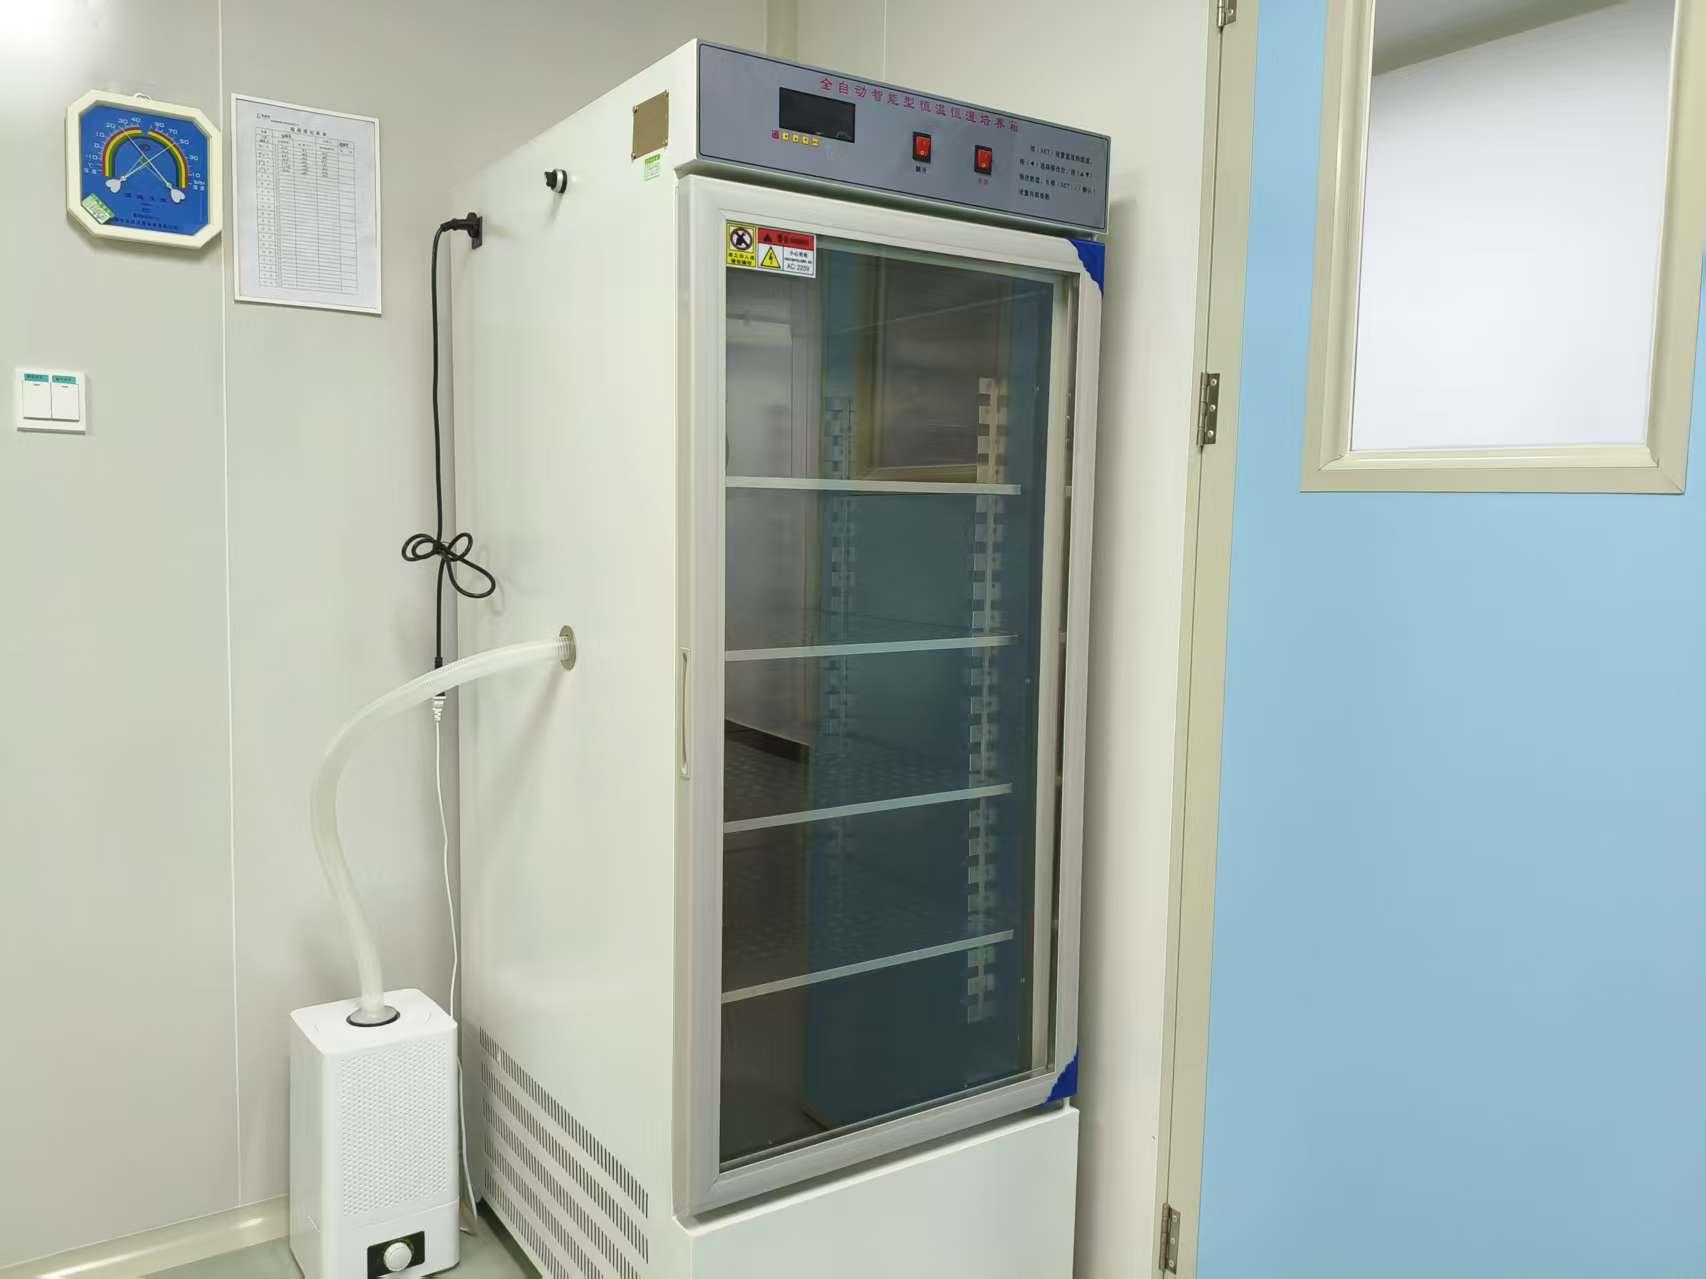
Calibrated microbiological incubators for aerobic plate count, yeast and mold identification, coliform testing, and pathogenic screening.
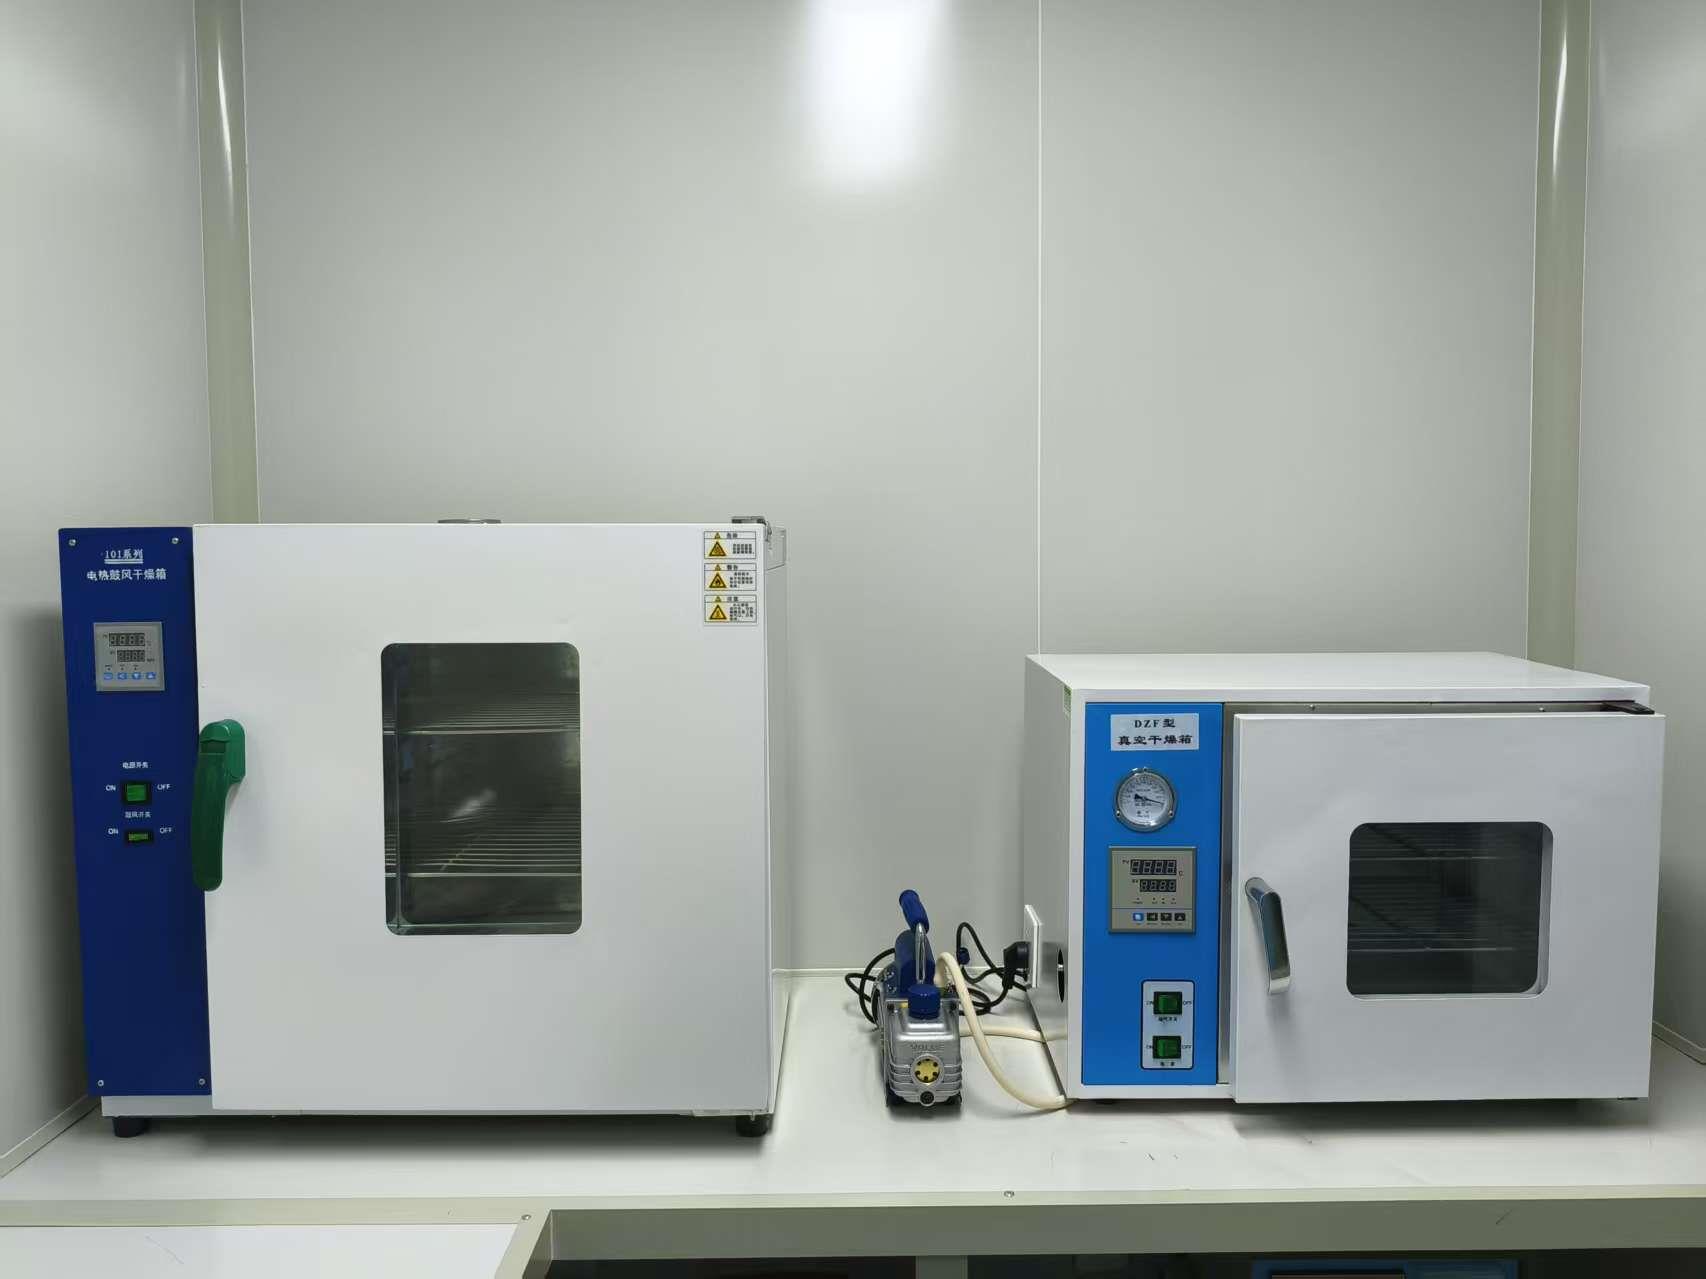
Thermostatically controlled drying ovens used for loss on drying (LOD) moisture determination, stability testing, and dry matter evaluation.
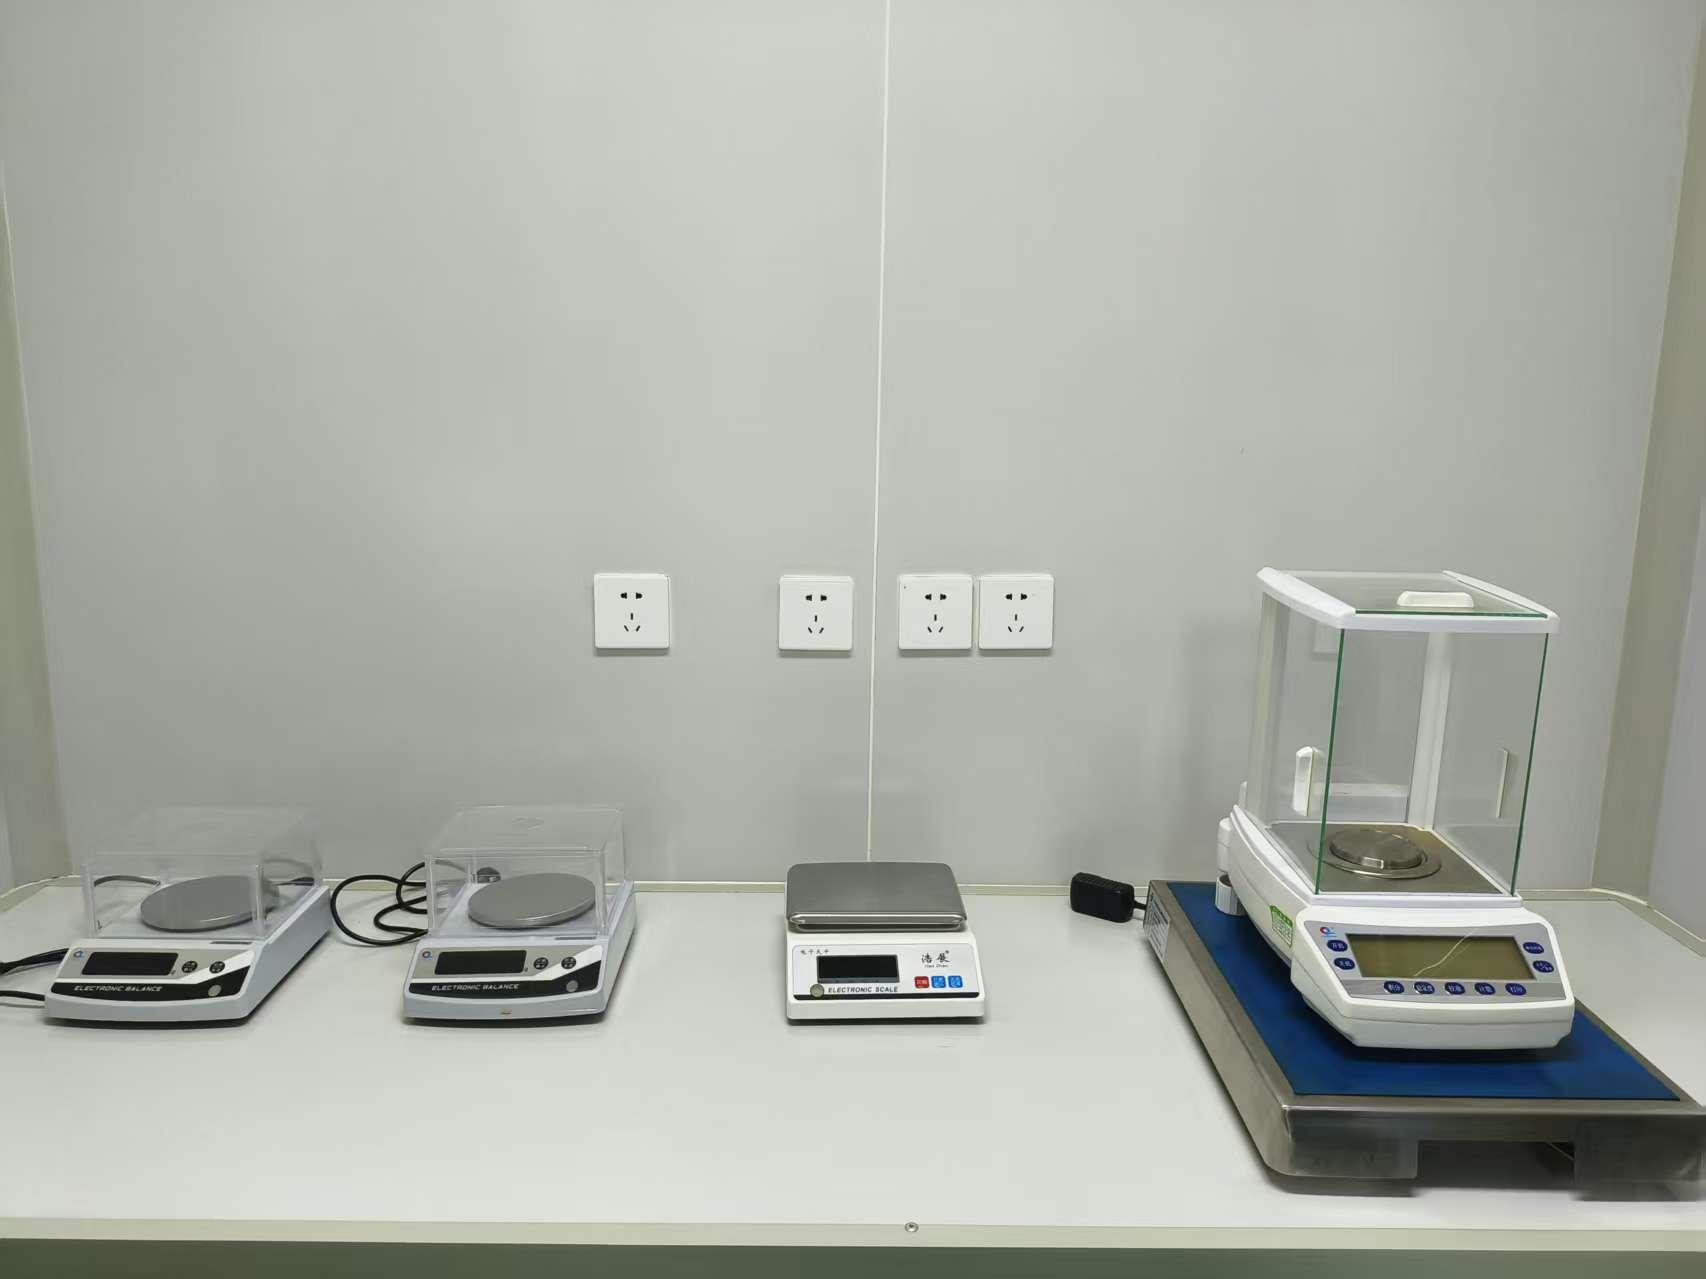
High-sensitivity analytical balances (0.1 mg precision) ensuring accurate micro-ingredient calibration, titration, and standard preparation.
Whether you require turn-key private label manufacturing, custom formula development, or pilot batch samples, our dedicated B2B project managers are ready to assist.