Standardized Botanical & Nutraceutical Formulations
Batch-verified, high-potency encapsulated formulations manufactured according to NSF 455-2 GMP, ISO 22000, and TÜV Rheinland-certified parameters for regional brands.
19+
Years of Direct Extraction Experience (Since 2006)
100+
Export Destination Markets Validated
400+
Proprietary Custom R&D Formulations Designed
3,500+
Global Brand & Distribution Partners
Strategic Sourcing of Concentrated Plant Extracts in Villa Nueva and Regional Industrial Corridors
The industrial landscape across the municipality of Villa Nueva—strategically positioned along the vital CA-9 South logistics highway connecting Guatemala City to Puerto Quetzal—serves as Central America’s premier conduit for raw material aggregation, pharmaceutical fabrication, and FMCG manufacturing. For procurement officers, contract research organizations (CROs), and private-label distributors operating within Villa Nueva’s expansive industrial zones (such as Parque Industrial Las Victorias, Zeta Gas corridors, and surrounding industrial hubs), access to verified, pharmaceutical-grade concentrated plant extracts is essential to maintain competitive supply line integrity.
Sourcing botanical active ingredients requires strict compliance beyond basic agricultural commoditization. Phytochemical compounds such as withanolides, polyphenols, trans-resveratrol, fulvic fractions, and alkaloids require precise molecular standardization, validated solvent residue elimination, and guaranteed microbiological safety. As brand owners within the Northern Triangle expand their footprint into export-ready functional foods and therapeutic supplements, partnering with an audited, primary manufacturing factory bridges the gap between agricultural sourcing and finished dosage stability.
1. Primary Extraction Methodology & Engineering Specifications
Concentrated plant extract factories serving high-precision regional supply chains must employ modern fractionation, selective precipitation, and chromatographic purification systems. The efficacy of concentrated herbal compounds relies on preserving native biological active structures while systematically eliminating heavy metals (Arsenic, Cadmium, Lead, Mercury), organochlorine pesticide residues, and microbial spores commonly found in ambient-dried botanicals.
Our extraction lines utilize low-temperature countercurrent extraction technology, high-efficiency vacuum thin-film concentration, and advanced spray drying or lyophilization (freeze-drying) systems. By maintaining precise thermal control under 45°C during active evaporation stages, volatile terpene profiles and thermolabile polyphenolic linkages remain biologically active. Each batch dispatched into international commerce operates under rigorous NSF 455-2 GMP and ISO 22000 management protocols, accompanied by batch-specific High-Performance Liquid Chromatography (HPLC) and Gas Chromatography-Mass Spectrometry (GC-MS) fingerprinting to guarantee active marker concentrations.
Standardized Titration
Verified bioactives via HPLC/UV-Vis: Ashwagandha (Withanolides 2.5%–10%), Trans-Resveratrol 99%, and Shilajit (Fulvic Acid ≥ 50%). Eliminates batch variance across global lots.
USP / EP Compliance
Strict adherence to microbiological limits and elemental impurities. ICP-MS testing confirms compliance with strict regional and international health standards.
Particle Engineering
Custom micronization (80 to 200 mesh), agglomeration, and granulate compaction for high-speed automated capsule filling and direct compression tableting.
2. Localized Industrial Application Scenarios in Villa Nueva
Villa Nueva's strategic positioning within the Departamento de Guatemala creates varied use cases for concentrated plant extracts across domestic production and regional distribution:
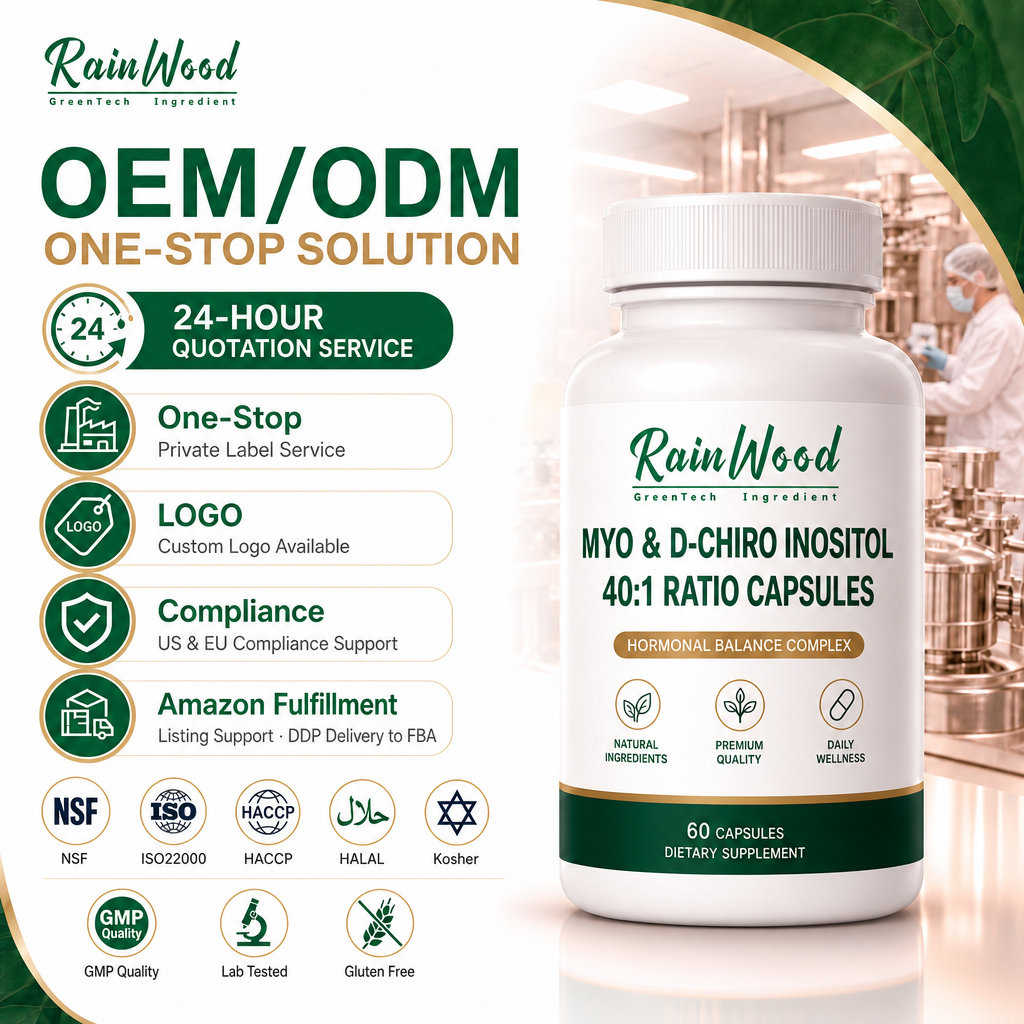
Pharmaceutical & Herbal Medicine Labs: Contract pharmaceutical facilities in Villa Nueva leverage concentrated, standardized extracts (such as Berberine HCl, Myo-Inositol, and standardized Ashwagandha) to manufacture phytomedicines registered with the Departamento de Regulación y Control de Productos Farmacéuticos y Afines. These formulations require rigorous stability testing under Zone IVb conditions (30°C and 75% relative humidity) to guarantee shelf integrity throughout the humid Central American lowlands.
Functional Beverage & Ready-to-Drink (RTD) Bottling: The food and beverage manufacturing cluster in Villa Nueva requires water-soluble, crystal-clear botanical powders that disperse without sedimentary clouding or active precipitation. Botanical active components like trans-resveratrol and polyphenol concentrates are micro-encapsulated to mask natural bitterness while remaining stable through pasteurization cycles.
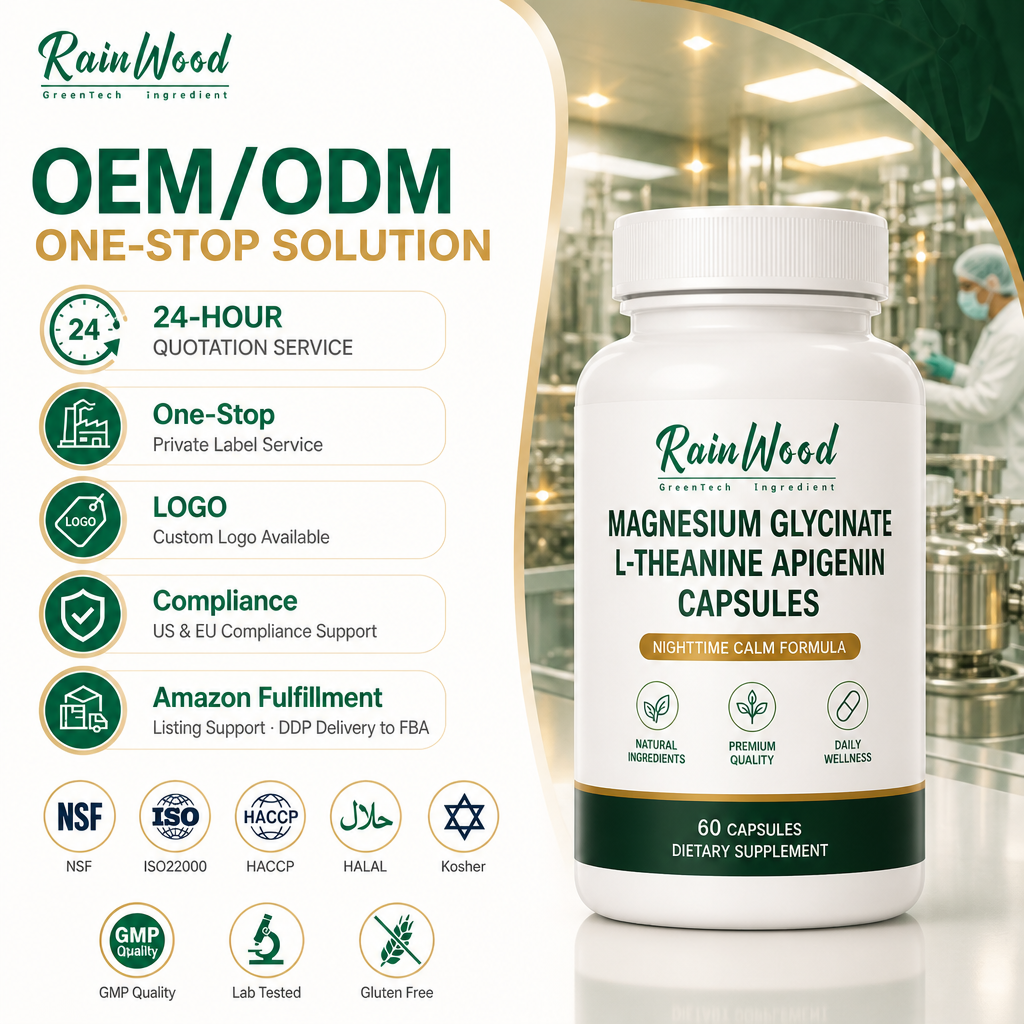
Private-Label Sports & Wellness Brands: Local brand incubators target retail supermarket chains and cross-border ecommerce via Amazon and MercadoLibre. Utilizing our turnkey OEM/ODM encapsulation and pouch stick-pack packaging enables local brands to access low-MOQ, factory-direct finished products without heavy capital expenditures in secondary processing machinery.
3. Macro Market Dynamics: Central American Botanical Modernization
The Latin American botanical extract and dietary supplement sector is undergoing a transformation. Historically dominated by unrefined bulk botanical powders, consumer demand across Guatemala, El Salvador, and Honduras has shifted decisively toward clinically backed bioactives, clean-label plant sources, and certified traceability.
Four primary factors are reshaping procurement priorities within the Villa Nueva trade corridor:
- Verification of Authenticity: Local distributors are moving away from unstandardized raw plant dusts toward extracts verified by independent DNA barcoding and HPLC chromatography, avoiding intentional adulteration and synthetic adulterants.
- Adoption of Modern Dosage Formats: Beyond traditional two-piece hard gelatin capsules, local consumer markets demand vegan HPMC capsules, effervescent tablets, functional pectin-based gummies, and convenient single-serve powder stick packs.
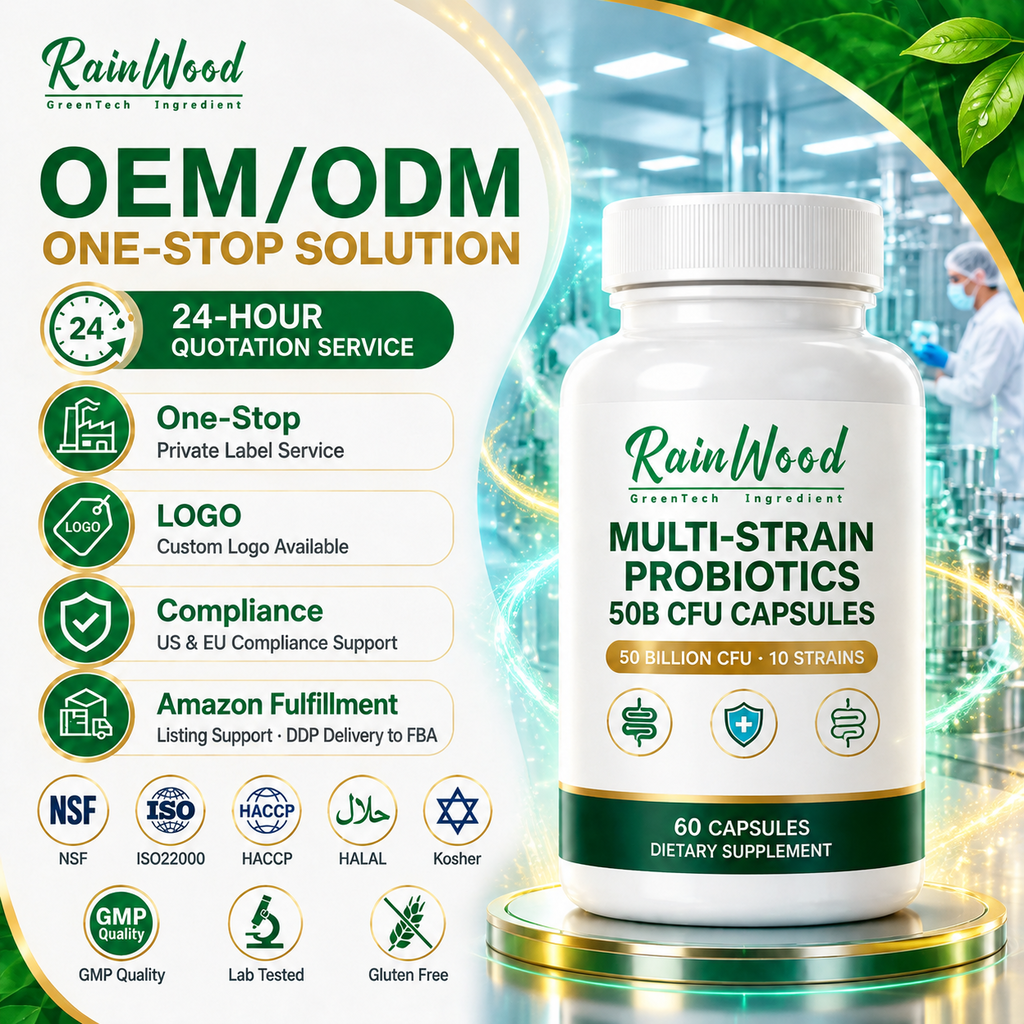
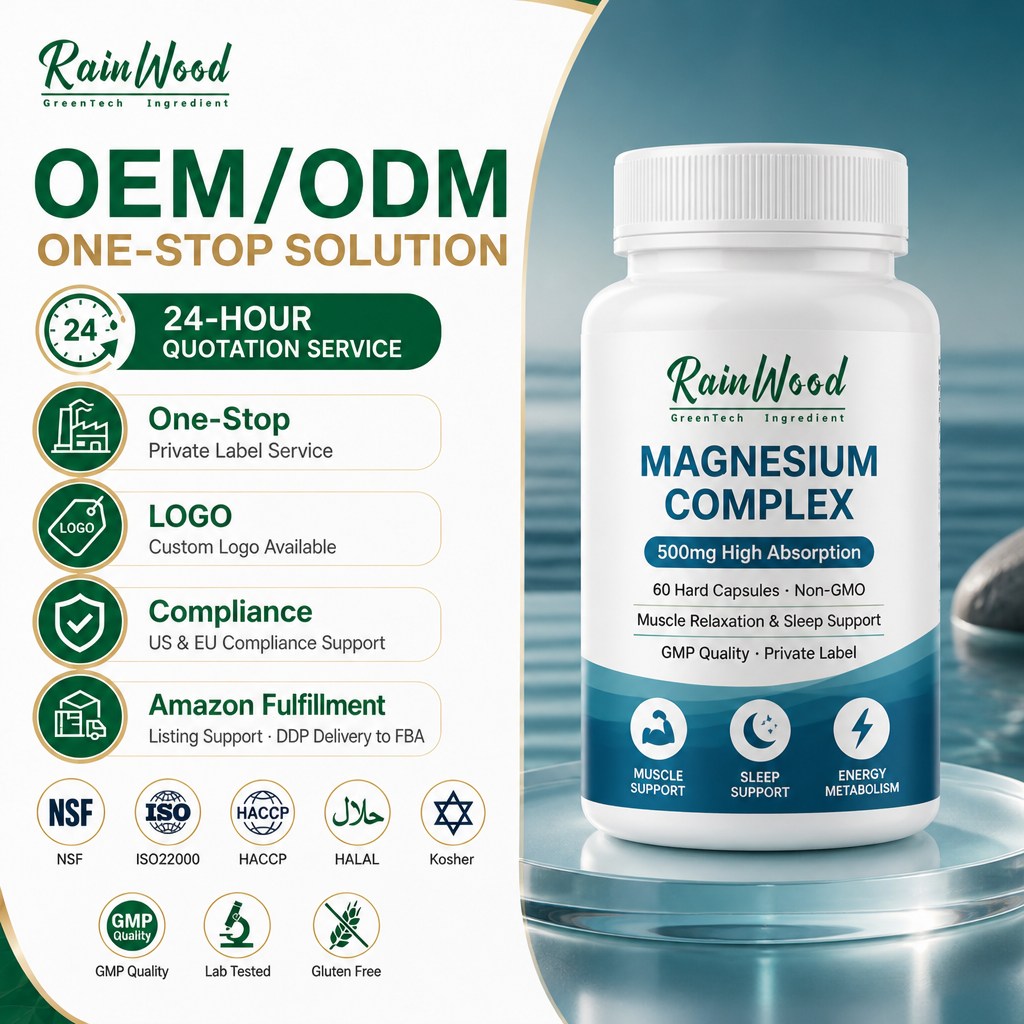
- Microbiome and Metabolic Health Focus: There is a significant rise in multi-strain probiotic combinations (up to 50 Billion CFU) and multi-ingredient metabolic stabilizers that pair concentrated plant alkaloids like Berberine with complex minerals such as Magnesium L-Threonate.
- Regulatory Documentation Rigor: Regional registration authorities increasingly require comprehensive documentation packages including Certificate of Analysis (COA), Certificate of Free Sale (CFS), stability studies, and BSE/TSE-free declarations before granting import clearances.
Shaanxi ESNO Biotech: Global Infrastructure & Technical Capabilities
Operating from the international biotechnology center of Xi'an, China since 2006, our modern manufacturing facilities deliver comprehensive OEM/ODM botanical extraction and finished supplement manufacturing.
NSF 455-2 GMP & ISO 22000 Certified
Every production run occurs within 100,000-class cleanroom workshops verified on-site by TÜV Rheinland. Clean production spaces meet EU, USDA Organic, and HACCP systemic standards.
Full-Spectrum Turnkey Capabilities
Formulation R&D across two-piece hard capsules (gelatin & vegan HPMC), pectin and gelatin gummies, softgels, compression/film-coated tablets, stick packs, and purified Shilajit resin drops.
Dedicated Testing & COA per Batch
In-house microbiology incubators, drying boxes for moisture testing, and analytical precision balances ensure complete traceability from raw botanical arrival to pallet dispatch.
Frequently Asked Questions for Sourcing in Villa Nueva
Key answers addressing logistics, customs documentation, shelf-life integrity, and minimum orders for regional importers.
What are the shipping routes, typical transit times, and documentation for deliveries into Villa Nueva?
FCL (Full Container Load) and LCL (Less than Container Load) maritime shipments depart directly from major Chinese hubs (Shanghai, Ningbo, or Qingdao) directly to Puerto Quetzal on Guatemala's Pacific coast. Typical ocean freight transit ranges from 24 to 32 days. From Puerto Quetzal, shipments proceed north along the CA-9 highway directly to Villa Nueva customs warehouses or free trade zones within 2 to 4 hours. Every consignment is supported by commercial invoices, packing lists, bill of lading (BOL), batch Certificate of Analysis (COA), Certificate of Origin, and sanitary export clearance documentation.
How do concentrated plant extracts remain stable in Central America's humid tropical climate?
Botanical extracts can be naturally hygroscopic. To guarantee chemical potency and prevent clumping or caking in tropical environments (Zone IVb conditions), raw concentrated powders are packed in double pharmaceutical-grade polyethylene liner bags sealed within airtight, moisture-barrier aluminum laminate drums with desiccant packs. For finished encapsulated and tableted products, we recommend high-barrier Alu-Alu or PVC/PVDC blister packing, or high-density polyethylene (HDPE) amber bottles featuring induction-sealed inner safety neck foils.
What are the minimum order quantities (MOQ) for custom private label vs. bulk extracts?
For standardized bulk botanical extracts and pure herbal powders, our baseline MOQ begins as low as 1 kg for pilot testing and 25 kg (standard fiber drum) for commercial production. For private-label finished goods, stock encapsulated formulas start at 100 to 500 bottles/boxes, custom functional gummies start at 500 to 1,000 units, and custom softgels begin at 2,000 pieces. Full turnkey formulation engineering is quoted based on specific active ingredient profiles.
Can your team support health registration with the Guatemalan Ministry of Public Health (MSPAS)?
Yes. Obtaining a sanitary registration (*Registro Sanitario*) via the *Departamento de Regulación y Control de Productos Farmacéuticos y Afines* requires rigorous technical dossiers. We supply comprehensive technical manufacturing flowcharts, qualitative-quantitative formulas, certificate of free sale (CFS) apostilled where requested, Certificate of Analysis per batch, stability testing data, and heavy metal/microbial validation reports adhering to USP/EP pharmacopeial guidelines.
How do you prevent contamination, heavy metals, and active ingredient degradation?
Every incoming botanical lot undergoes strict quarantine and raw identity verification. Our quality assurance lab utilizes Inductively Coupled Plasma Mass Spectrometry (ICP-MS) for heavy metal profiling, high-precision HPLC for active compound titration, and systematic microbiology plating in dedicated incubator chambers to verify total plate count, yeast, mold, Salmonella, and E. coli absence. We do not use harsh ethylene oxide (EtO) irradiation, maintaining organic standard compliance.
Partner with a Global Leader in Plant Extract Synthesis
Initiate direct communication with our technical formulation engineers. Request comprehensive product dossiers, factory-direct wholesale pricing, and sample pilot batches for your Villa Nueva manufacturing or distribution business.
Contact Us