Export Grade Standard
Featured Functional Raw Materials & Formulation Bases
Engineered to rigid GMP, ISO 22000, and analytical purity profiles, our botanical matrix concentrates deliver predictable solubility, flowability, and chemical stability.
Engineering Technical Dossier
Overcoming Thermal Degradation & Hygroscopicity in Industrial Botanical Milling
For food scientists, compounders, and supplement brand directors in Puebla and the broader Bajío/Central Mexican industrial corridors, botanical powders present distinct processing challenges. Converting whole fruits—including passionfruit, prickly pear (tuna), guava, acerola, and endemic citrus—into flowable, bioactive powders requires precise moisture mitigation, glass transition temperature (Tg) stabilization, and targeted carrier matrix control.
1. Glass Transition Control & Carrier Dynamics in Spray Drying
Natural fruit juices contain elevated proportions of low-molecular-weight carbohydrates (fructose, glucose) and organic acids (malic, citric, tartaric acid), resulting in intrinsically low glass transition temperatures, often dipping below 40°C. In high-humidity manufacturing hubs, unmitigated fruit powders rapidly cross this threshold, triggering severe caking, sticky matrix collapse, and microencapsulation failure. Our Puebla-facing supply architecture integrates standardized maltodextrin (10–15 DE), organic gum acacia, and native pea starch systems via advanced thermodynamic co-current spray towers. By elevating the formulation's cumulative Tg above 65°C, we assure that our powders resist humidity-induced structural collapse during prolonged intermodal freight across Mexico and into United States logistics terminals.
2. Phenolic Bioavailability & Low-Thermal Retention Systems
Conventional flash heating causes immediate isomerization and degradation of sensitive antioxidant anthocyanins, polyphenols, and native ascorbic acid chains. To resolve these nutrient depletion vectors, our production relies on continuous low-temperature vacuum extraction and counter-current tangential membrane concentration. By concentrating the native juice matrix without prolonged thermal load prior to atomization, thermolabile bioactive phytonutrients remain intact. Each production lot comes certified via High-Performance Liquid Chromatography (HPLC) to guarantee minimum guaranteed bioactive assay targets, meeting the stringent audit expectations of modern pharmaceutical cleanrooms and functional food compounding operations.
Localized Integration
Target Application Paradigms across Puebla's Industrial Core
Tailoring botanical dry-extract specifications to regional manufacturing hubs from Huejotzingo to Tehuacán.
Beverage & Ready-to-Drink (RTD) Formulation
Instant cold-water dispersal without sediment dropout. Used heavily in Puebla's growing craft carbonated botanicals, functional kombuchas, and electrolyte reconstitution drink packets requiring zero artificial dyes and crystal-clear solubility profiles.
Clean-Label Bakery, Confectionery & Snacks
Natural fruit powders engineered for high bake-stability. Formulators replace synthetic red and purple lake pigments in artisan cookies, pan dulce coatings, and extruded grain snacks with heat-resistant beet, hibiscus, and berry solids.
Nutraceutical Blends, Sachets & Gummies
Micro-milled to >80 mesh standards for direct high-speed tableting and rotary capsule filling. Completely compatible with vegan pectin gummy manufacturing setups avoiding pre-gelation curdling or syneresis under varying pH ranges.
Market Intelligence
Procurement Dynamics Driving Botanical Demand in Puebla
How nearshoring, clean-label shifts, and strict NOM regulations are transforming regional supply chains.
Nearshoring Growth
International functional nutrition companies are utilizing Puebla’s strategic rail and highway connections to Veracruz and Mexico City, setting up contract packing facilities for North American export.
NOM-051 Warning Seal Avoidance
Mexico's strict front-of-package nutritional warning system pushes R&D teams to substitute refined sugars with concentrated fruit powders delivering natural sweetness and functional dietary fiber.
Certified Microbial Traceability
Local QA managers no longer tolerate unverified agricultural raw goods. Purchasing directors require comprehensive heavy metal, E. coli, Salmonella, and pesticide screens before material offloading.
Supply Stability & Bulk Warehousing
Procurement teams are shifting away from spot agricultural market volatility, favoring contracts with manufacturers offering long-term pricing, standardized COAs, and reserve batch staging.
Enterprise Authority
19 Years of Advanced Manufacturing Rigor
Founded in 2006, Shaanxi ESNO Biotech Co., Ltd. operates modern, audited production workshops dedicated to botanical extraction, standardized spray-drying, and turnkey nutraceutical formulation. Certified under NSF 455-2 GMP, ISO 22000, and HACCP frameworks, we provide verified industrial consistency to over 3,500 enterprise partners across 100+ nations.
- NSF 455-2 GMP & ISO 22000 Audited: Strict cleanroom workflows verified on-site by TÜV Rheinland.
- End-to-End Analytical Dossiers: Every individual shipment includes a batch-specific Certificate of Analysis (COA) containing HPLC/UV active assays, loss-on-drying, and heavy metals screening.
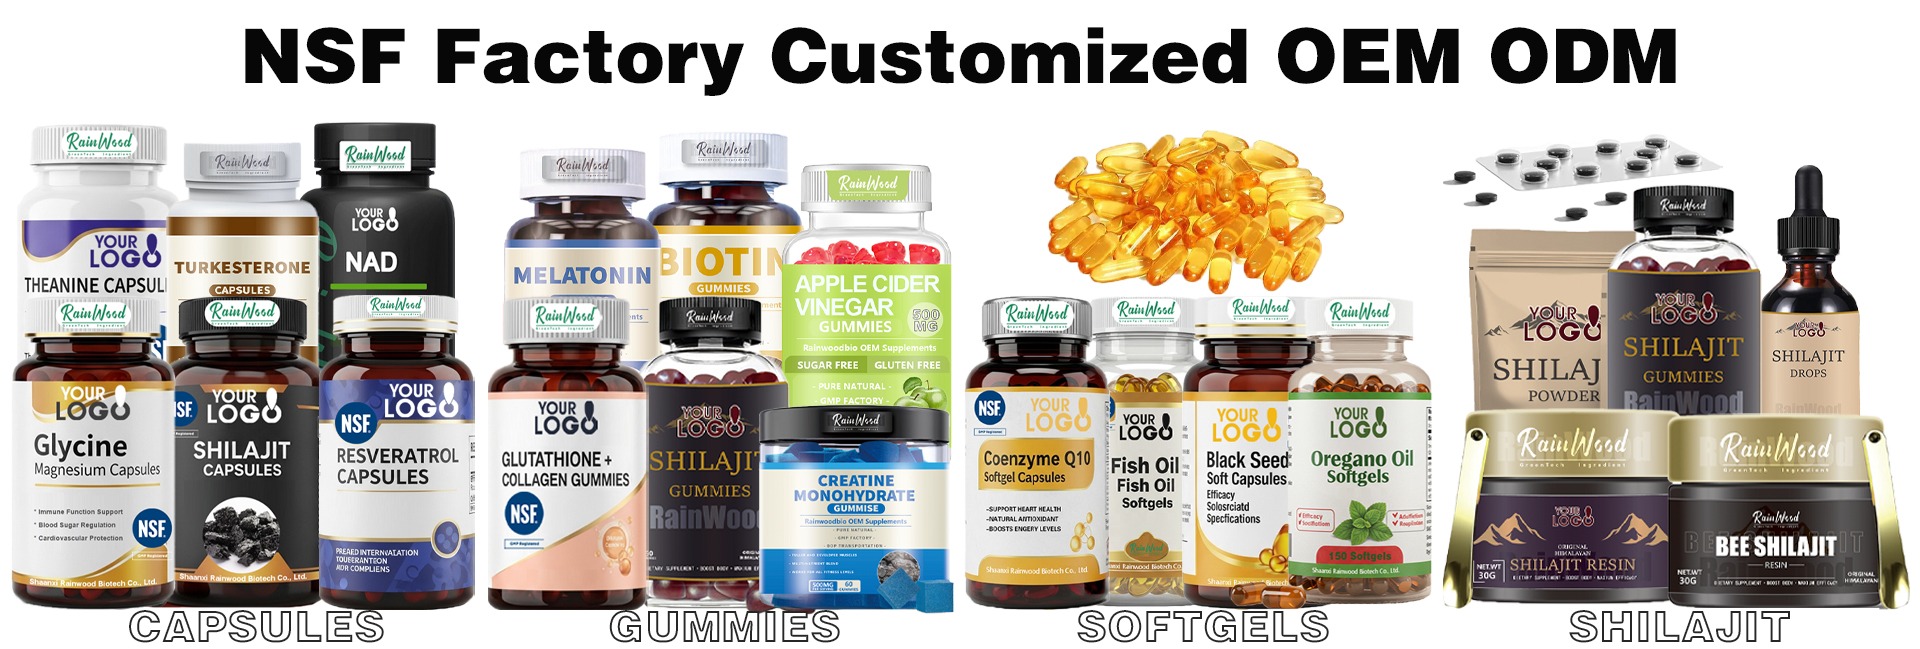
- Scalable Custom Contract Formulations: Complete formula support spanning bulk dry powders, premix stick packs, customized hard capsules, and vegan pectin gummies.
Technical Q&A
Frequently Asked Questions by Industrial Sourcing Teams
Analytical insights into customs clearance, carriers, stability, and minimum purchase commitments.
What carrier options and carrier-free formulations are offered for natural fruit powders?
Depending on your target matrix and local regulatory goals (e.g., European clean label vs. domestic Mexican confectionery processing), we provide customizable carrier substrates. Standard options incorporate non-GMO maltodextrin (10–15 DE) for optimal flowability and rapid dispersion. Alternatively, we produce 100% natural, certified organic carrier options using organic gum acacia or native pea fiber, as well as pure fruit solid freeze-dried concentrates formulated without exogenous anti-caking or carrier agents.
How do you ensure batch-to-batch solubility and avoid caking during storage in high-humidity facilities?
Our facilities utilize continuous fluidized-bed agglomeration following primary spray drying. This process reorganizes fine micro-particulates into uniform porous granules (>80 mesh) with high wettability and dispersibility. To protect hygroscopic fruit powders against tropical and sub-tropical storage climates, products are sealed in multi-layer vacuum heat-sealed aluminum barrier liners with inner polyethylene food-contact bags, encased in rigid fibre drums. We recommend staging storage below 25°C and <60% relative humidity.
What compliance documentation accompanies shipments to Puebla manufacturing plants?
Every shipment arrives with full documentation to streamline COFEPRIS customs clearance and internal QA qualification. Standard documentation includes our comprehensive Certificate of Analysis (COA) specifying microbiological limits (USP/EP standards for total plate count, yeast/mold, absence of Salmonella and E. coli), ICP-MS heavy metals testing (Pb, As, Cd, Hg within international safety margins), moisture isotherms, and particle size distribution curves. Technical Data Sheets (TDS), Safety Data Sheets (SDS), and Allergen Statements are provided prior to export dispatch.
What are your Minimum Order Quantities (MOQ) for stock ingredients and tailored premixes?
For catalog items and standardized fruit concentrates, commercial MOQs start as low as 25 kg (single drum trial orders) to support preliminary pilot runs and sensory compounding tests. For custom functional spray-drying profiles (tailored carrier matrices, fortification with amino acids, or targeted colorimetric indices), production runs typically initiate at 500 kg to ensure optimal thermal efficiency and yield consistency.
Can you manufacture finished OEM capsule, tablet, or gummy formats using custom fruit powder formulas?
Yes. Beyond supplying raw bulk active materials, our OEM/ODM infrastructure supports turn-key formulations. We process custom functional powders into direct-compressed chewable tablets, vegan HPMC hard-shell capsules, single-dose powder sachets/stick packs, and high-potency pectin gummies. Our product engineering team handles complete formula blending, stability evaluations, primary packaging, and customized private label secondary carton production.
Optimize Your Product Development Pipeline
Consult with our applications engineering and commercial sourcing specialists. Request technical dossiers, regulatory validation packages, or pilot formulation samples dispatched directly to your facility in Puebla.
Inquire Now