The growing demand for high-integrity dietary supplements and therapeutic botanicals in regional Asian medical hubs has elevated quality expectations for active ingredients. As an established GMP, ISO 22000, and HACCP-certified manufacturer, Shaanxi ESNO Biotech Co., Ltd. provides robust contract manufacturing (OEM/ODM) solutions tailored for specialized healthcare frameworks, commercial dispensaries, and retail brand distributors supplying the Wonsan market. Leveraging precision extraction pipelines and advanced powder encapsulation infrastructure, we deliver targeted botanical actives characterized by uniform active markers, verified bioequivalence, and stringent batch-to-batch repeatability.
Featured Turnkey Herbal & Mineral Formulations
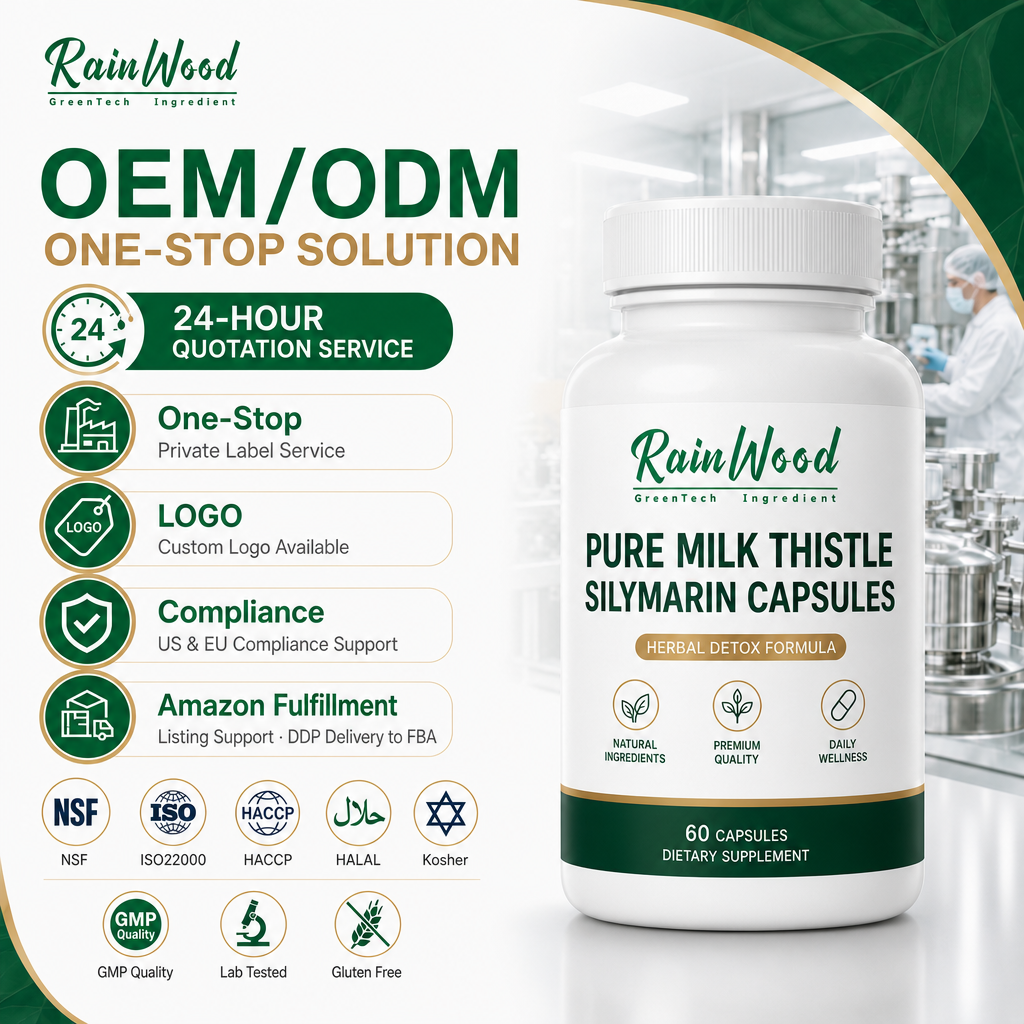
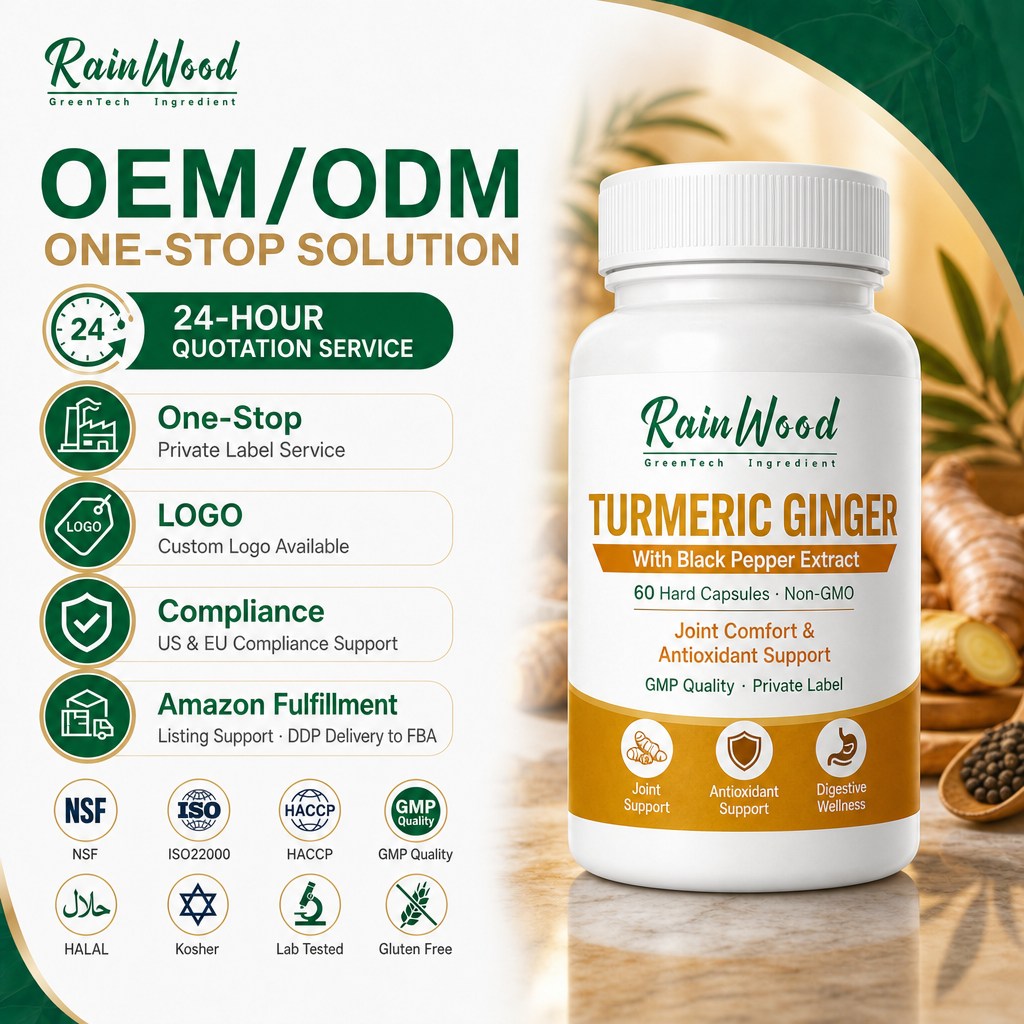
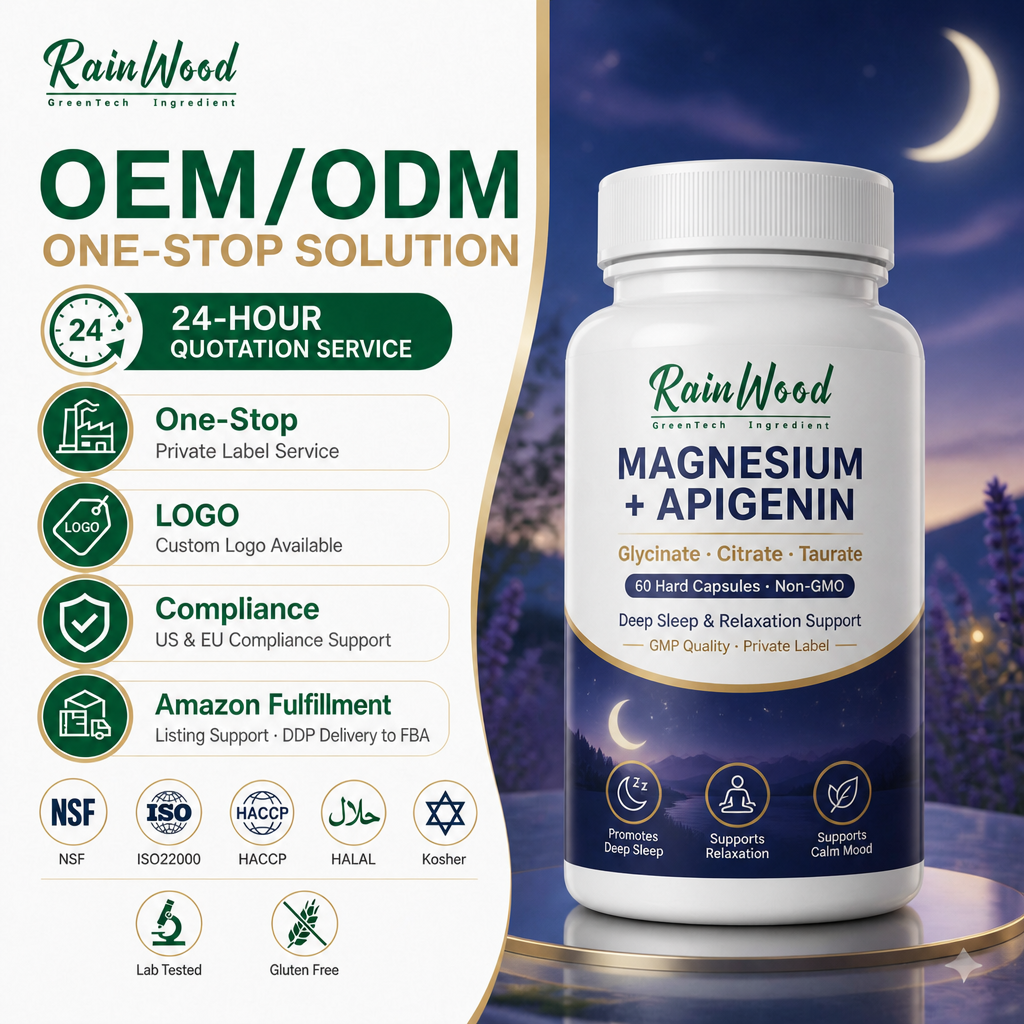
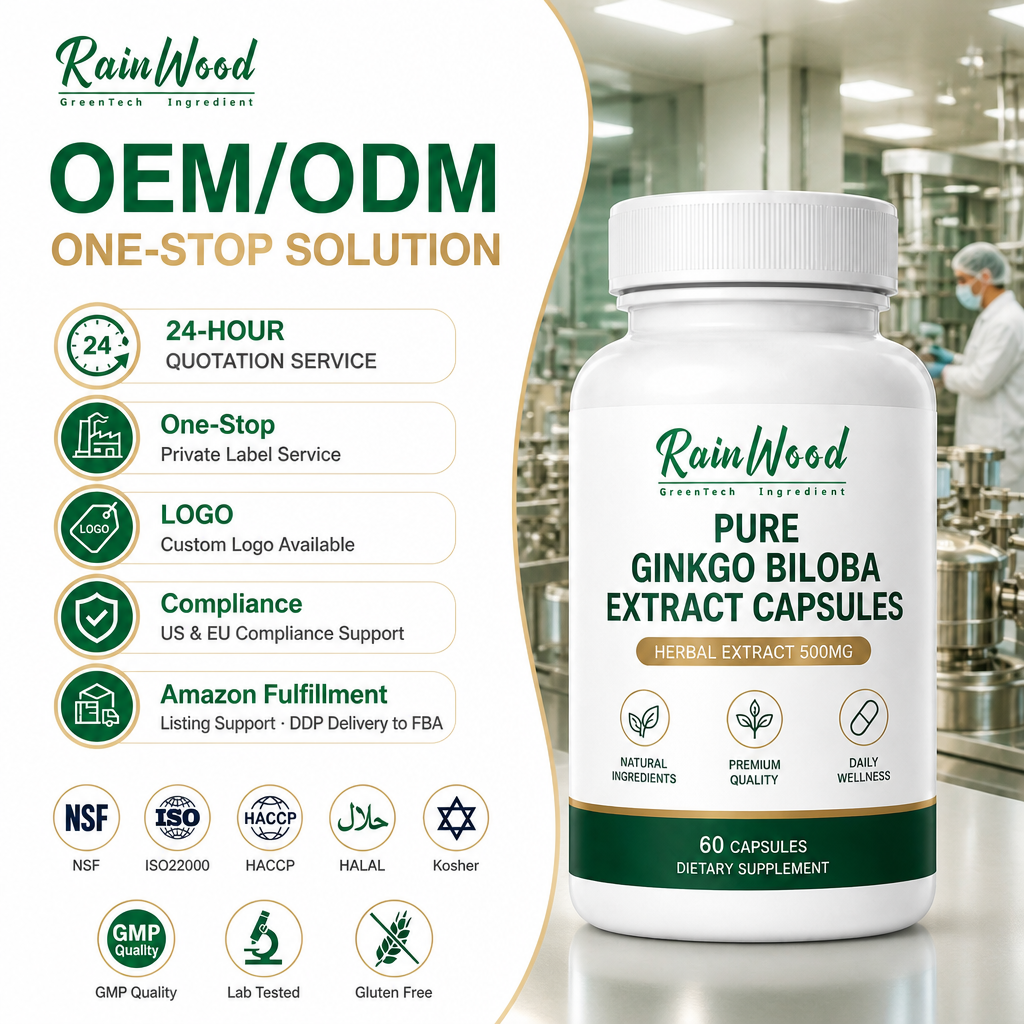
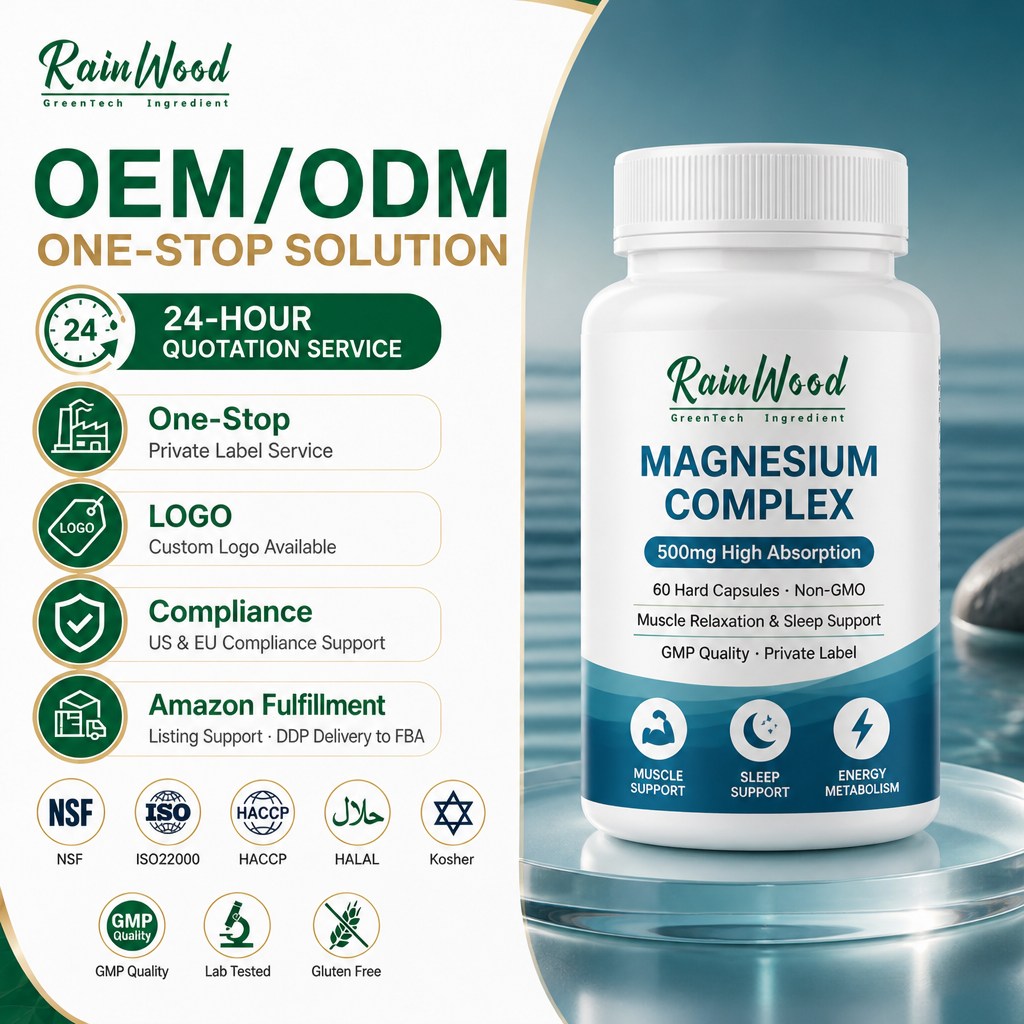
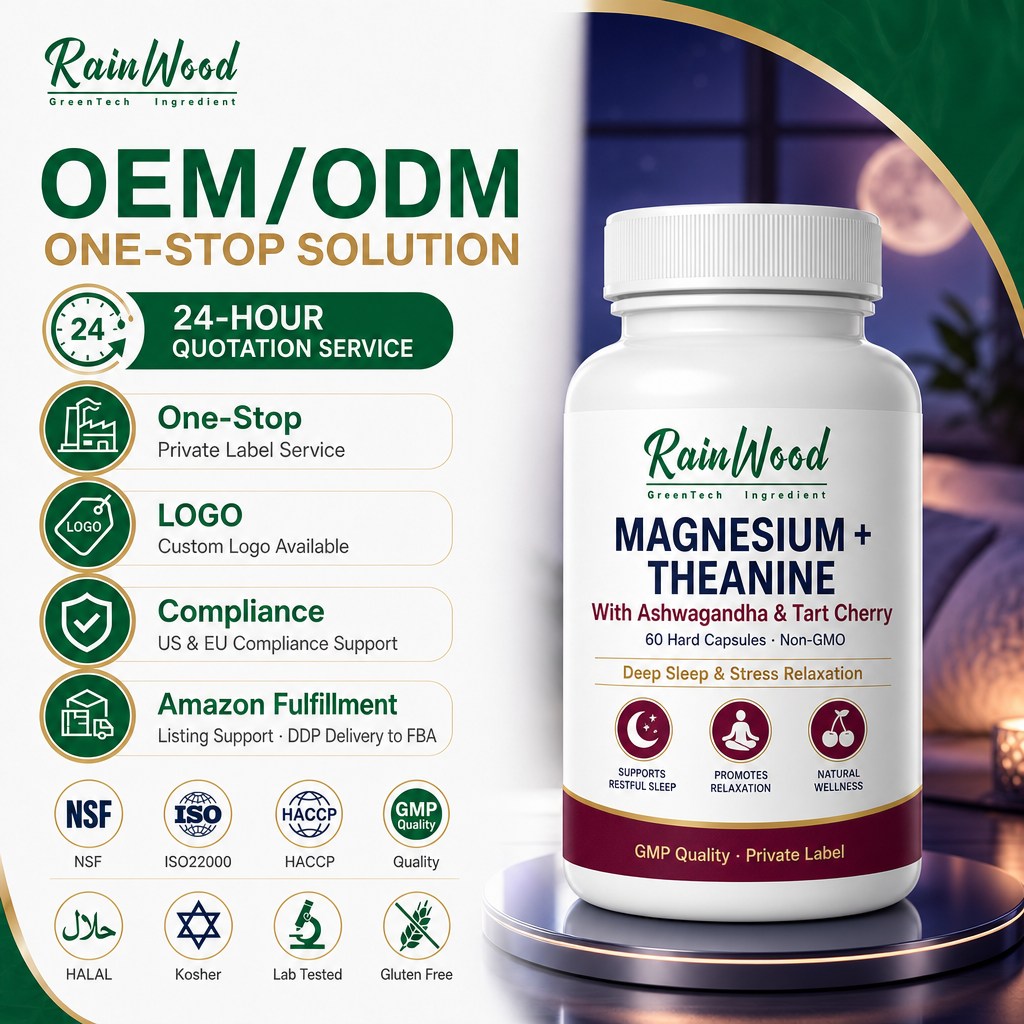
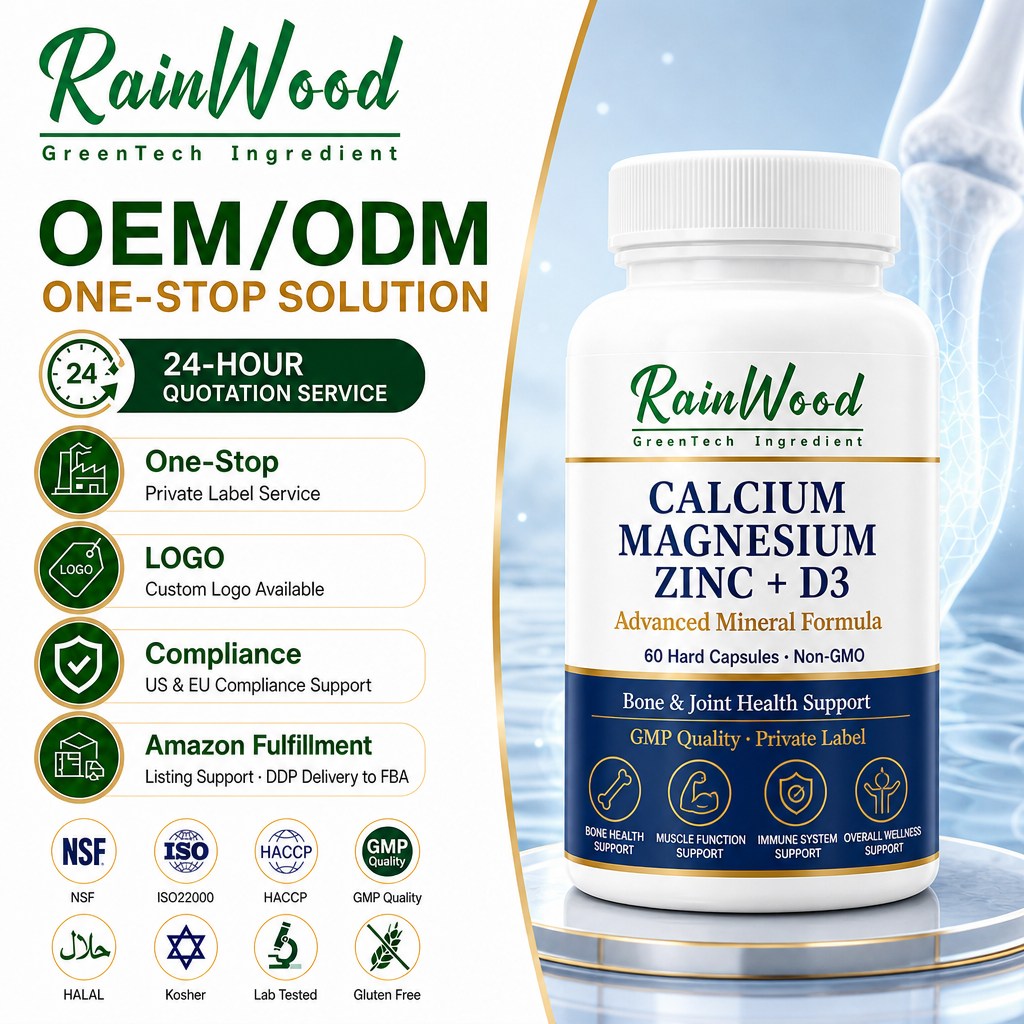
Engineered for private label deployment, our ready-to-scale dietary formulas combine functional herbal isolates with synergistic vitamins and chelated minerals to satisfy international pharmacopeia tolerances.
Localized Application Scenarios in the Wonsan Industrial & Healthcare Ecosystem
The developmental and commercial landscape of Wonsan—characterized by coastal industrial initiatives, expanding hospitality districts, and specialized health sanitariums—demands targeted phytotherapeutic formulations designed to withstand distinct regional environmental stressors and demographic needs.
Maritime & Heavy Industrial Occupational Health
Heavy engineering, port operations, and industrial manufacturing expose personnel to elevated oxidative stress and systemic fatigue. Our high-potency standardized botanical extracts—notably Silymarin from Milk Thistle and nano-milled Curcuminoids combined with Piperine—provide institutional procurement directors with bioavailable solutions for hepatic cytoprotection and cellular anti-inflammatory management.
Geriatric Care & Convalescent Sanitariums
Regional therapeutic resorts and recuperation retreats focus heavily on cognitive longevity, bone remineralization, and autonomic relaxation. Incorporating Ginkgo Biloba Terpene Lactones (24/6) and multi-chelated Magnesium Glycinate-Citrate-Taurate into daily protocols addresses neuro-microvascular insufficiency, arterial compliance, and restorative sleep quality in aging cohorts.
High-Humidity Coastal Physical Resilience
Coastal microclimates characterized by sharp seasonal thermal fluctuations trigger chronic joint discomfort and metabolic sluggishness. Our tailored mineral-vitamin complexes (Calcium-Magnesium-Zinc-D3) and standardized adaptogenic formulations (Ashwagandha with Tart Cherry) maintain systemic mineral homeostasis and accelerate connective tissue rehabilitation under harsh coastal shifts.
Emerging Nutraceutical & Botanical Trends in Regional Supply Chains
Procurement executives operating in maritime transit points and provincial medical facilities are executing strategic shifts toward scientifically validated botanical concentrates. Understanding these shifts provides a competitive edge:
1. Transition to High-Assay Standardized Extracts
Historical dependence on unstandardized raw botanical decoctions is being replaced by quantifiable phytochemical markers. Professional procurers increasingly require HPLC/UV-verified assays—such as total silymarin ≥80% or curcuminoids ≥95%—to guarantee consistent pharmacodynamic activity across batches, eliminating potency variations associated with raw plant harvesting seasons.
2. Chelated Formats Outpacing Inorganic Salts
Mineral supplementation within medical recovery centers has transitioned away from cheap, gastro-irritating inorganic oxides and carbonates. The market demands highly bioavailable bisglycinates, citrates, and taurates. These organic chelates bypass normal competitive ion channels in the intestinal mucosa, preventing gastric distress and maximizing bioavailability at lower doses.
3. Climate-Resilient Packaging & Shell Technology
Due to Wonsan's marine relative humidity, conventional animal gelatin capsules frequently suffer from moisture absorption, stickiness, or brittleness. In response, modern buyers prioritize non-animal HPMC (Hydroxypropyl Methylcellulose) vegetarian capsules packaged in hermetically induction-sealed HDPE containers or double-layer Alu-PVC thermoformed blister cards to guarantee active shelf-life stability.
Enterprise Advantage: Shaanxi ESNO Biotech Co., Ltd.
With headquarters in the high-tech botanical extraction corridor of Xi'an, Shaanxi ESNO Biotech operates an integrated vertical supply ecosystem spanning botanical sourcing, supercritical fluid extraction, granular compaction, and fully automated packaging lines.
Stringent International Quality Audits
Our manufacturing plant maintains continuous certification under NSF 455-2 GMP, ISO 22000, and HACCP. Every batch is released exclusively after comprehensive in-house and third-party laboratory verification, ensuring complete safety from microbiological pathogens, pesticide residues, and heavy metals (Pb, As, Cd, Hg) well below international thresholds.
Custom Formulation & Formulation R&D
Backed by 19 years of formulation engineering and over 400 commercialized products, our technical division assists client partners in solving complex active-ingredient incompatibilities, optimizing powder flowability for zero-excipient encapsulation, and executing targeted particle-size reduction via micronization.
Dedicated Account Management & Compliance Support
We eliminate communication latency by assigning dedicated B2B technical account managers to oversee your product life cycle from initial bench-scale pilot sampling through primary production, bilingual labeling audit, and customs export clearances. Every export shipment includes full traceability dossiers: Certificate of Analysis (COA), Batch Manufacturing Records, and MSDS.
Frequently Asked Questions: Wonsan B2B Procurement
What are the standard Minimum Order Quantities (MOQs) for custom private label orders?
For verified stock formulations in existing tooling sizes (such as standard 60-count hard capsule bottles), our production runs start at a competitive 500 to 1,000 units. For specialized custom-milled compounds, bespoke color-matched vegetarian capsules, or custom-printed blister sleeves, MOQs typically range from 2,000 to 3,000 units. We also offer lower pilot-scale trial quantities to facilitate initial market qualification.
What analytical documentation and assay verifications accompany export shipments?
Every single dispatch is accompanied by an authenticated Certificate of Analysis (COA) generated by our ISO-compliant analytical testing laboratory. This includes active phytochemical marker assays (HPLC/UV), loss on drying, bulk density, disintegrating profile testing, heavy metal ICP-MS quantification (Lead, Cadmium, Mercury, Arsenic), and full microbial panel testing (Total Plate Count, Yeast & Mold, E. Coli, Salmonella). Additional verification reports via TÜV Rheinland or third-party SGS audits are available upon contract request.
How do you ensure formulation stability during ocean transit and humid coastal storage?
Coastal distribution channels require specialized atmospheric defense. We employ pharmaceutical-grade desiccant inserts (silica gel or molecular sieve packets), high-density polyethylene (HDPE) or amber glass containers with induction-heat aluminum foil seals, and specialized low-hygroscopic plant HPMC shells. Accelerated stability testing (40°C ± 2°C / 75% RH ± 5% RH) is standard for all formulations to ensure active potency remains within declared label claim throughout the 24- to 36-month shelf life.
Can ESNO Biotech modify ingredient ratios to conform to specific regional health regulations?
Yes. Our in-house R&D staff regularly reformulates products to align with target regional regulatory guidelines. Whether your procurement guidelines restrict specific excipient binders (such as magnesium stearate or silicon dioxide) or mandate strict dosage caps on active elemental minerals and herbal extract concentrations, our team provides custom blending, granulation adjustments, and complete ingredient declaration sheets.
What is the typical production lead time from sample sign-off to port delivery?
Pilot bench samples are typically prepared and dispatched within 5 to 7 business days. Following sample approval, packaging design finalization, and deposit confirmation, commercial mass manufacturing is executed within 20 to 25 business days. Containerized export shipments are coordinated directly via major northern transport terminals with complete transit tracking and customs clearing document suites.
Connect with our Technical Formulation Team
Whether you are seeking custom capsule manufacturing, bulk standardized botanical isolates, or private-label turnkey solutions, our specialists are available to review your specifications and supply detailed quotation dossiers.
Send an Inquiry